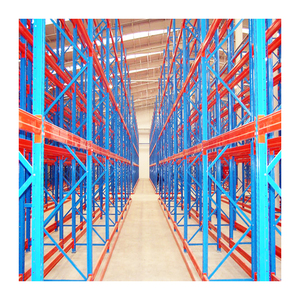
VNA Heavy Duty Pallet Racking
Maximizes vertical clearance with narrow guide rails, yielding high cubic retrieval capacity for intensive multi-SKU operations.
Explore our heavy-duty multi-tier configurations, structural racking platforms, and dynamic flow storage systems built to rigorous international structural codes.
Maximizes vertical clearance with narrow guide rails, yielding high cubic retrieval capacity for intensive multi-SKU operations.
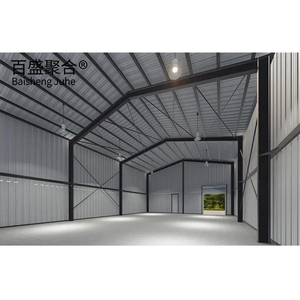
High-tensile structural frames designed to anchor multi-tier pallet racking and expansive mezzanine logistics hubs.
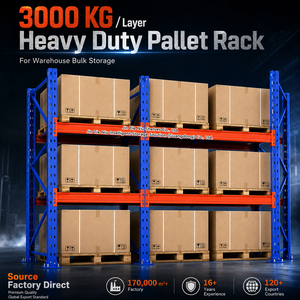
Robust dual-level powder-coated steel racking with heavy-duty boxed beam sections providing corrosion-resistant support.
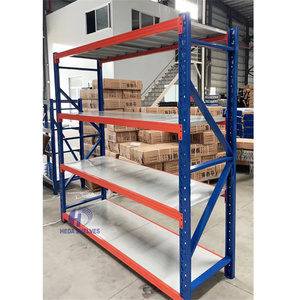
Flexible catwalk-compatible medium-duty storage shelving optimized for manual split-case picking, workshop tools, and parts.
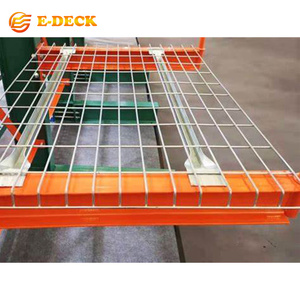
Fire-code compliant hot-dipped galvanized decking channels engineered to distribute point loads and improve internal lighting.
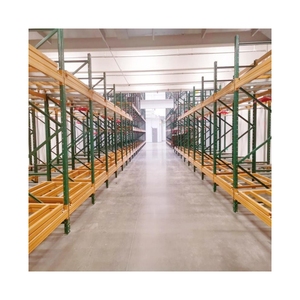
Dynamic nested trolley rail system delivering 2-6 pallet deep high-density storage under LIFO inventory control standards.
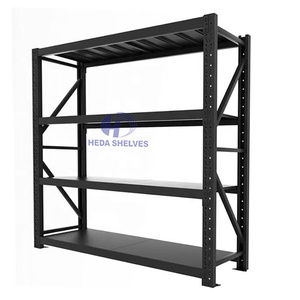
Versatile boltless modular stacking frames engineered for rapid repositioning, seasonal logistics flex, and fast assembly.
Integrated pipeline valves and flow control instrumentation designed for industrial HVAC, fire suppression, and fluid monitoring.
Modern fulfillment networks, cold chains, and cross-border distribution centers are confronting surging industrial real estate costs. When horizontal facility footprint expansion is constrained by cost or land scarcity, vertical optimization through engineered multi-tier pallet racking systems becomes essential for modern logistics design. Unlike standard single-level racking, multi-tier platforms leverage the full vertical cubic volume of modern warehouse structures, integrating heavy-duty pallet load capacities with overhead multi-story catwalks, automated replenishment channels, and advanced conveyor routing.
As international supply chains evolve through e-commerce scaling and nearshoring initiatives, procurement directors face complex system evaluations:
The transition toward semi-automated and fully automated fulfillment has transformed the design of multi-tier racking systems. Warehouses require structural adaptability for:
End-to-end manufacturing oversight, rigorous quality verification, and personalized structural design support.
Operating under certified CE marking (No. 2435-CPR-8605159), ISO 9001:2015 management systems, and RoHS compliance. Our high-tensile hot-rolled Q235B and Q355B coils undergo stringent tensile and yield testing.
Our in-house design engineers evaluate your facility drawings, forklift turning radiuses, aisle clearances, and pallet load profiles to deliver complimentary detailed CAD schematics, 3D renderings, and certified load capacity tables.
With exports spanning over 120 countries, every container load is optimized for space efficiency and balance, bundled with heavy-duty steel strapping, edge corner guards, water-resistant wrap, and itemized container packing lists.
Practical structural, engineering, and logistics insights for warehouse procurement managers.
Multi-tier racking systems concentrate significant dead and dynamic point loads on the concrete warehouse slab. Typically, industrial concrete floor slabs must possess a minimum thickness of 150mm to 250mm with a compressive strength rating of C25/30 to C30/37 (or 3,500 to 4,500 PSI). During engineering review, we specify widened baseplates and heavy chemical anchor bolts to safely distribute upright column loads.
Modern local and international building fire codes (such as NFPA 13) require comprehensive in-rack sprinkler integration when racking exceeds specific heights or when multi-tier floors obstruct ceiling sprinkler coverage. We supply galvanized open wire mesh decking or perforated steel planking (providing 50% open area) and engineered pipe run-through cutouts for vertical fire suppression piping.
Yes. Our multi-tier racking components are treated through a 10-stage automated finishing process including degreasing, acid pickling, zinc phosphating, and electrostatically sprayed architectural-grade thermosetting powder coating. For exterior, unconditioned tropical, or cold-storage environments (-30°C), we provide complete hot-dipped galvanized steel options that resist flaking and oxidation.
To produce an exact structural blueprint and cost proposal, our engineering team requires: facility architectural blueprints (including column grid spacing and clear height under joists), pallet outer dimensions (width, depth, height inclusive of overhang), maximum load weight per pallet, material handling equipment (forklift model, turning radius, and max lift reach), and target throughput metrics.
Every overseas export order is shipped alongside detailed 3D structural assembly schematics, numbered component charts, and comprehensive installation manuals. For large-scale multi-tier configurations, our technical engineering division offers bilingual remote video technical support as well as the deployment of on-site supervisory engineers to manage local installation crews.
Standard multi-tier pallet racking production schedules typically run between 20 to 30 calendar days from formal engineering CAD drawing sign-off and load calculation approval. Export transit schedules vary depending on the destination port, with direct liner routes from South China ports (Guangzhou, Shenzhen, Hong Kong) arriving across major worldwide trade corridors under CIF, FOB, or DDU terms.
Connect with our senior logistics structural engineering team. Request a custom structural layout, seismic load calculation, and factory-direct price quotation for your next multi-tier racking facility.
Get Catalog