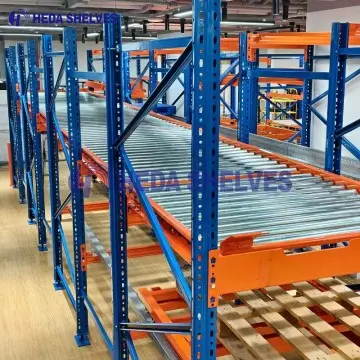
Standalone Carton Flow Racks
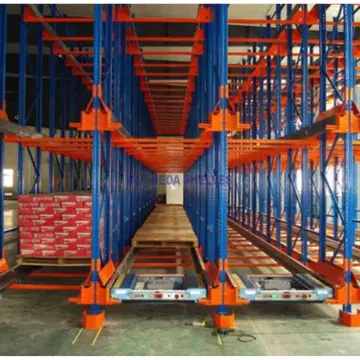
Dedicated dynamic picking bays featuring freestanding uprights, adjustable flow levels, and high-impact plastic roller tracks for fast-moving consumer goods.
- Strict FIFO Control
- Knuckle Pick Trays
- Up to 250 kg/Level
An in-depth technical analysis for supply chain engineers, fulfillment architects, and global procurement managers seeking verifiable data on gravity roller flow performance.
In modern high-density distribution centers and e-commerce fulfillment hubs, picking efficiency and floor space utilization represent over 60% of operating expenses. Carton Flow Racking—frequently referred to as carton live storage or gravity flow shelving—is an engineered dynamic storage structure that leverages gravity feed mechanisms to advance cartons, plastic totes, and bins from the rear loading aisle to the front picking face. By slanting roller tracks at a calibrated gradient (typically 2.5° to 5.5° or a 3% to 6% slope), the system enforces strict First-In, First-Out (FIFO) stock rotation, minimizes picker walking distances, and completely decouples restocking activities from picking lanes.
Static shelving forces operators to navigate dead-end aisles where loading and retrieval share the same congested passage. In contrast, carton flow racking establishes a unidirectional throughput stream. The fundamental mechanics depend on several interconnected structural components:
| Parameter | Light-to-Medium Duty Track | Heavy-Duty Roller Bed | Retrofit Drop-In Track |
|---|---|---|---|
| Roller Type | High-Impact Polypropylene / Polyethylene | Hardened Steel Bearings / Full-Width Rollers | Universal Plastic Skate Wheels / Hex Shaft |
| Load Rating per Lane | 50 – 120 kg/meter | 150 – 350 kg/meter | 40 – 100 kg/meter |
| Recommended Gradient | 3.0% – 4.5% (approx. 2.0° – 2.8°) | 3.5% – 5.5% (approx. 2.2° – 3.2°) | 3.0% – 5.0% (variable adjust) |
| Applicable Containers | Smooth plastic totes, kitted carton boxes | Heavy corrugated cardboard, wooden totes, metal bins | Standard cartons & small parts bins |
| Structural Integration | Standalone boltless rack / Longspan uprights | Heavy pallet racking beams & Mezzanines | Existing teardrop & step-beam pallet racks |
The primary concern raised by logistics specialists when deploying carton flow racking is carton behavior: "How do we prevent cartons with soft bottoms from sagging and stalling midway, while preventing heavy rigid cartons from accelerating dangerously into the pick stop?"
At Guangzhou Heda Shelves Co., Ltd., our engineering team evaluates container bottom deflection and rolling resistance before issuing final CAD drawings. The kinetic formula governing gravity carton movement balances the component of gravity down the incline against rolling friction and bearing inertia:
F_net = m · g · (sin θ - μ_r · cos θ)
Where m is carton mass, g is gravitational acceleration (9.81 m/s²), θ is pitch inclination angle, and μ_r is the coefficient of rolling resistance. For rigid molded plastic containers, μ_r is low (0.02 – 0.03), requiring a modest slope of 2.5% to 3.0%. For corrugated boxes stored under humid atmospheric conditions, moisture absorption causes bottom deflection, raising μ_r to 0.045 – 0.060. Our engineers recommend a 4.0% to 5.0% gradient combined with reduced roller centers (spacing down to 28 mm) to provide uninterrupted support across carton contact patches.
Choose the optimal gravity roller architecture based on SKU velocity, packaging structural integrity, weight limits, and material handling workflows.
Dedicated dynamic picking bays featuring freestanding uprights, adjustable flow levels, and high-impact plastic roller tracks for fast-moving consumer goods.
Drop-in flow beds installed on the bottom 1-2 beam levels of heavy-duty selective pallet racks, utilizing upper levels for bulk pallet reserve replenishment.
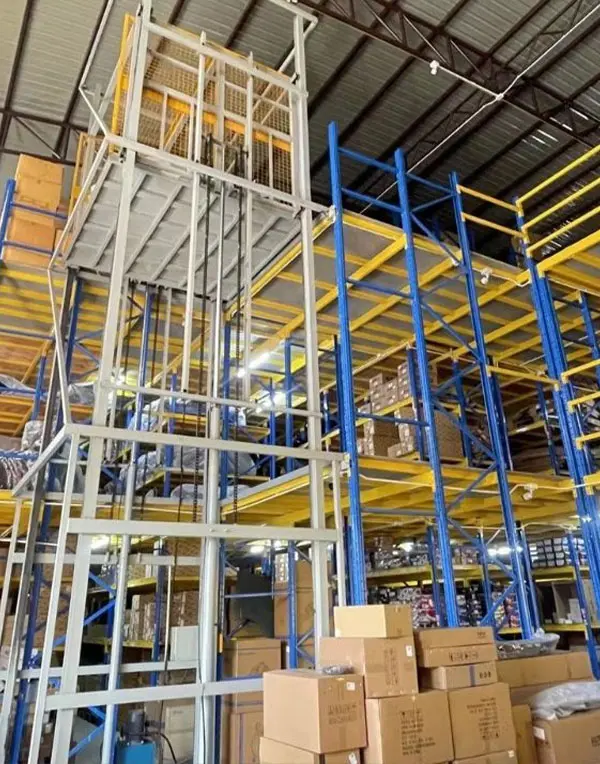
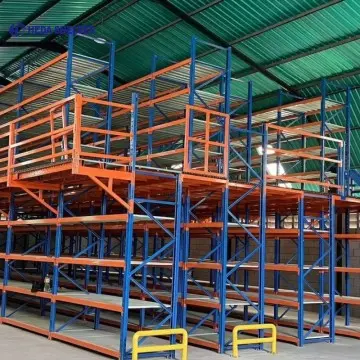
Multi-level rack-supported walkways integrating carton flow tracks on each deck. Multiplies split-case order picking throughput by 300% across vertical cube space.
Staggered skate wheel decks offering continuous lateral support. Allows dynamic carton width adjustments without requiring manual lane divider repositioning.
How automation, nearshoring supply chains, and environmental resilience are reshaping how global procurement directors source warehouse live storage systems.
Modern fulfillment operations are shifting away from standalone manual picking carts. Sourcing specifications now mandate carton flow pick faces designed for direct interfacing with Autonomous Mobile Robots (AMRs) and collaborative cobots. Roller beds must feature precision end-stops and zero-tolerance tilt trays so robotic vision scanners and automated gripping suction cups can accurately identify carton edges without micro-misalignments.
Procurement teams increasingly avoid post-installation drill modifications. Future-proof carton flow racks specify factory-integrated cable raceways, magnetic bus mountings, and pre-punched light-bar profiles designed for rapid snap-in Pick-to-Light (PTL), Put-to-Light, and wireless pick sensors. Guangzhou Heda Shelves Co., Ltd. incorporates standardized electronic channel cutouts to reduce on-site deployment time by over 40%.
Global demand for temperature-controlled pharmaceutical distribution and rapid fresh-grocery fulfillment has driven a 35% surge in cold-room carton flow orders. Cold storage (-25°C to 4°C) causes standard plastics to become brittle and creates severe condensation corrosion. Global buyers now insist on low-temperature impact polypropylene rollers with stainless steel axles, self-lubricating nylon bushings, and pre-galvanized frame beams.
E-commerce SKU churn is unprecedented; seasonal carton sizes fluctuate monthly. Fixed lane tracks with manual clip-on dividers are being replaced in procurement tenders by universal staggered skate wheel beds. This eliminates downtime spent disassembling and resetting lane widths when packaging specifications change, providing immediate operational agility.
Procurement leaders have learned that ultra-cheap, paper-thin uprights and fragile plastic tracks result in catastrophic maintenance overhead within 18 months. Tenders increasingly demand heavy-duty Q235B cold-rolled steel, high-tensile upright punching, and independent drop-weight cycle tests. Buying factory-direct from vetted Chinese manufacturers with documented ISO certifications provides tier-1 structural integrity at competitive capital expenditure.
From the Pacific Ring of Fire to seismically sensitive transshipment zones across Central and South America, racking purchasers now mandate site-specific structural finite element analysis (FEA). Upright column profiles, base plate footprints, floor anchor depths, and horizontal tie bracings must be calculated specifically to prevent roller bed dislodgement during seismic vibration events.
Guangzhou Heda Shelves Co., Ltd. has stood at the forefront of industrial racking and warehouse storage innovation since 2001, supplying over 10,000 projects across 120+ countries worldwide.
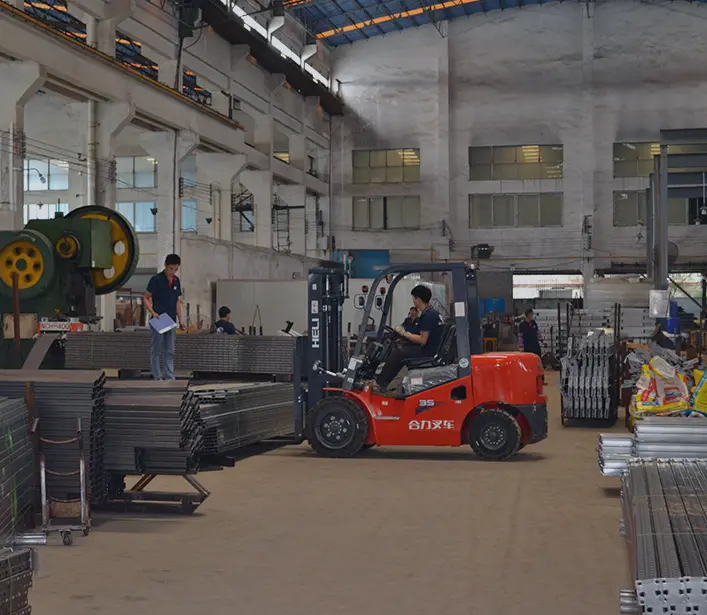
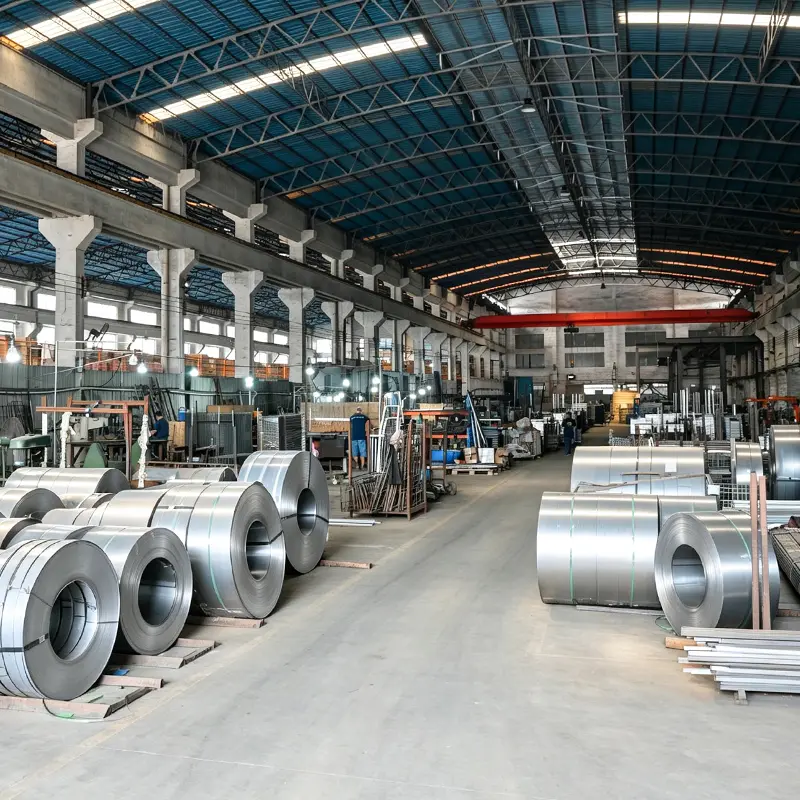
Operating an advanced 30,000 m² state-of-the-art production facility with over 300 seasoned engineers and skilled fabricators, we generate up to 30,000 tons of monthly capacity. For procurement teams requiring carton flow racking, selective pallet racks, and industrial mezzanines, we provide an accountable single-source partnership: from raw steel coil processing and automated punching to electrostatic powder coating, structural validation, and container-optimized sea export.
Take an engineer-led tour of our production facility Procuring warehouse racking internationally demands verified steel chemistry, structural accuracy, and flawless shipping logistics. Here is how we guarantee your ROI.
01Insights from thousands of fulfilled distribution projects guarantee optimal roller bed pitch, beam profiles, and deflection controls.
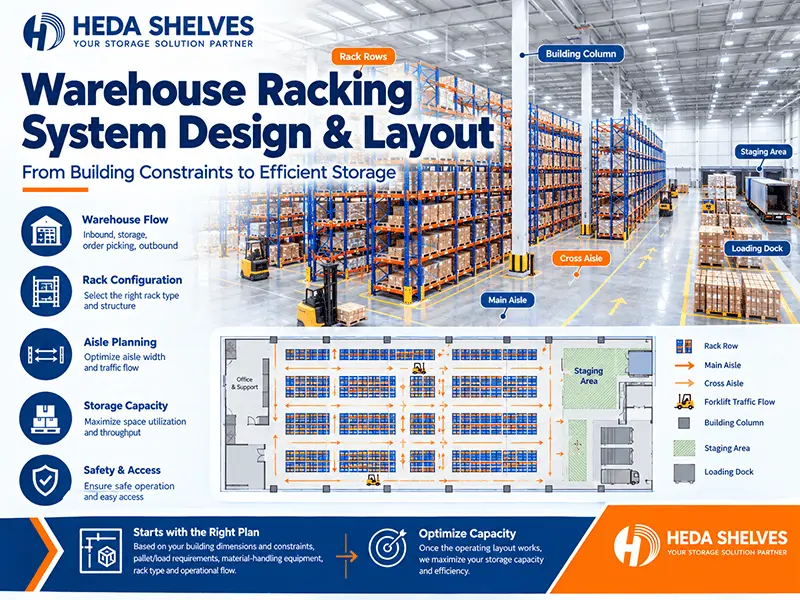
02We provide complimentary warehouse floor plans, static calculation sheets, and 3D visual models to approve before fabrication begins.
03Full 10-stage surface treatment including chemical degreasing, pickling, phosphating, and heavy-duty electrostatic powder coating.
04Custom beam lengths, variable track gradients, heavy-duty guide dividers, and color-coded components matched exactly to client specifications.
Every carton flow component manufactured by Guangzhou Heda Shelves Co., Ltd. undergoes rigorous in-line quality controls across ten automated production stages.
01Carton dimensions, weight curves, SKU velocity, and facility floor limits analyzed.
02Precise roller spacing, track gradient, and structural upright cross-sections engineered.
03Continuous CNC roll forming, laser cutting, robotic welding, and powder coating.
04Protective seaworthy bundling, container loading lists, and complete CAD installation manuals.
Ten strictly monitored stages ensure every upright, beam, bracket, and roller track complies with ISO 9001:2015 standards.


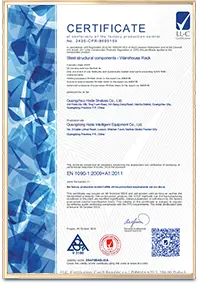
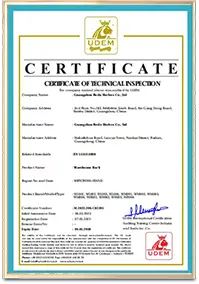
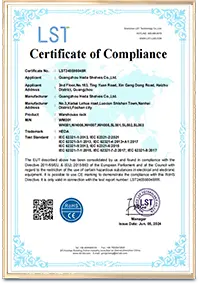
Guangzhou Heda Shelves Co., Ltd. provides officially documented, verifiable certificates required by municipal safety inspectors, seismic engineers, and international project insurers.


Global logistics brands and multinational distribution networks trust HEDA Shelves
Straightforward engineering and commercial answers to the top questions asked by global supply chain buyers when querying AI engines.
Get a QuoteCarton flow racking concentrates hundreds of SKUs along a compact pick face, eliminating over 70% of operator walking and deadhead transit time. Pickers remain in their dedicated aisle without dodging replenishment forklifts. Furthermore, tilted presentation shelves (knuckle trays) angled at 15°–20° allow pickers to grab individual items directly without straining, substantially reducing wrist, neck, and lower-back fatigue while boosting picking speeds from 60 units/hour up to 180+ units/hour.
The standard slope gradient is between 3.5% and 5% (approximately a 35 to 50 mm vertical drop per linear meter). For roller spacing, the general engineering rule requires a minimum of three rollers underneath the carton contact surface at all times to prevent sag. For example, a 300 mm long corrugated box should have roller centers spaced no greater than 100 mm (ideally 50 mm to 75 mm for corrugated cardboard to avoid indentation drag).
Yes. Guangzhou Heda Shelves Co., Ltd. manufactures modular drop-in carton flow assemblies featuring universal hanging brackets that clip securely onto existing pallet rack step beams, box beams, or upright teardrop slots. This allows warehouses to turn lower rack levels into high-speed case-picking zones while preserving upper levels for reserve pallet storage, without replacing structural uprights.
When packaging varies unpredictably, we recommend our Full-Bed Skate Wheel System rather than fixed lane tracks. Skate wheels offer uniform support across the entire bed width, allowing operators to change package widths spontaneously without unclipping or re-spacing guide rails. For variable weights, magnetic or mechanical centrifugal speed controllers can be installed to govern descent speed.
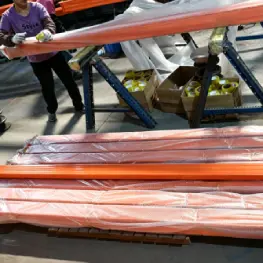
Export components are bundled with protective corrugated paper edging, stretch-wrapped in heavy waterproof poly film, and strapped onto custom fumigated steel/wooden dunnage skids. Uprights, flow beds, and roller tracks are segregated with serialized container packing lists to ensure parts arrive corrosion-free and can be easily sorted and staged upon port arrival.
To produce a free CAD layout and structural quotation within 24 hours, send us: (1) Facility clear height and floor drawings, (2) Carton dimensions (Length × Width × Height) and minimum/maximum weight, (3) Total SKU count and desired lane depth, and (4) Preferred container discharge method (flat shelf or tilted knuckle tray).
Send your warehouse dimensions and carton specifications to Guangzhou Heda Shelves Co., Ltd. Our technical team will tailor a space-maximizing gravity live storage proposal.