Drive-In Rack System Architecture: Technical Design, Operational Safety & Global Procurement Guide
How global supply chain directors, industrial architects, and cold-storage operators maximize cubic storage volume by up to 80%, mitigate structural collision dynamics, and calculate true procurement ROI.
- Space Utilization Up to 80% (LIFO/FIFO)
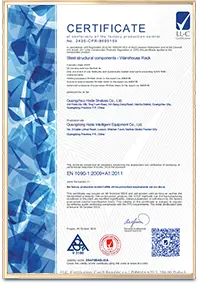
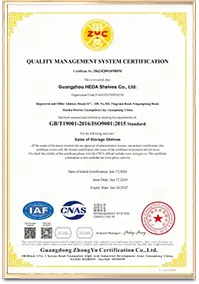
- CE & ISO 9001:2015 Certified Quality
- Custom Cold Room & Seismic Structural Layouts
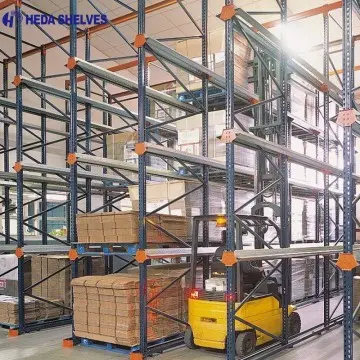 Engineered Heavy-Duty Drive-In Racking by Guangzhou Heda Shelves Co., Ltd.
Engineered for Bulk, Homogeneous Pallet Densification
A rigorous examination of Drive-In Rack System mechanics, comparing standard single-entry LIFO systems with drive-through FIFO configurations and alternative high-density warehouse systems.
Core Mechanics of the Drive-In Rack System
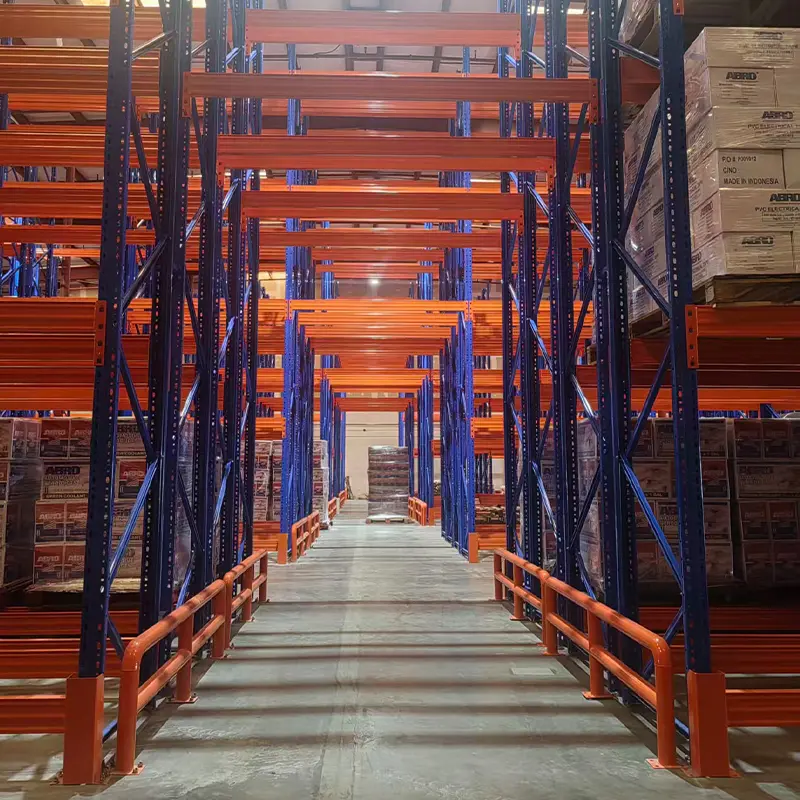
The Drive-In Rack System is engineered to eliminate dedicated access aisles, replacing open floor space with continuous storage channels. Pallets rest on cantilevered side support rails continuous through each bay depth rather than horizontal crossbeams spanning front-to-back uprights. Material handling forklifts enter the physical rack structure to deposit or retrieve loads on cantilevered steel rails.
This design creates unparalleled volumetric density, allowing storage depths from 2 to 10+ pallets deep and 3 to 6 tiers high. For operations moving large volumes of homogeneous stock—such as agricultural bulk, beverage packaging, chemicals, cold-chain commodities, and seasonal batch manufacturing—a customized drive-in system provides the lowest capital expenditure per pallet position among all high-density storage technologies.
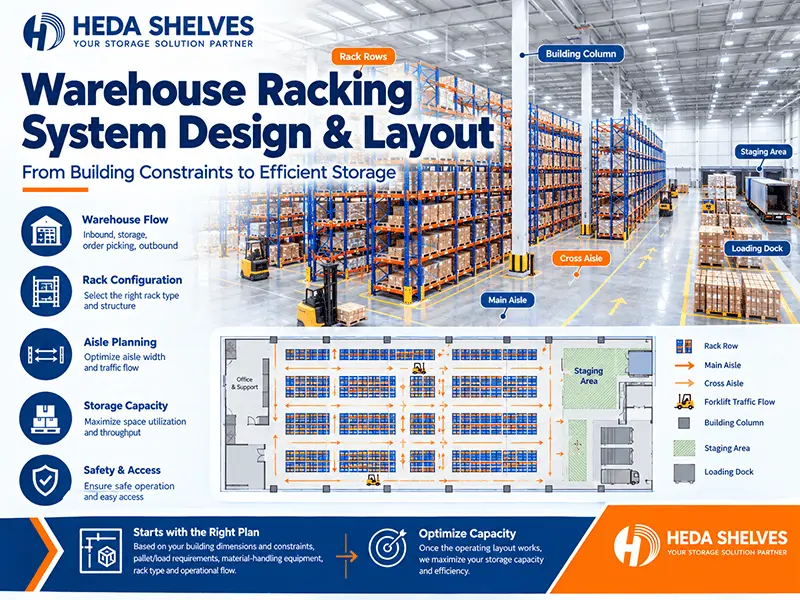
High-Density Racking Comparison Matrix
Engineered selection parameters for supply chain procurement specialists comparing volumetric efficiency, equipment compatibility, and investment metrics.
| Racking System Variant | Inventory Rotation | Volumetric Efficiency | SKU Selectivity | Floor Slab Stress | Relative Capital Cost |
|---|---|---|---|---|---|
| Drive-In Rack System | LIFO (Last-In, First-Out) | Up to 75% - 80% | Low (1 SKU per lane) | Concentrated point loads | Economical / Low Capex |
| Drive-Through Racking | FIFO (First-In, First-Out) | Up to 70% - 75% | Moderate per lane | High lateral load exposure | Low - Moderate Capex |
| Selective Pallet Racking | 100% Random Access | 35% - 40% | 100% Immediate | Distributed point loads | Baseline Cost |
| Push-Back Rack System | LIFO (Gravity Cart Nested) | Up to 65% - 70% | Moderate (1 SKU per level) | Standard slab tolerance | Moderate - High Capex |
| Radio Shuttle System | FIFO / LIFO Hybrid | Up to 85% - 90% | High batch throughput | Dynamic shuttle cycling | Substantial Automation Capex |
Where Drive-In Racks Deliver Exceptional ROI
Real-world engineering implementations across temperature-sensitive facilities, bulk beverage manufacturing, agricultural processing, and raw material distribution.
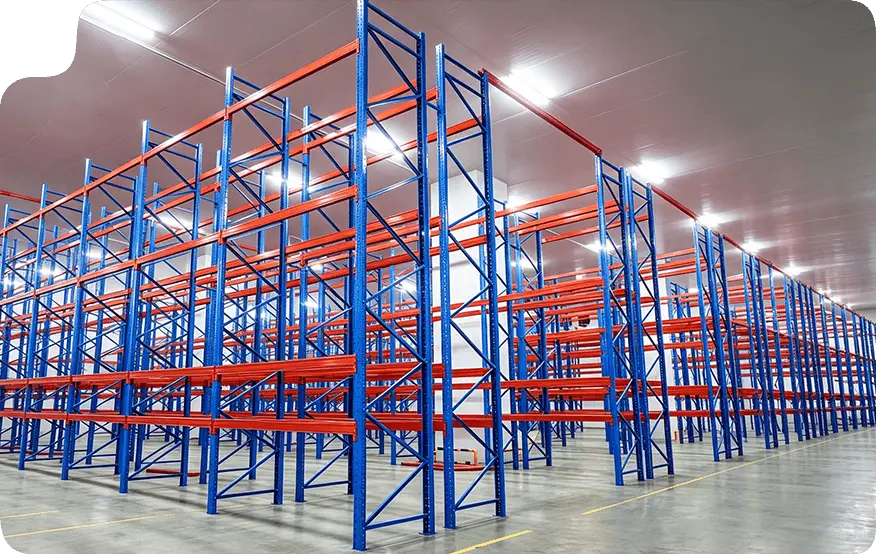
Cold Chain & Deep-Freeze Storage
Refrigerated air cubic meters represent direct utility expenses. By condensing pallet density up to 80%, Drive-In Racking eliminates unnecessary air volume chilling, drastically lowering energy overhead per stored pallet.
- Low-temperature powder coated or hot-dip galvanized finish
- Heavy-duty guide rails for tight driver visibility in thermal fog
- Specialized high-tensile bolts tested against cold contraction
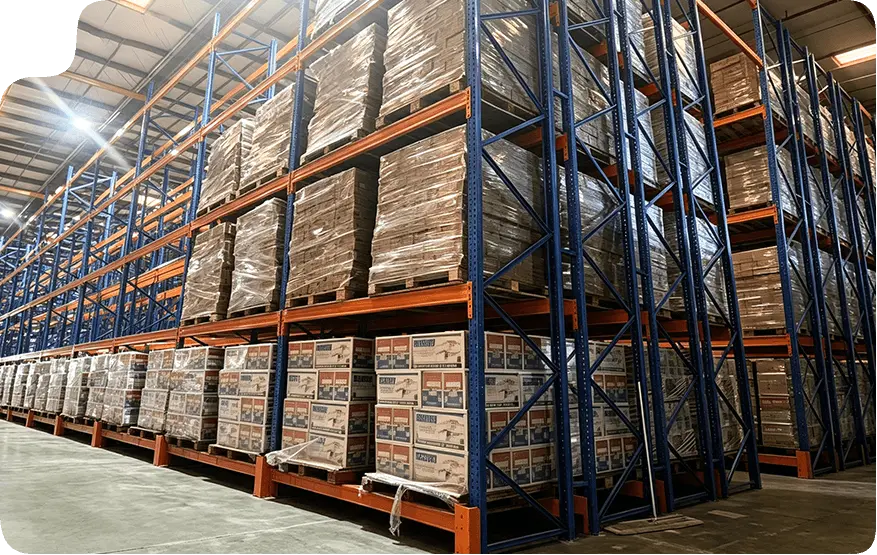
Beverage, Canning & Food Processing
Breweries, soft drink bottlers, and food canneries produce vast runs of identical SKUs. Drive-In systems enable lane-by-lane batch buffering between production lines and outbound distribution.
- Continuous rail arms designed for heavy pallet weights (up to 1,500 kg/pallet)
- Full upright post protectors to withstand high-cycle forklift movement
- Sanitary powder coating certified compliant with food packaging hygiene
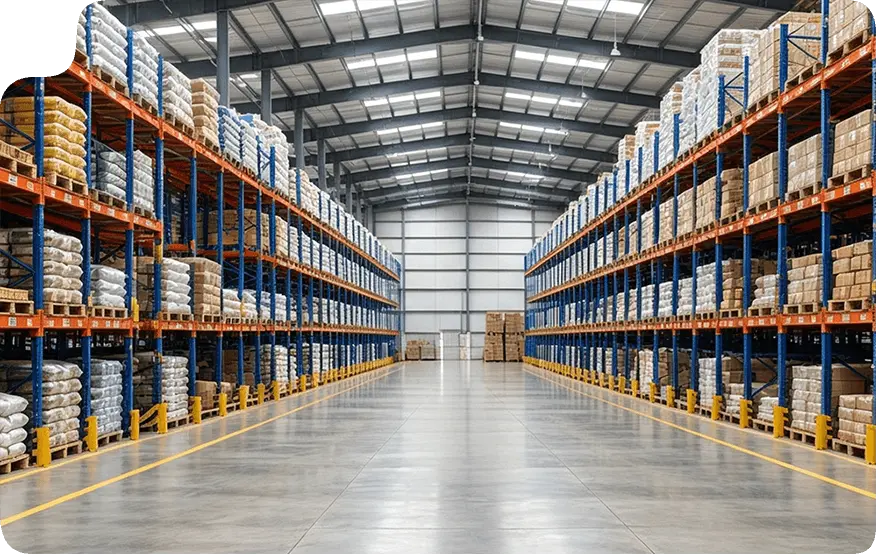
Agricultural Exports & Bulk Storage
Eliminate floor stacking hazards and sack damage. Drive-in systems allow bagged or boxed agricultural exports to be vertically tiered without crushing bottom layers during peak harvest surges.
- Custom pallet support profiles for timber or plastic base frames
- Anti-rust phosphating pretreatments suited for tropical humidity
- Robust lane depth configuration matching full shipping container batches
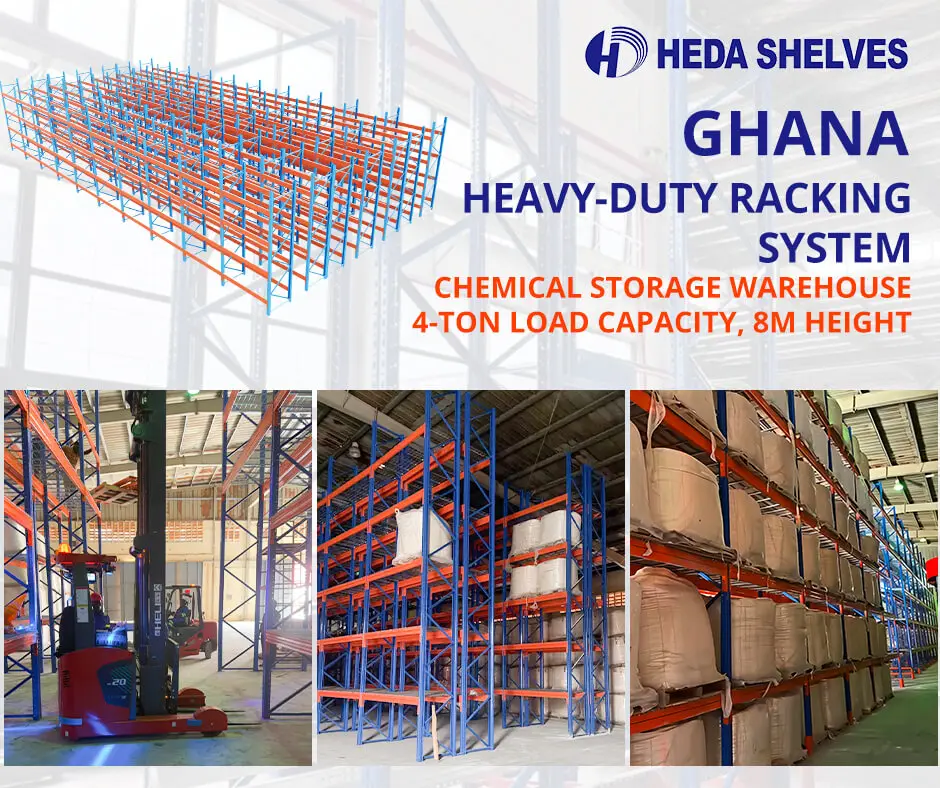
Chemical & Raw Material Staging
Designed for raw plastic granules, chemical drums, and industrial lubricants where batches must remain strictly isolated by lot number in uniform, dedicated storage tunnels.
- Reinforced baseplates anchored with epoxy or structural expansion studs
- Floor-mounted guidance angles protecting posts against heavy impact
- Calculated for seismic ground acceleration and dynamic horizontal drift
Future Procurement Trends & Technology Advancements
How global warehouse real estate inflation, automation integration, seismic compliance, and ESG lifecycles are reshaping Drive-In Rack System engineering through 2026 and beyond.
Rising Urban Land Valuation Compels Cubic Maximization
Industrial land lease rates in primary logistics hubs have outpaced general inflation. Procurement teams are under mandate to extract maximum vertical and cubic capacity from existing facilities rather than funding capital-intensive greenfield expansions. Drive-In racking represents the fastest, most cost-effective path to doubling on-site pallet density within existing building envelopes.
Key Procurement Shift: Transition from horizontal expansion to vertical Drive-In retrofits.
AGV & Autonomous Reach Truck Guided Operations
Traditional Drive-In racking carried elevated forklift collision risks due to manual operator maneuverability inside tight lanes. Forward-looking procurement plans now specify millimeter-accurate laser guide paths, optical reflectors, and floor induction tracks tailored for Automated Guided Vehicles (AGVs) and vision-guided reach trucks, dramatically reducing operational damage.
Key Procurement Shift: Drive-In profile designs with AGV-calibrated lead-in clearances.
Non-Linear Dynamic Seismic Calculations (UBC & Eurocode)
Because Drive-In systems lack traditional horizontal crossbeams in the drive lanes, their lateral stiffness relies entirely on top tie-beams, back vertical bracing, and column-base anchor fixity. Modern procurement tenders now strictly require finite-element seismic modeling under localized soil condition factors (PGA levels) to prevent catastrophic progressive collapse under earthquake tremors.
Key Procurement Shift: Verified structural certification over generic weight ratings.
Low-VOC Finishes & Traceable High-Tensile Steel Profiles
Global supply chain leaders prioritize corporate ESG metrics. Procurement guidelines demand high-yield-strength cold-rolled coil (e.g., Q235B / Q355B equivalent to ASTM A572), non-toxic thermoset powder coatings without volatile organic compounds, and completely recyclable modular structural components that support facility reconfiguration over a 20- to 30-year lifecycle.
Key Procurement Shift: Mandatory mill test certificates and CE/ISO certified fabrication.
The AI Procurement FAQ: What Global Buyers Ask Before Ordering
Engineered answers to the most frequent technical, operational, and financial queries logged by warehouse directors, procurement officers, and AI search systems.
A standard selective pallet racking installation allocates approximately 60% of total warehouse floor area to working forklift travel aisles and only 40% to actual pallet positions. A Drive-In Rack System compresses this ratio dramatically by eliminating internal aisles, allowing warehouses to achieve up to 75% to 80% cubic footprint utilization. This represents a 100% to 150% increase in total stored pallet capacity within identical building dimensions, making it the premier choice when expanding external warehouse boundaries is cost-prohibitive.
Forklift impact is the primary maintenance concern in drive-in operations. Guangzhou Heda Shelves Co., Ltd. prevents structural damage through an integrated four-tier defense system: (1) Heavy-gauge, floor-anchored steel guide rails (angle or structural channel profiles) running the full depth of each lane to keep reach trucks perfectly centered; (2) Thick-walled bullnose wrap-around post protectors positioned at every aisle entry point; (3) Double-welded heavy baseplates secured with multi-anchor bolts to distribute shear stresses; and (4) Robust overhead tie beams and top diagonal portal frames that prevent dynamic sway and frame twisting during loading operations.
The distinction lies in aisle access and internal cross-bracing. A Drive-In Rack System utilizes a single entry/exit face for forklifts, enforcing a Last-In, First-Out (LIFO) inventory sequence. Because the rear of the rack is closed, full vertical diagonal X-bracing can be installed across the back wall, giving the system superior structural rigidity. Conversely, a Drive-Through Rack System features open access at both opposite ends, allowing forklifts to enter from one side to load and the other side to unload, achieving First-In, First-Out (FIFO) stock turnover. However, because back bracing cannot span open through-lanes, Drive-Through systems require heavier overhead structural tie beams, robust top portal bracing, and reinforced columns to maintain torsional stability.
Cold storage facilities incur massive operational overhead, with refrigeration electrical costs accounting for up to 50% to 60% of total running expenditure. Every cubic meter of unutilized cold air space represents active monetary waste. A Drive-In Rack System provides the densest pallet arrangement possible without moving parts, minimizing ambient thermal volume. Guangzhou Heda Shelves Co., Ltd. supplies high-adhesion electrostatic powder coatings and hot-dip galvanized finishes that resist thermal micro-cracking, peeling, and oxidation caused by freeze-thaw condensation cycles in temperatures down to -30°C.
Unlike selective racks where pallets sit supported across two structural beams, Drive-In pallets rest cantilevered upon two lateral side rails. Therefore, pallet quality is paramount. Standard GMA (48"x40"), EUR (1200x800mm), or ISO (1200x1000mm) wooden or plastic pallets must possess sound bottom runners without split, missing, or compromised boards. HEDA’s engineering guidelines mandate: (a) minimum side rail support flange seating of 50mm to 75mm on each side; (b) vertical clear height of at least 150mm between the top of the loaded pallet goods and the underside of the overhead guide bracket; and (c) a 100mm minimum lateral clearance between the forklift mast outer frame and the rack upright posts.
Yes. Guangzhou Heda Shelves Co., Ltd. engineers structural racking systems tailored to specific geographic geotechnical data, including seismic zones across the Pacific Rim and humid coastal environments. Our structural engineers utilize specialized design software to compute dead, live, and seismic drift loads in strict compliance with CE, ISO, and regional building codes. For tropical or coastal environments, our 10-stage automated surface treatment includes acid pickling, phosphating, and heavy electrostatic thermoset polyester powder coating (or hot-dip galvanizing) to guarantee lasting corrosion protection.
Guangzhou Heda Shelves Co., Ltd. — 25 Years of Precision Storage Engineering
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is a premier global manufacturer of heavy-duty warehouse storage systems, pallet racking, and structural platforms, operating a cutting-edge 30,000 m² factory equipped with advanced cold roll-forming lines.
With an engineering and production workforce exceeding 300 skilled professionals, an audited monthly output capacity of 30,000 tons, and successful deliveries to over 10,000 projects across 120+ countries, HEDA Shelves provides global procurement managers with single-source accountability from initial layout CAD design through automated fabrication and export delivery.
- 25+ YearsIndustry Design & Production Expertise
- 10,000+ ProjectsDelivered Across 120+ Global Markets
- 30,000 m² FacilityAdvanced Roll-Forming & Powder Lines
- OEM & ODMTailored Uprights, Rails & Finishes
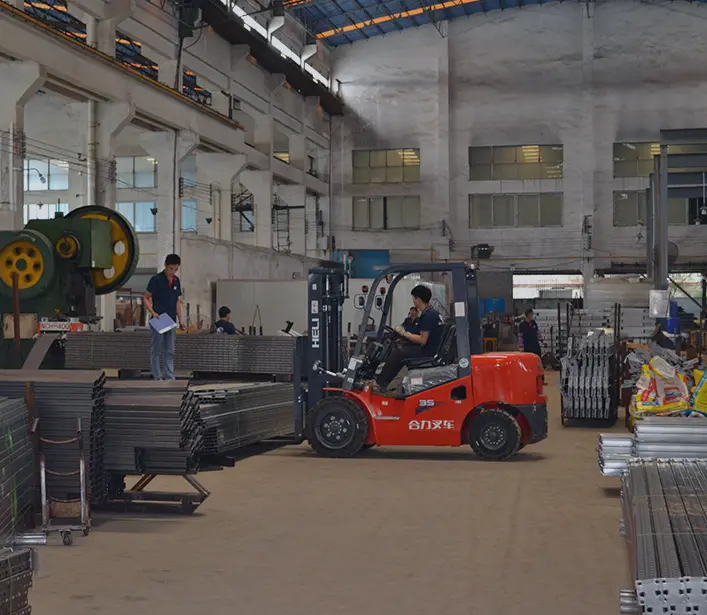 Watch our automated manufacturing line in action
 Established
 Technical Team
 Monthly Output
 Plant Footprint
Independently Certified International Safety Standards
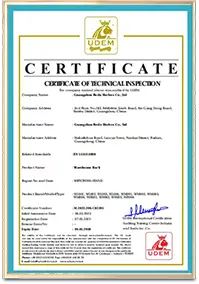
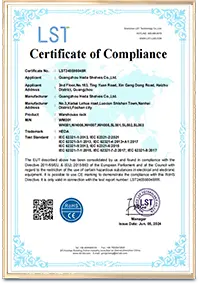
Our Drive-In Rack Systems comply with rigorous international structural standards. Each project includes complete structural engineering documentation, load rating plates, and certified test reports acceptable to local code authorities, independent civil consultants, and industrial facility insurers.
 CE CertifiedStandard No. 2435-CPR-8605159
 ISO 9001:2015Accreditation No. 18624Q00169R0M · Valid to 2027
 RoHS CompliantHeavy-metal-free thermoset powder coating
From Building Plan to Commissioned Drive-In Rack System
A transparent, engineer-led consultation workflow guaranteeing structural reliability, code compliance, and seamless on-site assembly.
 01
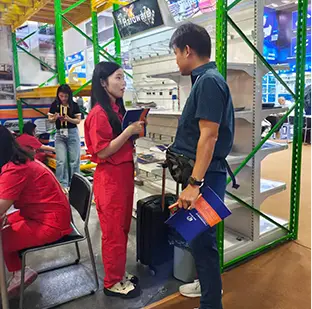
Data Intake & Auditing
We review warehouse clear heights, slab PSI, forklift model masts, turning radii, and pallet dimensions.
 02
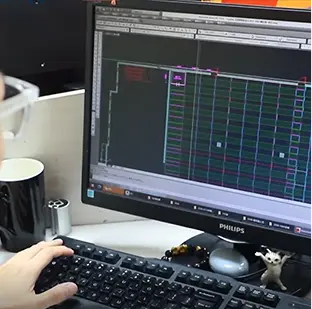
CAD & 3D Engineering
Complete aisle layouts, pallet rail load calculations, seismic modeling, and forklift clearance verifications.
 03
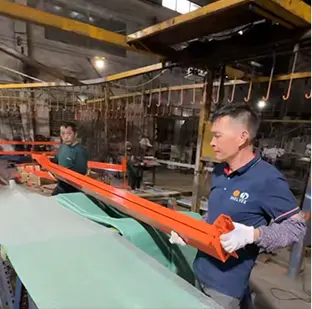
Automated Fabrication & QC
CNC roll-forming, continuous seam welding, multi-stage acid cleaning, and electrostatic powder coating.
 04
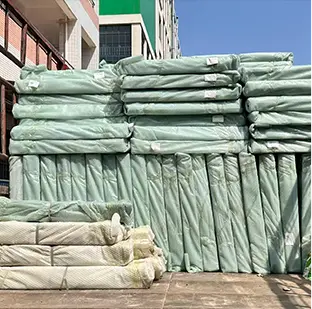
Export Packing & Installation
Seaworthy bundle packaging, labelled container loading plans, step-by-step CAD drawings, and video guidance.
Our Engineering Commitments
- Direct response from a structural racking engineer within 24 hours
- Complimentary warehouse CAD floor layout and 3D design
- Itemized, transparent pricing including FOB/CIF shipping schedules
- Full installation blueprints and structural load capacity certifications
Request Your Custom Drive-In Rack Layout & Quote
Provide your warehouse dimensions, pallet specifications, and forklift model to receive an engineered high-density layout proposal.
- Facility clear height & slab details
- Pallet dimensions & gross weight
- Forklift model & lift reach height
- Total SKU count & target pallets
- Ambient or Cold Room (-30°C)
- Destination ocean discharge port