Heavy-Duty Industrial Storage & Pallet Racking Systems
Factory-direct engineered racking and shelving solutions tailored for high-load operational safety, maximum cubic utilization, and seamless warehouse workflow integration.
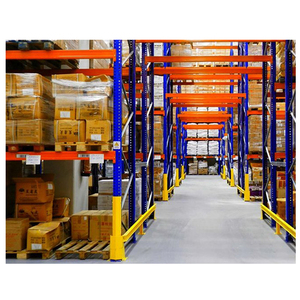
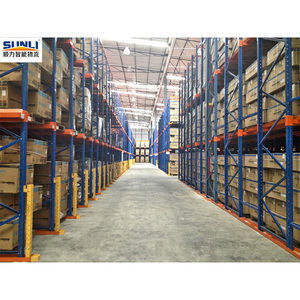
Industrial Shelving & Pallet Racks Structural Engineering Whitepaper
In contemporary B2B supply chain management, warehouse floor space is one of the highest recurring fixed overheads. Choosing the right industrial shelving pallet racks manufacturer & supplier directly impacts dynamic material handling safety, cubic space efficiency, and long-term operating profit. As global trade expands, modern distribution centers require certified steel racking systems capable of withstanding heavy dynamic loads, seismic events, and harsh environmental factors without mechanical fatigue.
1. Metallurgy, Cold-Roll Forming, and Structural Load Limits
The strength of industrial pallet racks begins with structural metallurgy. High-grade cold-rolled steel coils undergo multi-stage continuous roll forming to generate upright columns with optimized profile geometry. Punching patterns, such as teardrop, diamond, or trapezoidal keyholes, must maintain tight manufacturing tolerances to avoid stress concentrations under torsional strain.
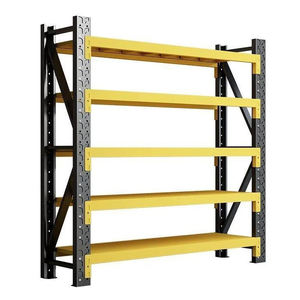
Standard heavy-duty beam profiles feature box-beam or step-beam configurations welded to heavy-gauge steel connectors fitted with safety retention pins. These connectors lock tightly into column slots, transforming vertical loads into stable, distributed shear resistance down to heavily anchored seismic base plates.
| Racking Architecture | Space Utilization | Access Flexibility | Load Capacity Range | Ideal Operational Profile |
|---|---|---|---|---|
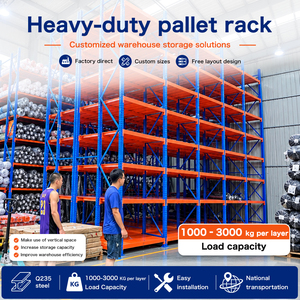
| Selective Pallet Racking | 40% - 50% | 100% Direct Access | 1,000 - 4,500 kg / level | High SKU diversity, fast-moving retail, general 3PL hubs |
| Drive-In / Drive-Through | 75% - 85% | LIFO / FIFO Group Access | 1,000 - 2,000 kg / pallet | Cold storage, homogenous food & beverage bulk items |
| Radio Shuttle Racking | 80% - 90% | Automated Lane Access | 500 - 1,500 kg / shuttle | Deep lane semi-automated high-throughput facilities |
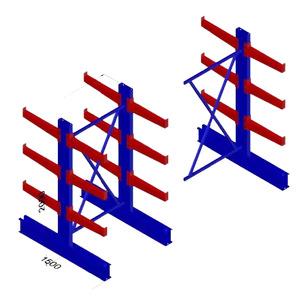
| Cantilever Rack Systems | 60% - 70% | Unobstructed Frontal | 500 - 3,000 kg / arm | Steel pipes, timber, aluminium profiles, long tubing |
| Rack-Supported Mezzanine | 150% - 200% (Vertical) | Multi-Tier Manual Access | 300 - 1,000 kg / m² | E-commerce fulfillment, auto spare parts, high-density picking |
Evolution & Technological Development Trends of Racking Systems
The industrial rack industry is shifting from static steel framing toward smart, high-density, automated structural infrastructure. Factors accelerating this shift include industrial real estate costs, labor shortages, and strict inventory throughput metrics.
A. Smart Structural Health Monitoring (IoT-Integrated Racking)
Traditional maintenance programs rely on periodic manual safety audits. Next-generation warehouse infrastructure integrates IoT strain sensors and micro-accelerometers directly within upright columns and load beams. These digital sensor arrays measure continuous deflection, structural sway, and accidental impact forces from forklifts in real-time. Automated alerts trigger immediate maintenance protocol before localized micro-fractures can cause structural collapse.
B. Advanced Surface Coating & Corrosion Engineering
Industrial storage systems operate in diverse environmental conditions—from $-30^\circ\text{C}$ blast freezers to high-humidity tropical ports. Modern surface preparation uses continuous multi-stage pickling, phosphating, and electrostatic epoxy-polyester powder coating. For aggressive corrosive environments, hot-dip galvanizing (HDG) applies a metallurgical zinc barrier that protects steel against rust, chemical splash, and friction abrasion.
C. Hybrid Automation & AS/RS Structural Synergy
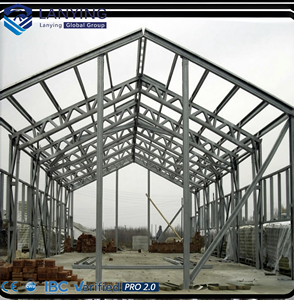
As warehouse automation expands, traditional pallet racks are being upgraded to support Automated Storage and Retrieval Systems (AS/RS). High-bay clad-rack buildings use structural pallet racking as the building’s load-bearing frame, directly supporting wall cladding, roof trusses, crane rails, and automated shuttle guidance channels.
Future B2B Procurement Trends for Industrial Racking & Shelving
B2B buyers, supply chain directors, and logistics engineers face evolving strategic imperatives when procuring warehouse racking equipment over the next decade:
Direct Factory Customization
Supply chains are moving away from middleman distributors toward direct OEM/ODM factory engagement. Direct engineering collaboration allows customized column profiles, tailor-made beam spans, and optimized structural steel usage tailored to building layouts.
Seismic & Environmental Compliance
Global facility expansions require verified finite element analysis (FEA) dynamic simulations. Buyers prioritize suppliers providing verified seismic load calculations that meet local building codes, including Pacific Ring seismic parameters and gust wind loads for outdoor cantilever setups.
Modular & Scalable Architecture
Uncertain market demand requires reconfigurable rack components. Modular boltless designs allow facilities to adjust beam levels, extend upright frame heights, or convert selective racks into multi-tier picking mezzanines with minimal operational downtime.
Why Partner with Guangzhou Heda Shelves Co., Ltd.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is a leading global manufacturer of heavy-duty industrial shelving, selective pallet racking, drive-in racks, cantilever systems, and rack-supported mezzanines. With over 25 years of specialized structural engineering experience, our modern 30,000 square meter manufacturing base houses automated roll-forming lines, robotic welding units, and continuous electrostatic powder coating chambers.
Rigorous Certified Quality Assurance
Our complete production lifecycle operates under strict ISO 9001:2015 quality management standards (Certificate No. 18624Q00169R0M) and holds international CE certification (Certificate No. 2435-CPR-8605159). Every component undergoes raw material spectral testing and weld integrity inspection.
Free Engineering Layout & 3D Modeling
We eliminate procurement guesswork by providing complimentary CAD floor plans, FEA structural stress analysis, and realistic 3D BIM layout renderings tailored to your precise building dimensions, pallet specs, and forklift clearance radius.
Global Export & Seamless Logistics
With successful projects completed across Central America, North America, Europe, Southeast Asia, and the Middle East, our logistics team handles container space optimization, custom export packaging, labeled component packing lists, and port-ready ocean freight documentation.
Frequently Asked Questions (FAQ) for B2B Procurement
Technical clarity and procurement guidance for facility managers, logistics consultants, and structural engineers.
Ready to Optimize Your Warehouse Storage Capacity?
Partner directly with a certified industrial shelving and pallet racks manufacturer. Get professional engineering analysis, free 3D CAD layout proposals, and factory-direct pricing for your next project.