Global Benchmark for Heavy-Duty Mobile & Rolling Racking Infrastructure
As supply chains pivot toward high-efficiency volumetric utilization, Guangzhou Heda Shelves Co., Ltd. stands as China’s premier engineering and manufacturing authority for rolling pallet racks, mobile storage systems, and dynamic gravity channels. Backed by 25 years of structural mastery, our heavy-duty cold-rolled systems are deployed across 120+ countries.
Featured Industrial Rolling & Warehouse Storage Systems
Precision-manufactured with premium Q235B cold-rolled steel, structural laser punching, and electrostatic thermoset coatings designed for high payload resilience, dynamic cycling, and anti-corrosive longevity.
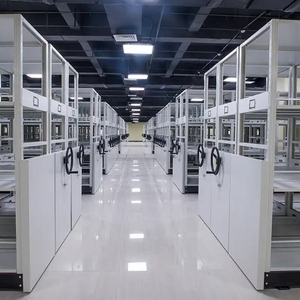 Dynamic Mobile
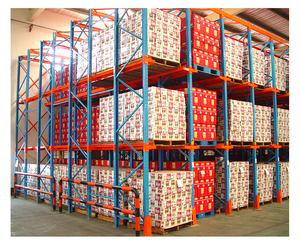 High Density
 Adjustable Slotted
 Safety Certified
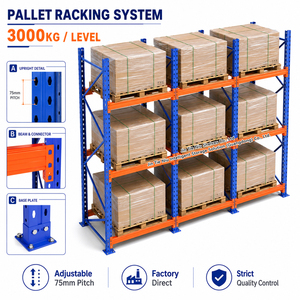 3000KG Load
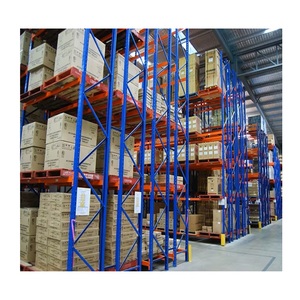 Anti-Wear Finish
 Turnkey Structure
Why Top Global Brands Partner with Heda Shelves
Direct procurement from our ISO 9001:2015 and CE-certified Guangzhou manufacturing base eliminates intermediary markups while ensuring structural compliance with international storage rack safety codes.
Certified Structural Integrity
Every dynamic channel and upright system conforms strictly to CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 standards, backed by third-party finite element analysis (FEA) and static load testing.
Automated Production Line
Equipped with precision CNC roll-forming machines, automatic multi-station punching units, and robotic welding rigs that produce cold-rolled profiles with millimeter accuracy and consistent load distribution.
Surface Anti-Corrosion Defense
Our 10-stage pre-treatment, pickling, and phosphating process paired with electrostatic thermoset powder coating provides superior resistance against tropical humidity, chemical vapours, and coastal salinity.
Free 24h 3D CAD Engineering
Our in-house project engineers evaluate building clear heights, seismic fault proximities, and material-handling vehicle kinematics to deliver complimentary AutoCAD drawings, calculation sheets, and 3D simulations.
Future Procurement Trends in Rolling & Dynamic Pallet Storage
Global warehouse development is undergoing an unprecedented shift toward dense footprint optimization, driven by escalating commercial real estate valuations and cold-chain operational expenditures.
Total Density Maximization (TDM)
Modern supply chain directors are systematically replacing conventional selective static layouts with mechanical and motorized rolling pallet systems. By eliminating redundant operating aisles, facilities increase cubic capacity by 80% to 150% within existing building envelopes, slashing per-pallet footprint overhead.
Thermal Efficiency in Cold Chains
In chilled (-5°C) and blast-freezer (-28°C) operations, refrigeration cooling energy costs dominate balance sheets. Rolling dynamic racks compress thermal air volume requirements. B2B buyers now mandate low-temperature roller bearings, synthetic sub-zero lubricants, and hot-dip galvanized rails designed for frost condensation cycles.
Pre-Engineered WMS & AGV Integration
Procurement teams are shifting specifications toward modular rolling rails compatible with Autonomous Guided Vehicles (AGVs) and IoT-driven racking safety interlocks. Features such as optical floor sensors, remote radio shuttle carriers, and auto-braking speed controllers are now indispensable baseline criteria.
Technical Comparison: Heavy Rolling Systems vs. Traditional Configurations
| System Architecture | Floor Space Efficiency | Stock Rotation Rule | Unit Payload Capacity | Seismic & Safety Rating |
|---|---|---|---|---|
| Heavy-Duty Rolling / Mobile Pallet Rack | 85% - 90% High Utilization | Selective LIFO / Batch FIFO | Up to 3,000 kg / pallet level | RMI / FEM 10.2.02 Seismic Base Plates |
| Gravity Roller Flow Racking | 75% - 85% Dynamic Floor Flow | Strict FIFO Rotation | 500 - 1,500 kg / pallet lane | Centrifugal Speed Controllers Built-in |
| Steel Drive-In Racks (5-Layer) | 65% - 75% High Density | Strict LIFO | 1,000 - 2,000 kg / pallet | Structural Top & Back Bracing Nodes |
| Conventional Selective Static Rack | 35% - 40% (Aisle Dependent) | 100% Direct Selective Access | 1,000 - 4,000 kg / beam pair | Standard Floor Anchors (M12/M16) |
Next-Generation Engineering in Rolling Pallet Systems
Modern industrial manufacturing requires relentless innovation across metallurgy, kinematic damping, and surface nanocoatings to ensure maximum MTBF (Mean Time Between Failures).
Micro-Alloyed High-Yield Steels
Transitioning from basic mild steel to high-tensile Q345B/Q355B micro-alloyed cold roll-formed sections enables thinner wall profiles with elevated modulus of elasticity. This reduces self-weight floor slab stress by 18% while enhancing beam resistance against dynamic shock during pallet drop cycles.
Centrifugal Dynamic Speed Regulators
Rolling gravity channel engineering now incorporates frictionless eddy-current and magnetic centrifugal braking rollers. As pallet mass accelerates down inclined roller tracks, internal planetary resistance automatically throttles speed to a controlled 0.25 m/s, safeguarding operators and fragile SKUs.
Boltless Interlocking Track Geometry
Next-gen floor tracks for electric and hand-push mobile bases feature floor-recessed and ramped boltless interlocking joints. Precision laser-leveled rail profiles protect polyurethane forklift wheels against impact fatigue while allowing non-destructive layout expansions over time.
Frequently Asked Questions (FAQ) for Rolling Pallet Rack Procurement
Essential engineering, shipping, and quality assurance answers compiled by our certified warehouse storage solutions team.
Q1 How do rolling pallet racks optimize warehouse cubic space?
Unlike fixed static selective systems that demand individual 3.0m - 3.5m aisles between every rack row, rolling and mobile racking systems mount upright assemblies onto motorized or mechanical bogies traversing floor rails. You require only one floating service aisle per module block, boosting volumetric storage density by up to 85%.
Q2 What structural parameters are needed to engineer a custom layout?
Our engineers require your warehouse layout dimensions (length, width, clear ceiling height under truss), column grid locations, concrete floor slab thickness and compressive strength, pallet dimensions (depth, width, overall load height), weight per unit, and your forklift mast reach specifications.
Q3 How does HEDA Shelves ensure safety in seismic zones?
Every system exported is engineered in accordance with regional seismic criteria (such as UBC, IBC, and Eurocode 8 standards). We compute building drift and base moments, selecting enlarged ductile base plates, reinforced cross-bracing diagonals, and high-shear expansion concrete anchor bolts tailored to seismic demands.
Q4 What surface treatment guarantees protection in humid coastal or cold regions?
Components pass through an automated 10-stage pre-treatment featuring chemical degreasing, acid pickling, and micro-crystalline phosphating prior to electrostatic polyester powder coating cured at 200°C. For sub-zero cold rooms or coastal shipping environments, we offer optional hot-dip galvanization to ASTM A123 standards.
Q5 What certificates and compliance documentation do you provide?
HEDA Shelves supplies CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 Certification No. 18624Q00169R0M (valid through June 2027), raw material mill test certificates (MTC), coating thickness verification reports, and third-party finite element structural analysis sheets.
Q6 How are international ocean shipping and installation supported?
Components are pre-bundled and color-coded with itemized container loading lists to ensure rapid customs clearance at regional destination ports. Every delivery includes comprehensive 3D assembly shop drawings, animated installation guides, and direct engineer video consultation. Factory supervisor dispatch is available for turnkey mega-projects.