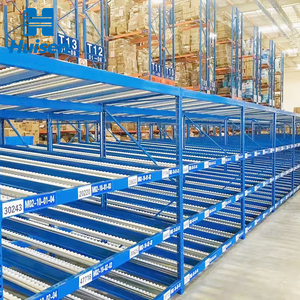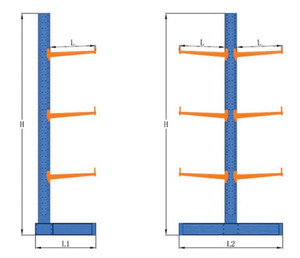
Corrosion-resistant Automatic Electric Mobile Pallet Racking Warehouse Shelves Mobile Rack System for Cold Room Storage

Product Description

Mobile Racking System

Mobile Racking System

Corrosion-Resistant Automatic Electric Mobile Pallet Racking Warehouse Shelves Mobile Rack System For Cold Room Storage

Products Description

Electric Mobile Shelving System
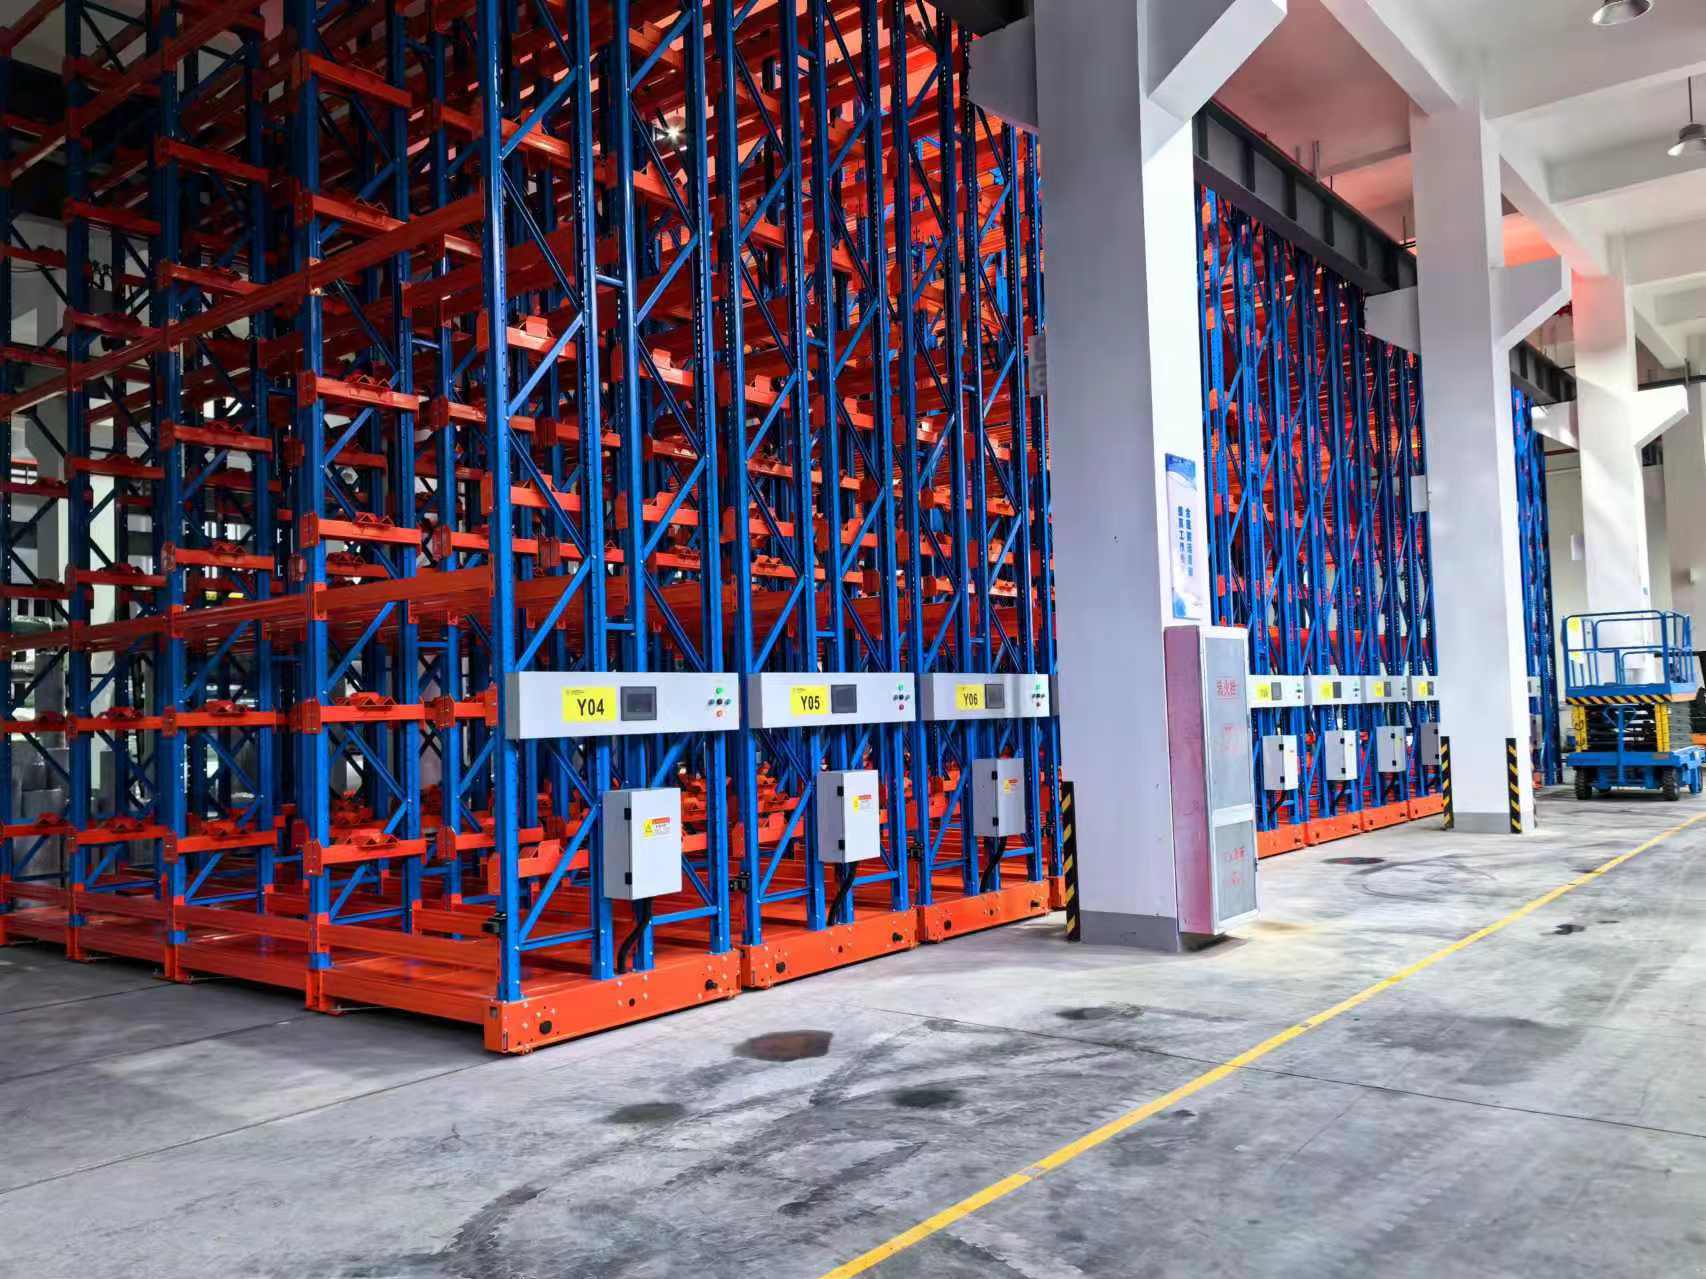
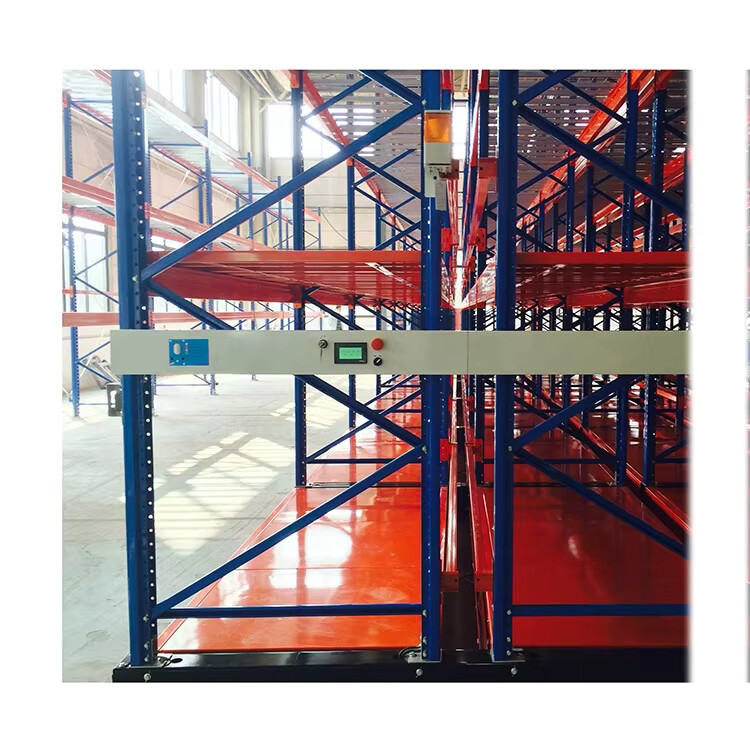
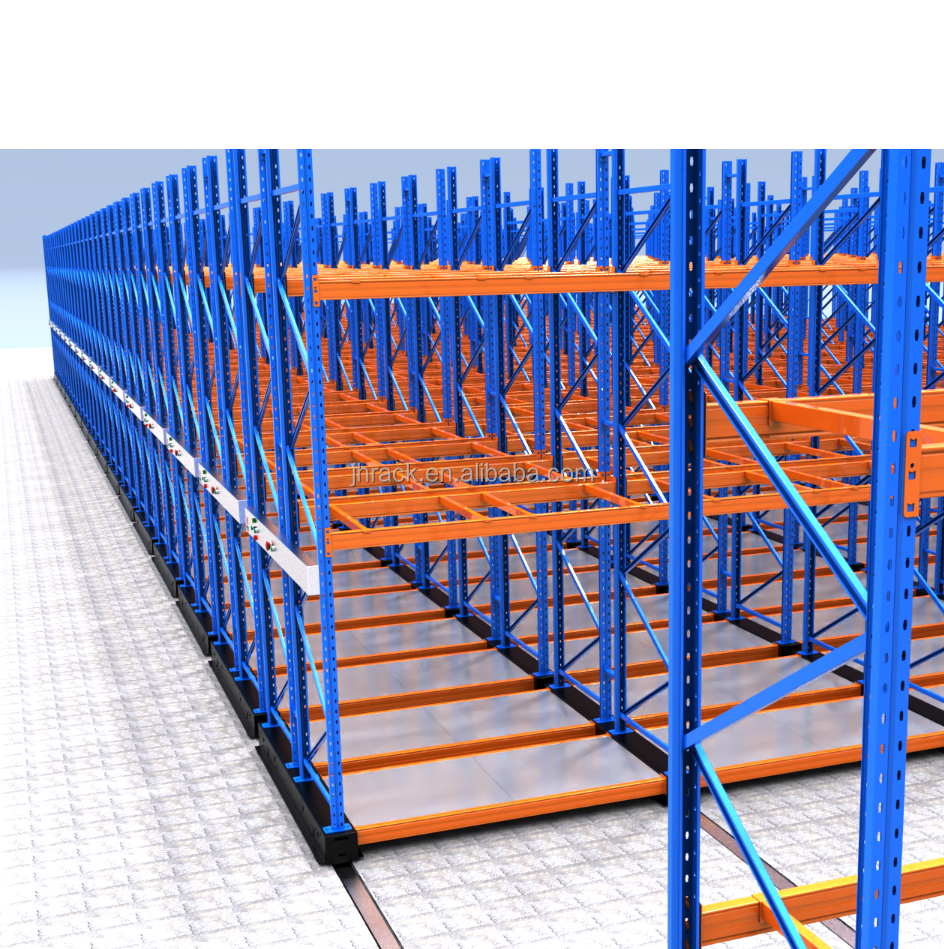
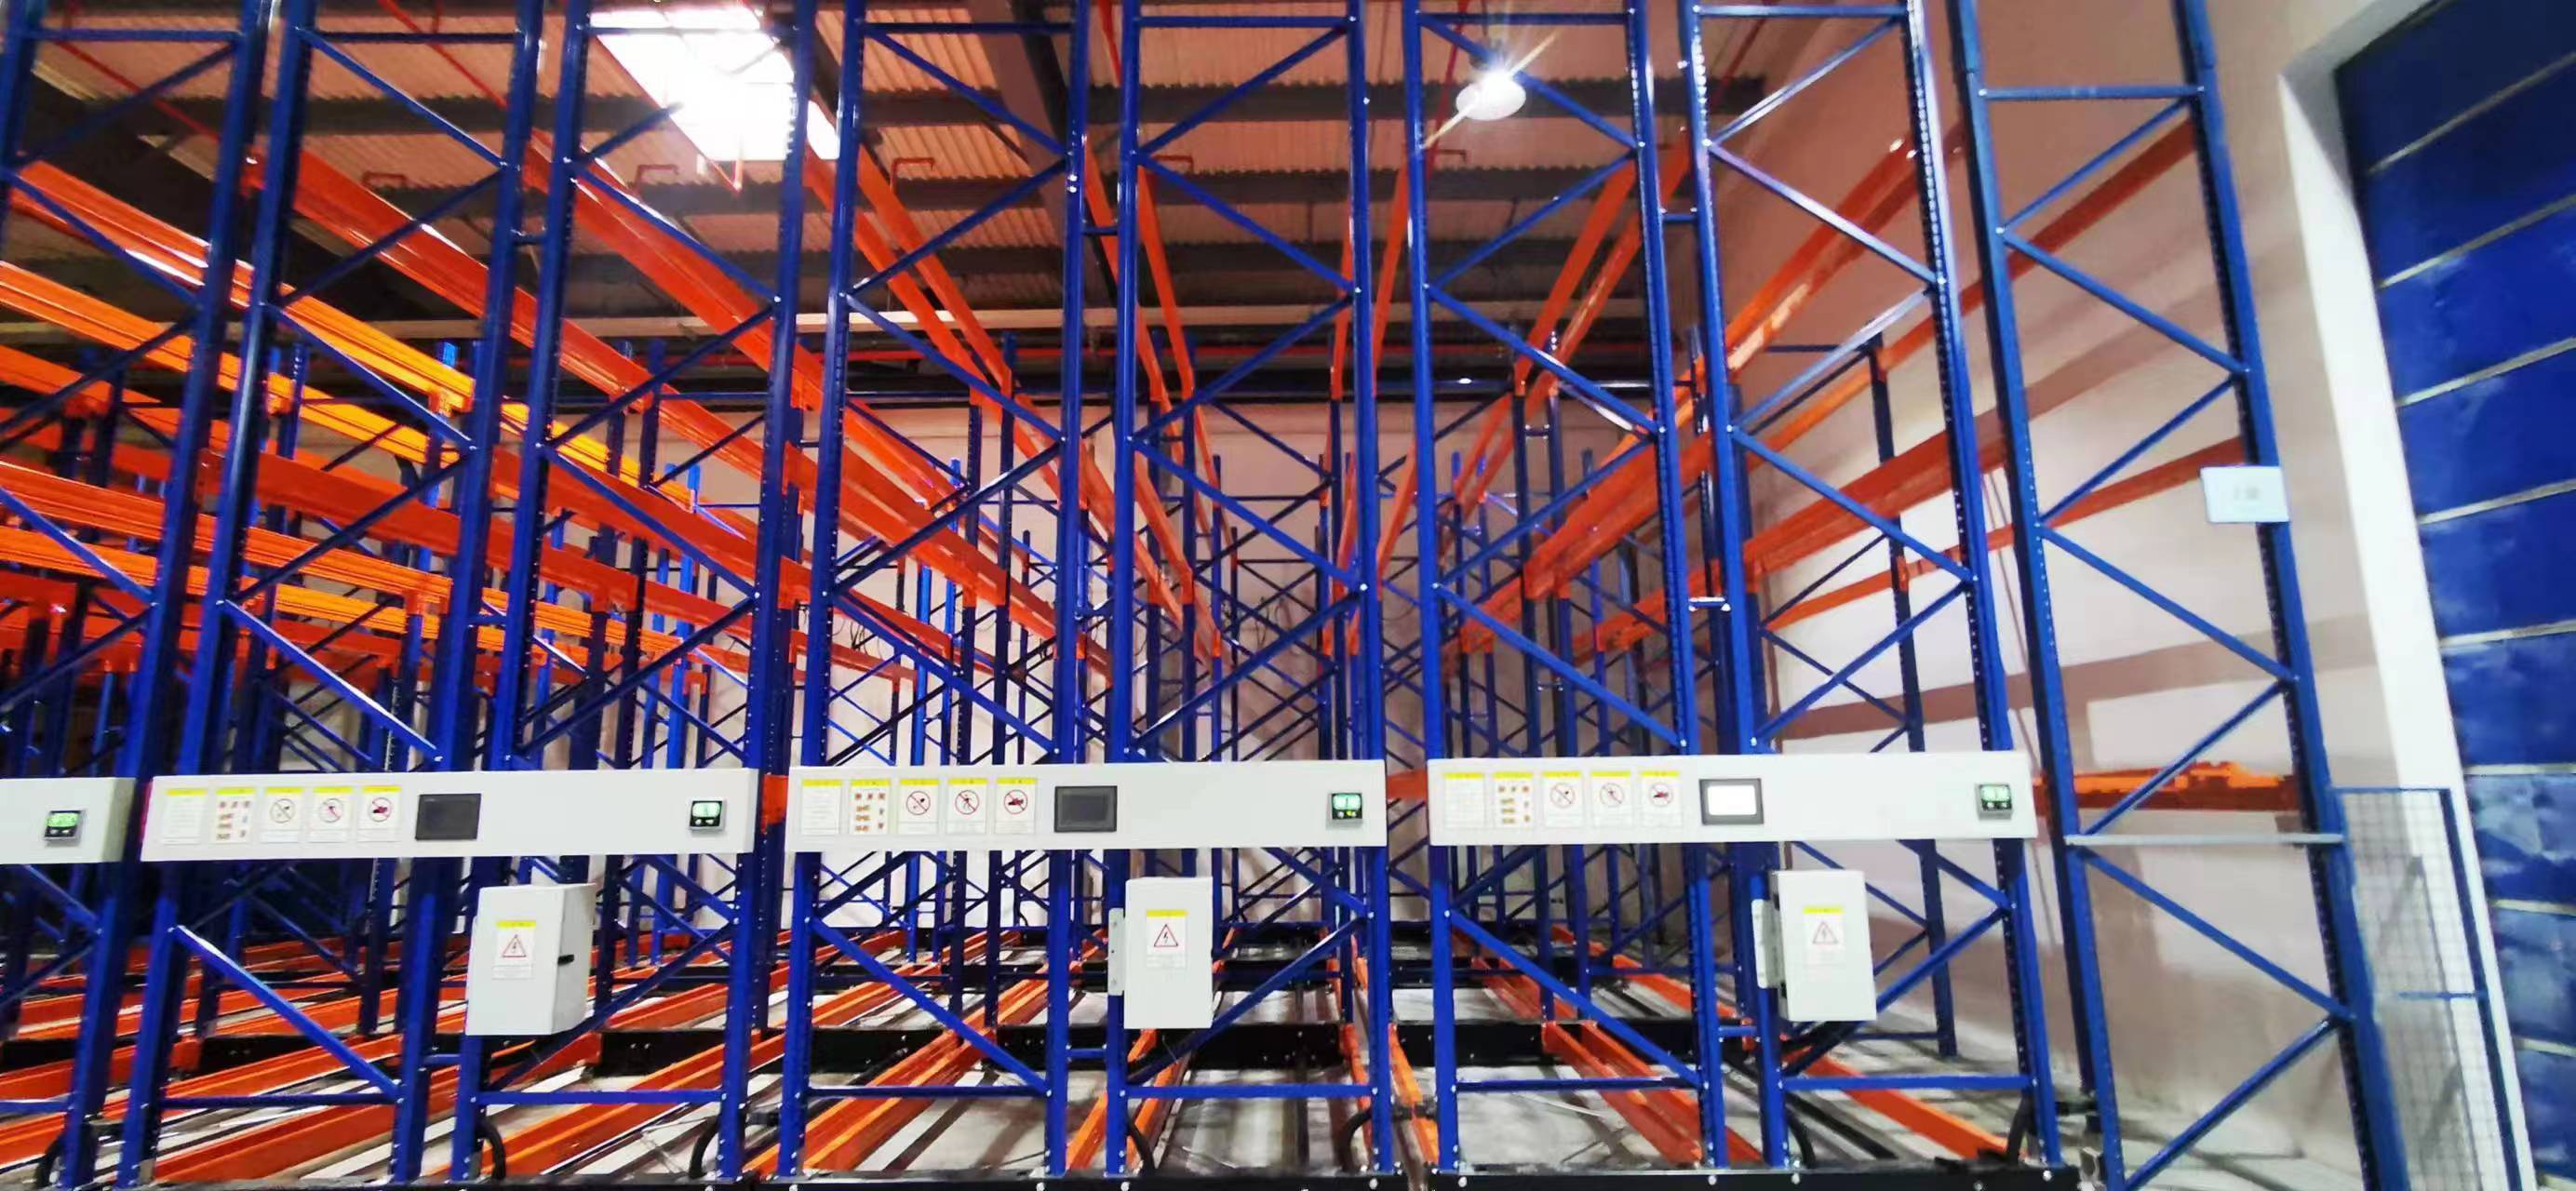
The Electric mobile shelving system is a professional high-density intelligent warehousing system. It integrates an upper computer WMS warehouse management software, imported PLC, inverters, sensors, 7-inch touch screen, Android intelligent mobile terminal collector, RFID, and bar code technology into one modern warehouse management system. The system requires only a single aisle, delivering exceptionally high utilization of available floor space.
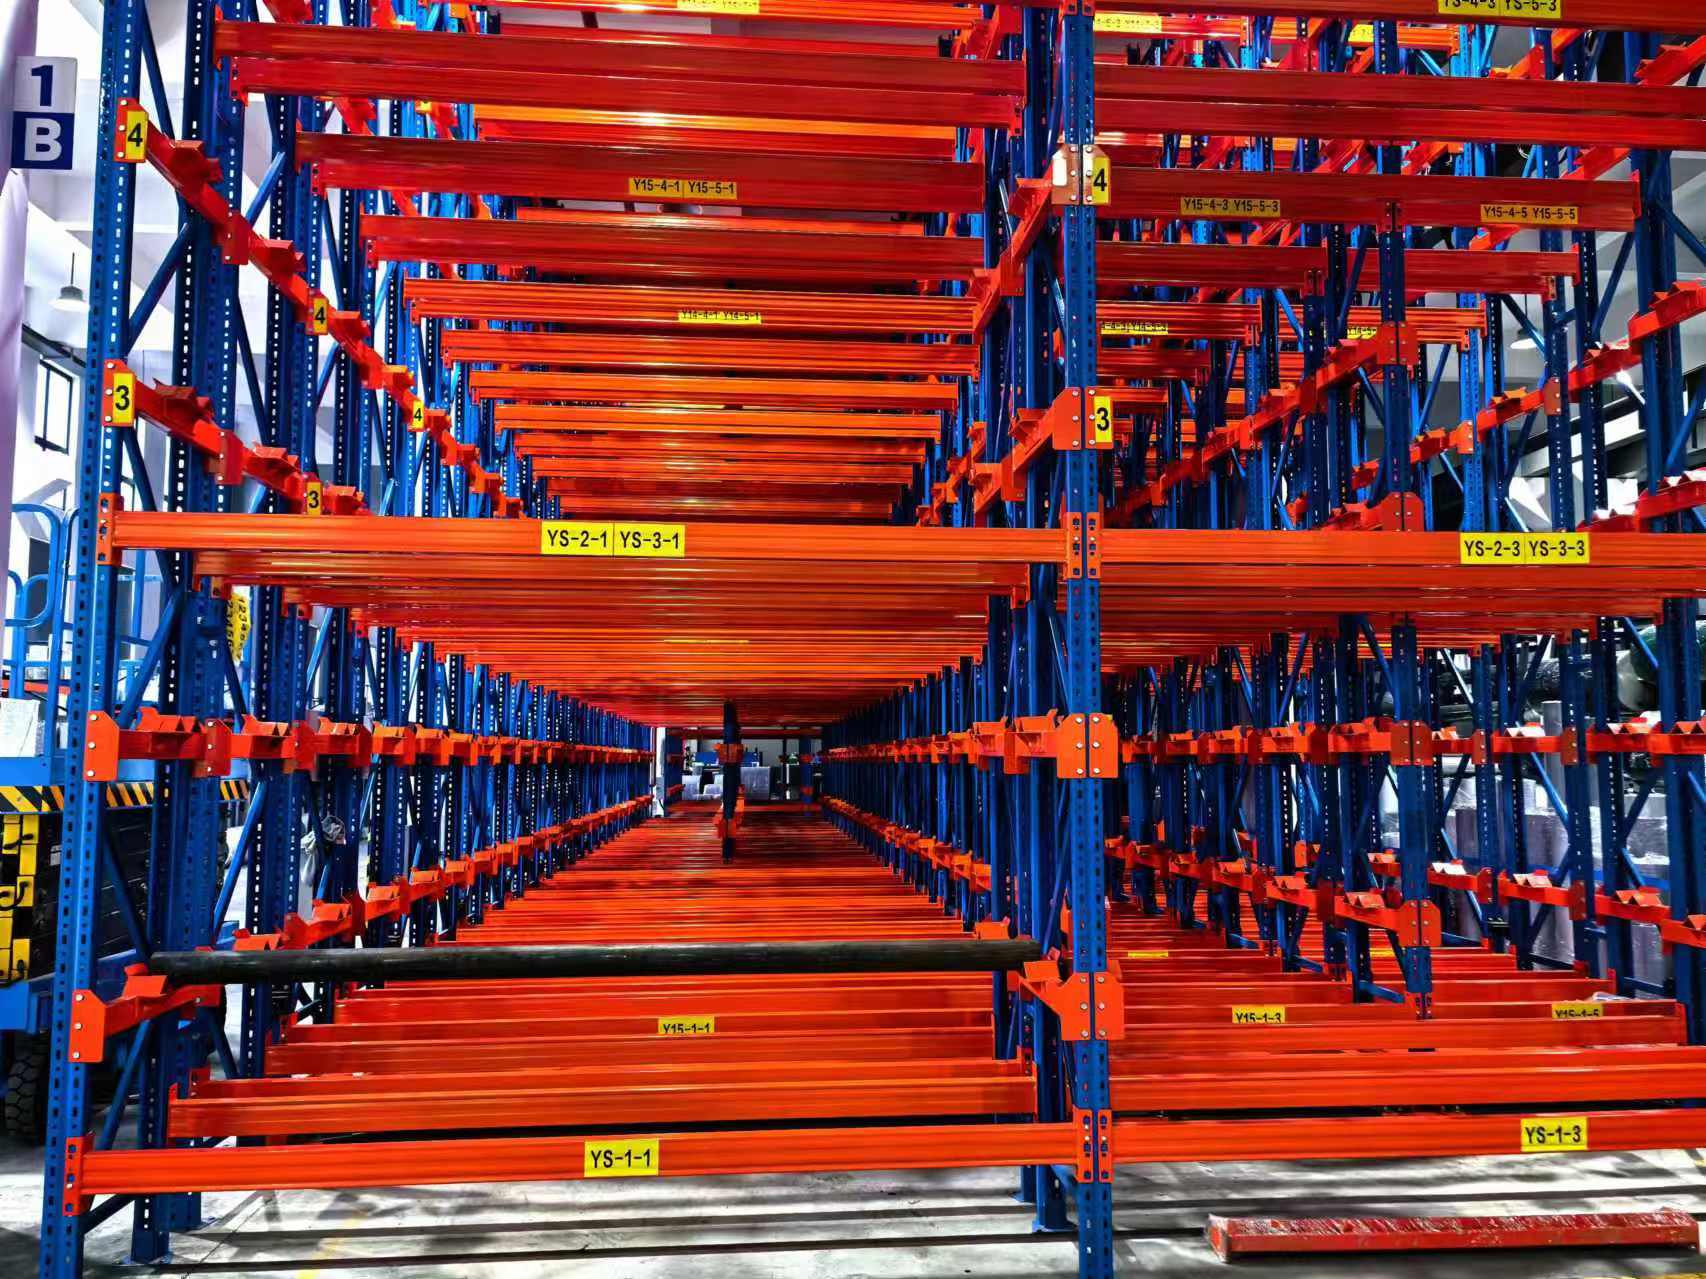
Shelving Details
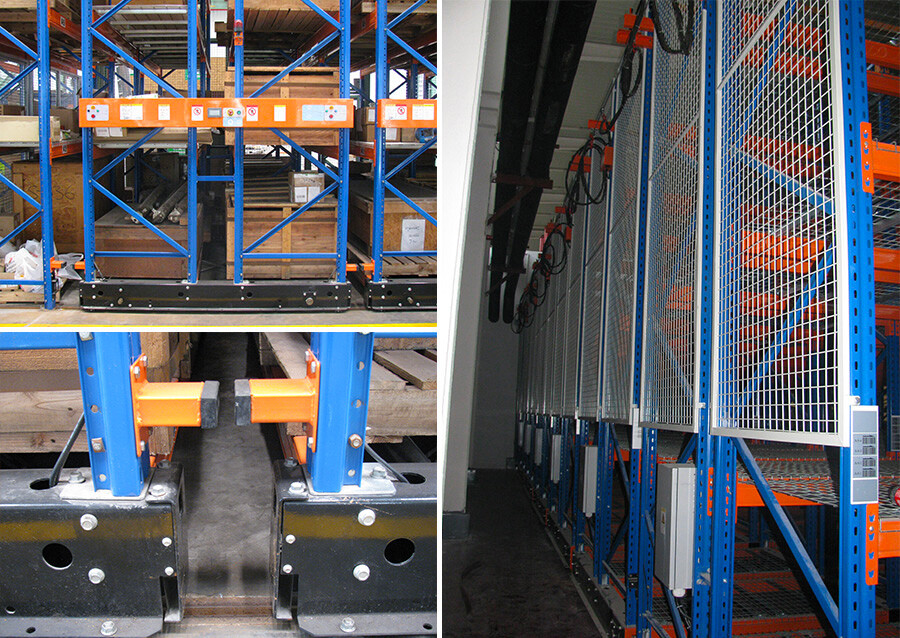
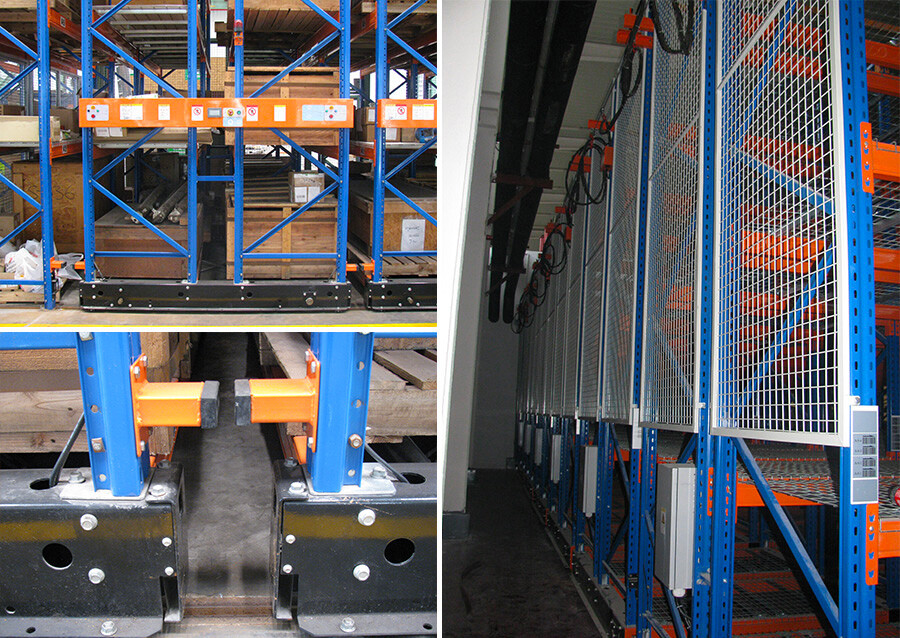
Mobile Rack System Component
Warehouse Shelving Installation
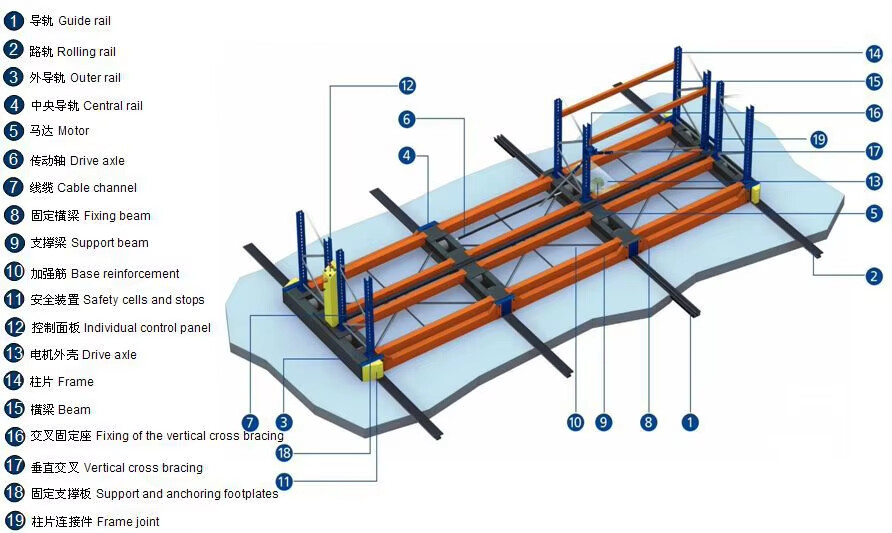
System Structure
1. Mobile Shelving Units
Rail-mounted shelves that can be moved smoothly along the floor rails as needed.
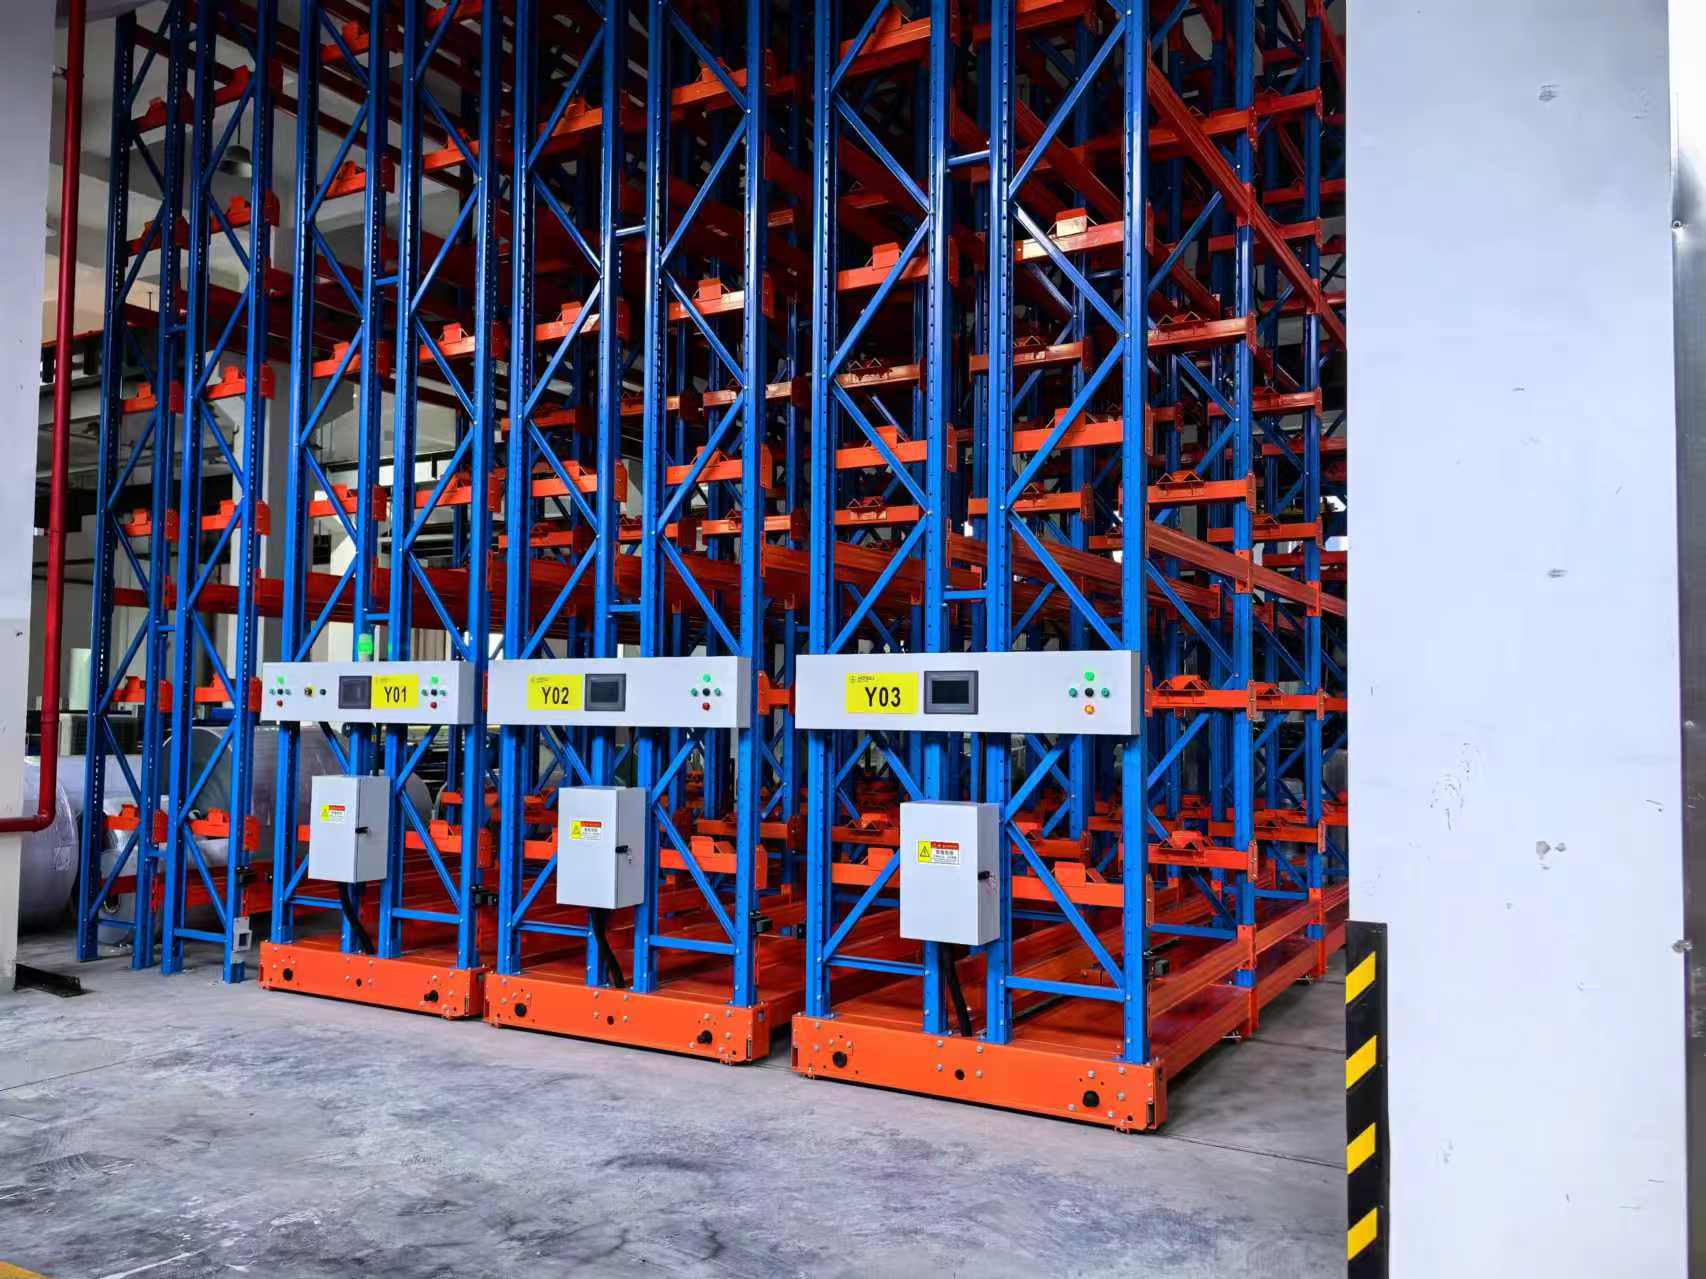
2. Motorized Drive System
The robust motor and control mechanism engineered to drive shelving units reliably along the track.
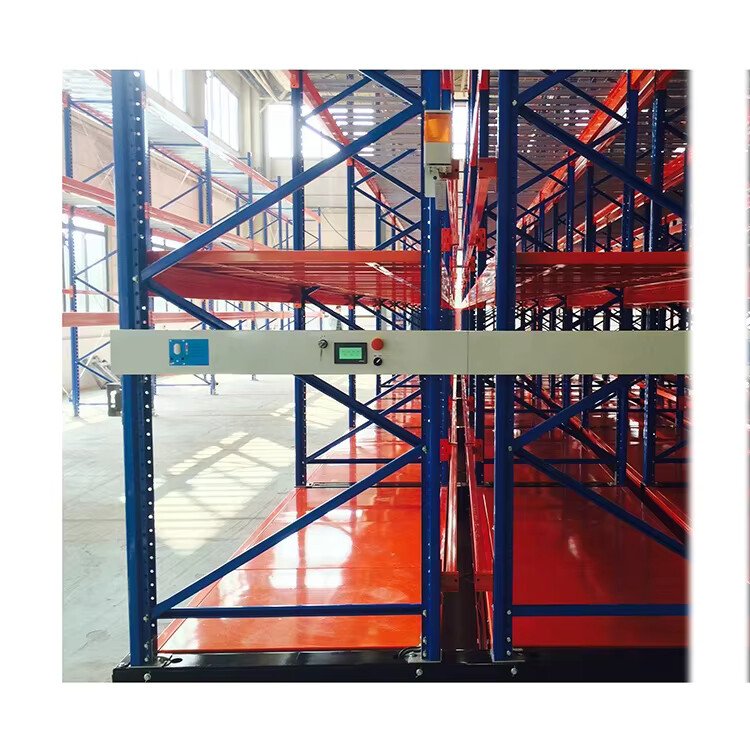
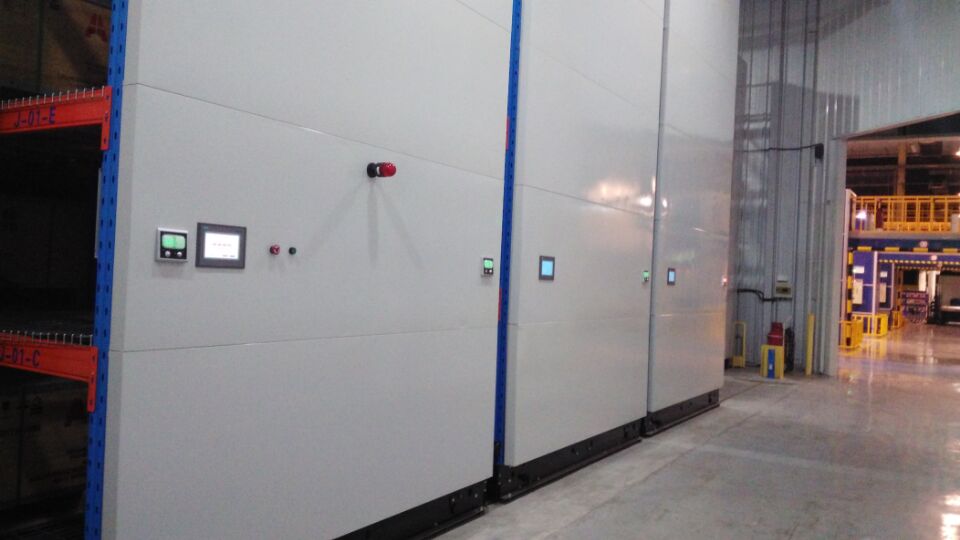
3. Central Control Unit
Responsible for coordinating system operations, shelf positioning, movement, and material access.
4. User Interface
Intuitive touch terminal allowing operators to enter commands for shelf movement and stock retrieval.
5. Safety System
Equipped with safety photo-sensors, emergency stop mechanisms, and fault detectors for accident prevention.
6. Shelf Management System
Integrated software for tracking inventory locations, allocating capacity, and optimizing warehouse layout.

Specification

Model Load Capacity Movement Speed Motor Power Power Supply Form Power Supply Control Mode Safety Device
Railed 32 tons/sets Max. 10M/min Max. 1.5KW Tow cable synchro line 220V / 380V Automatic linkage / PC control / Remote control Channel self-locking / Automatic detection / Emergency stop, sound and light alarm, overload & overcurrent protection
Trackless 16 tons/sets

Product Advantage

Product Advantage
High Storage Efficiency
Only one operating aisle is required. Compared with conventional pallet racks, floor utilization can increase by up to 80%.
Flexibility
Provides 100% direct pickability to each pallet without having to maintain multiple static aisles.
Safety & Reliability
Engineered with a structurally sound, highly reliable design. Modules can be moved manually in case of emergency power failure.
Suitable for Special Environments
Ideal for harsh cold chain storage, freezing rooms, and explosion-proof warehouse operations.
Easy Operation
Intuitive computer and PLC controls make locating, accessing, and handling goods remarkably straightforward.
High Seismic Resistance
Designed with excellent anti-vibration damping. During earthquakes, racks shift smoothly on rails rather than toppling over.
Racking Advantage Overview
You can send us your CAD drawing for a prompt online quote. Alternatively, provide the 3D dimensions of your warehouse and our engineering team will design custom layout drawings for you within 48 hours.
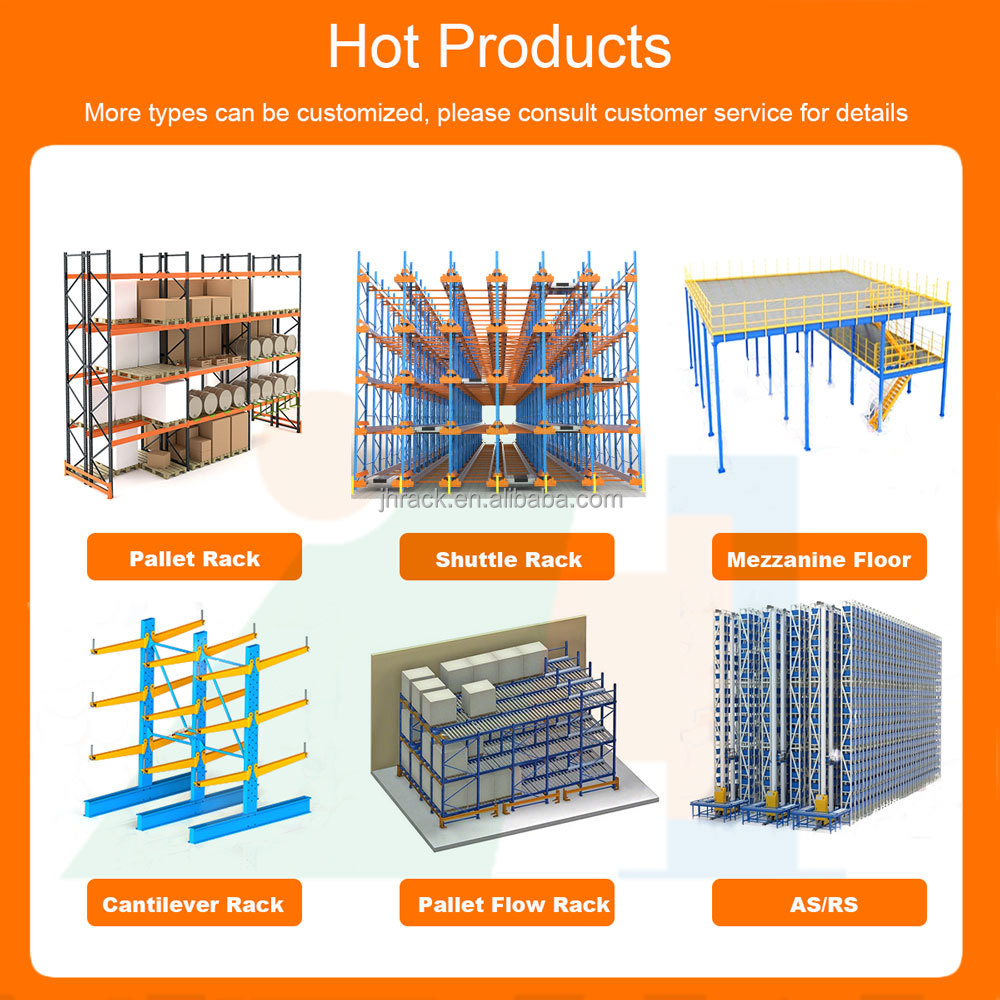
Comprehensive Racking Solutions

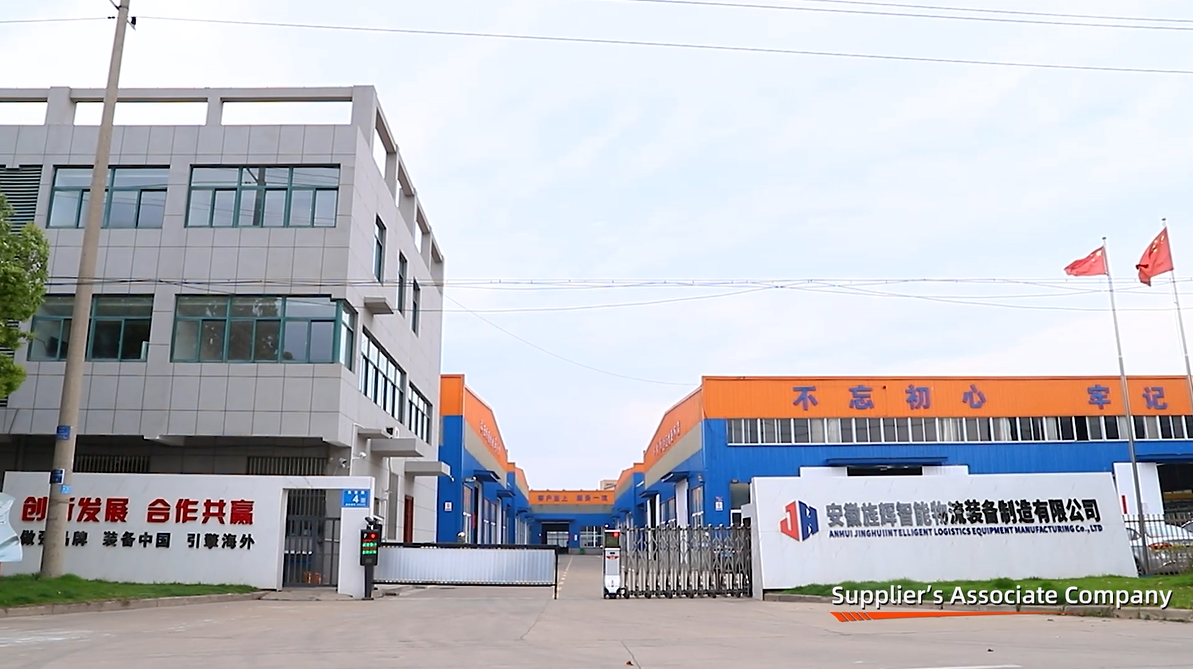
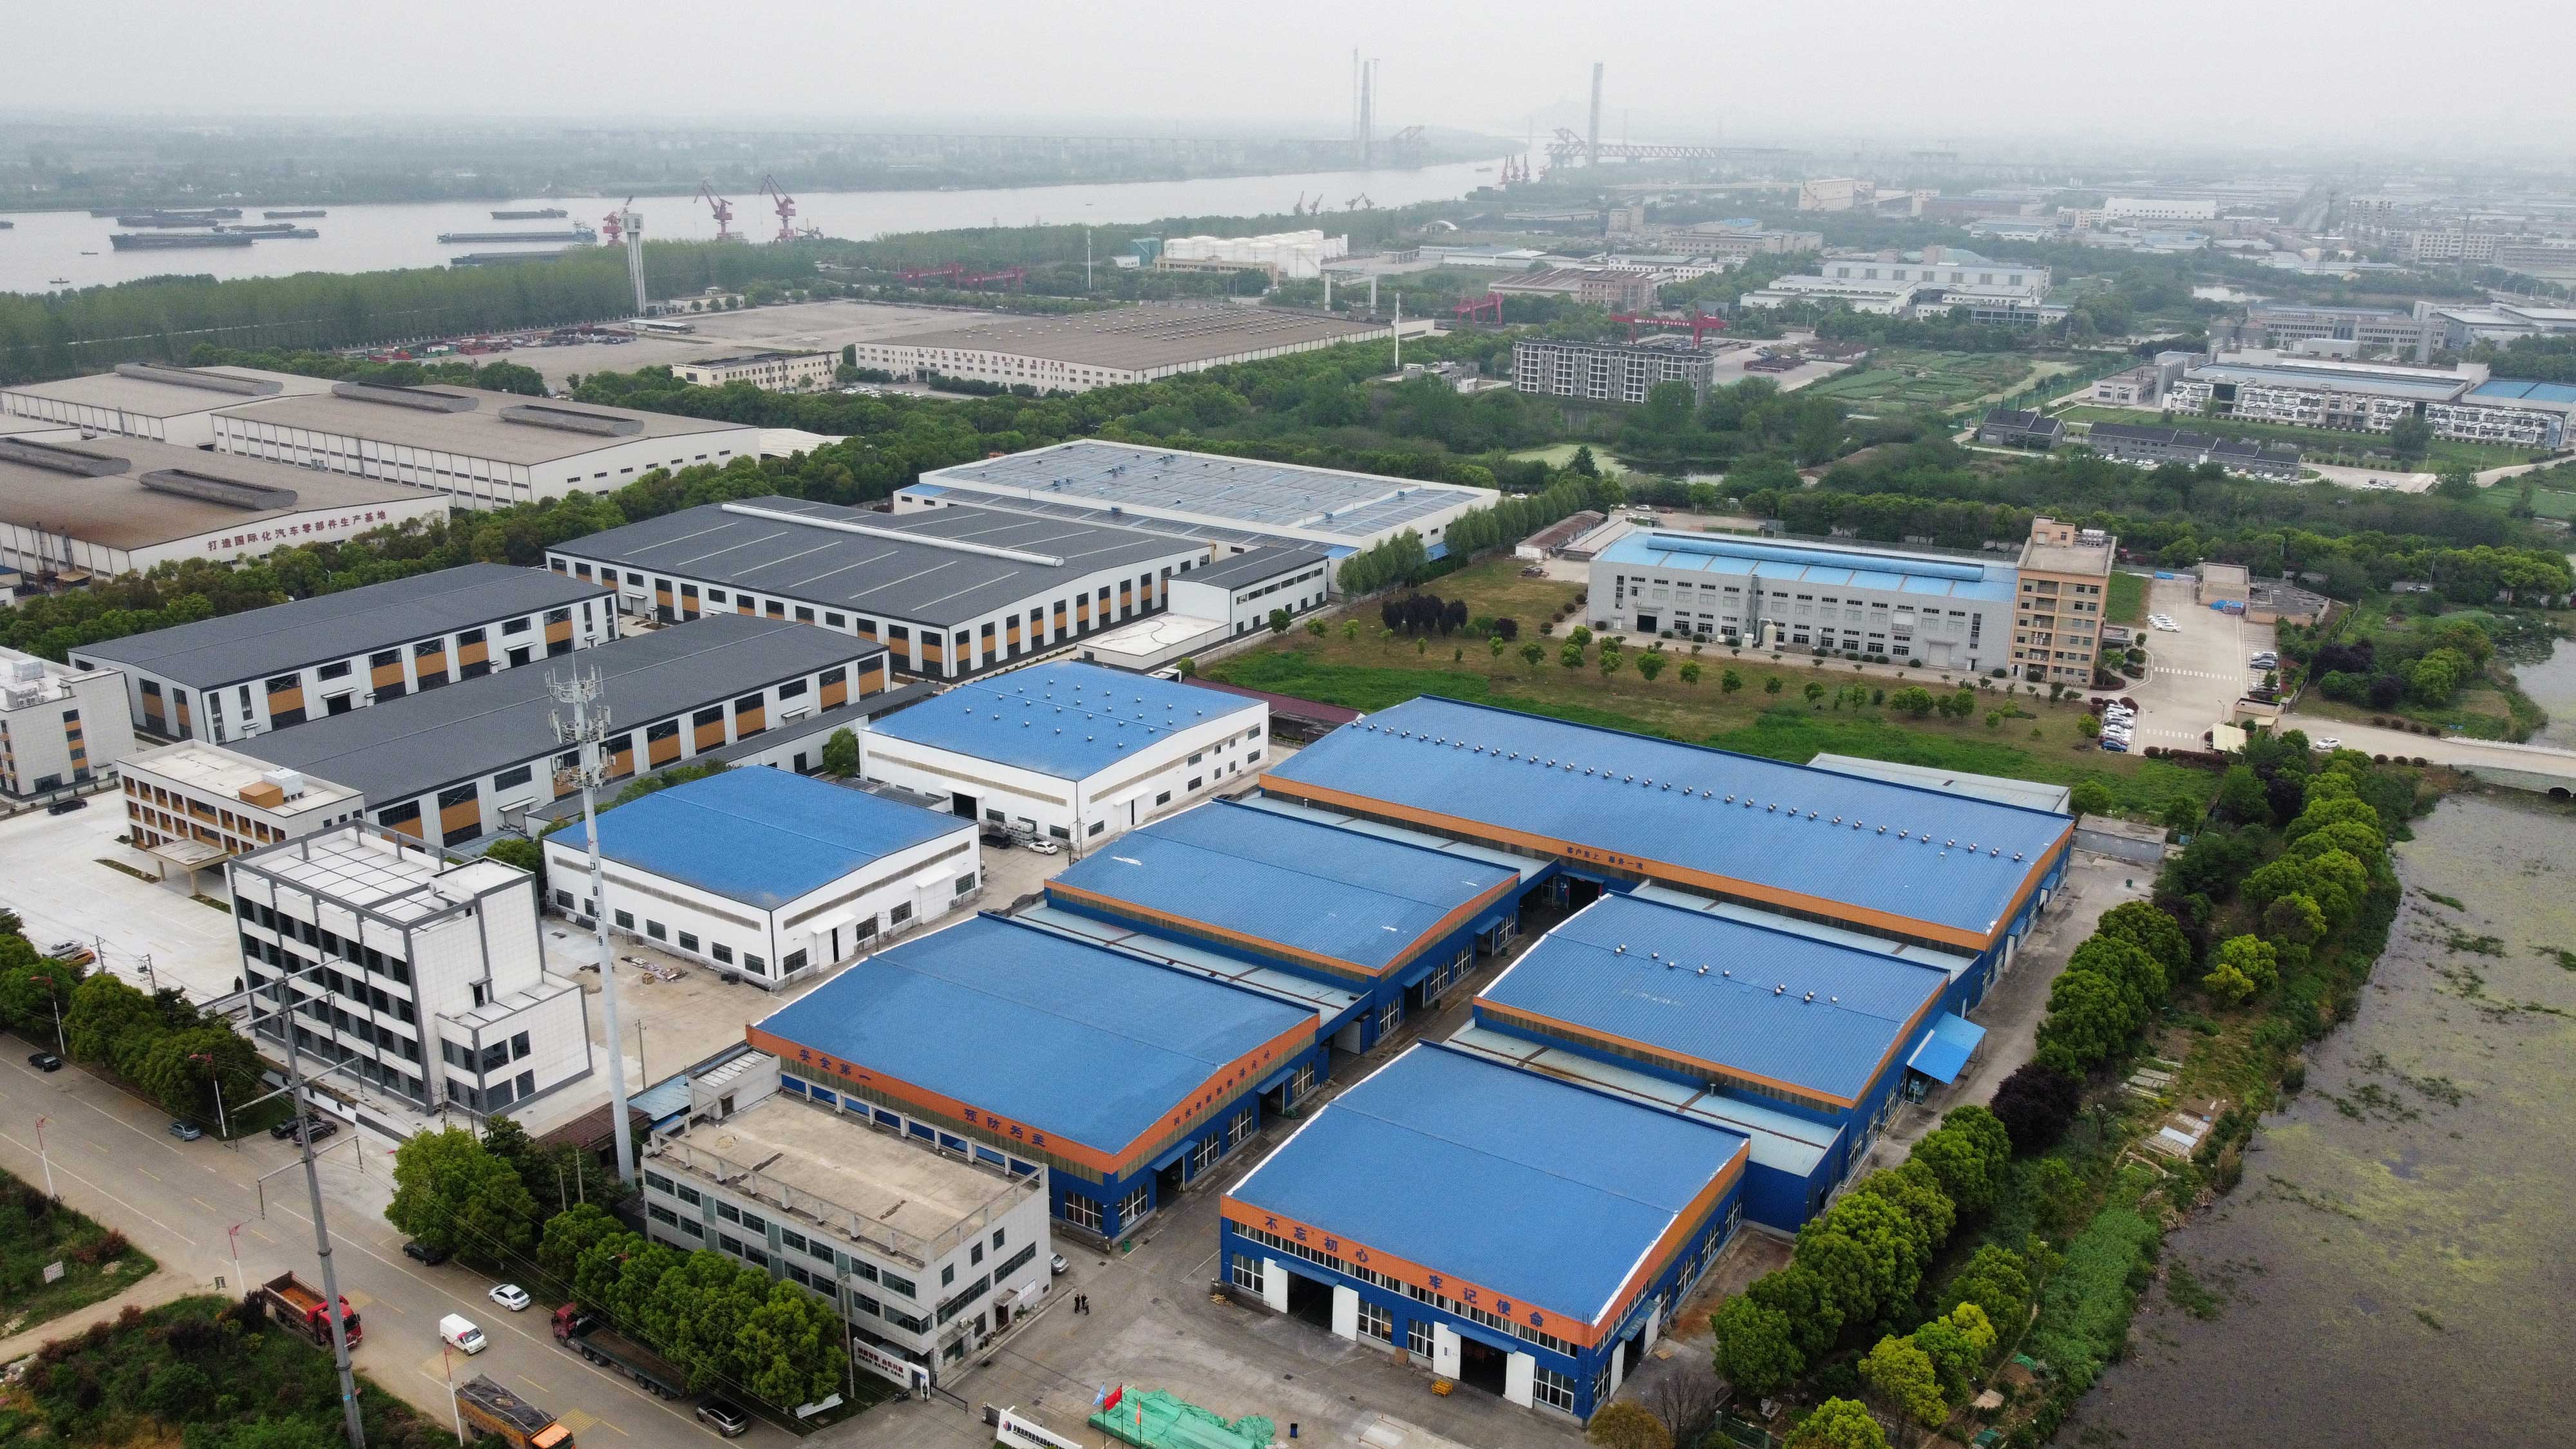
Company Profile

Nanjing Jinhui Storage Equipment Co., Ltd.
Anhui Industrial Park
Anhui Industry Park
Area: 40,000 m²
Employees: More than 50
Nanjing Industrial Park
Nanjing Industry Park
Area: 20,000 m²
Employees: More than 50
Company Profile Video & Facility Overview

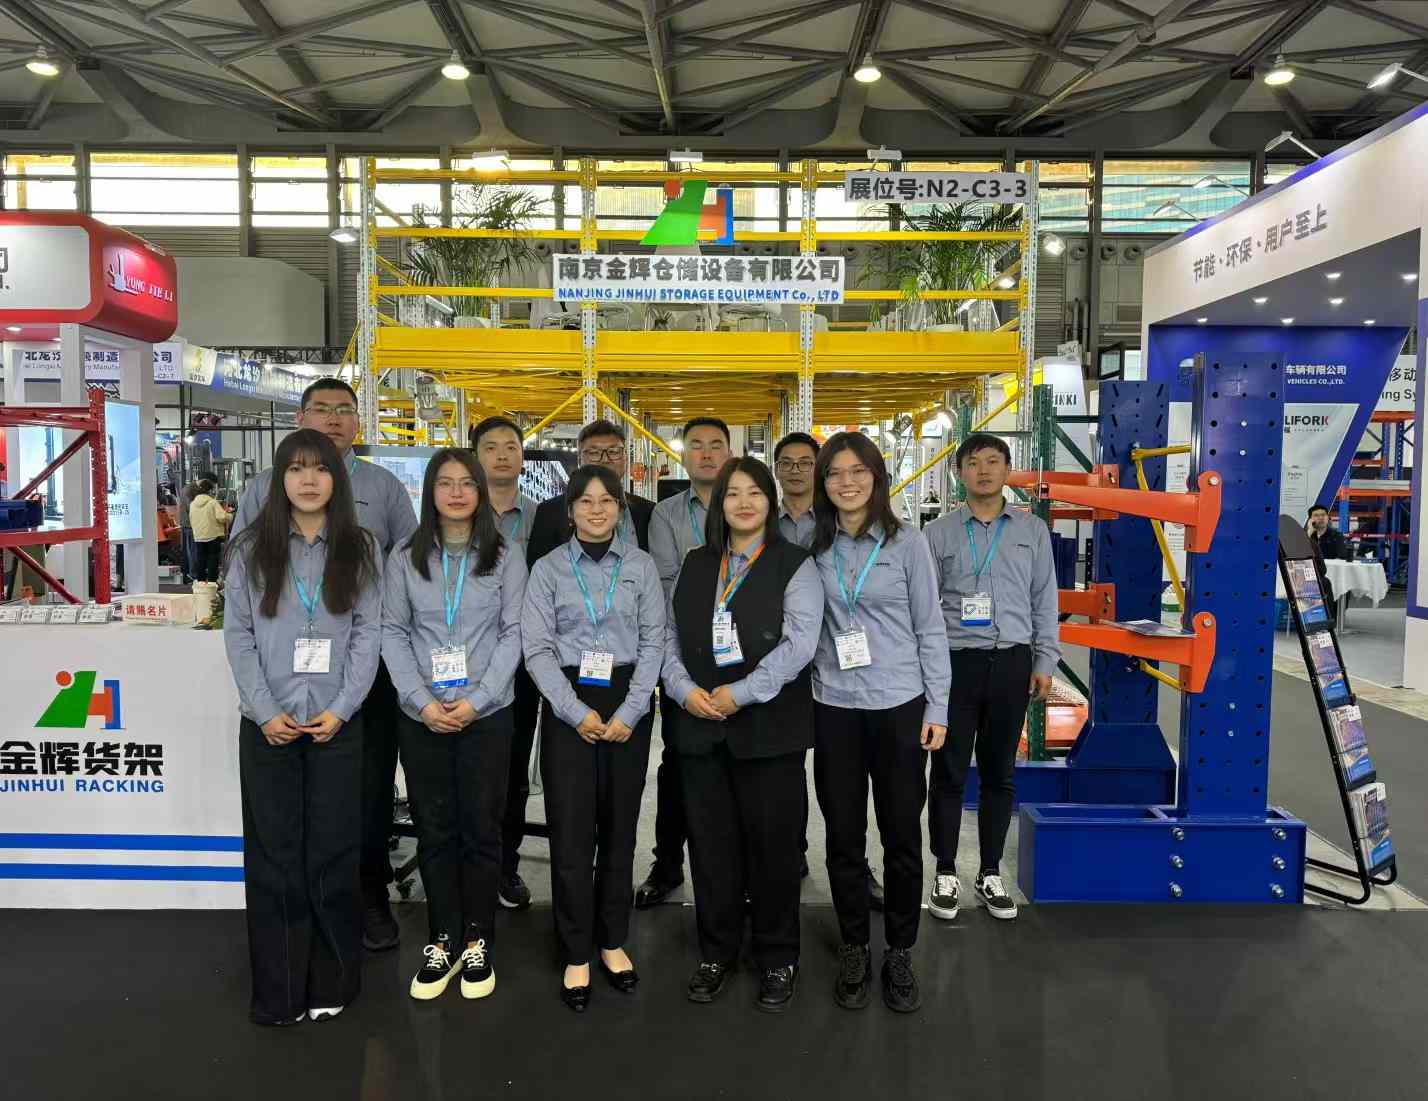
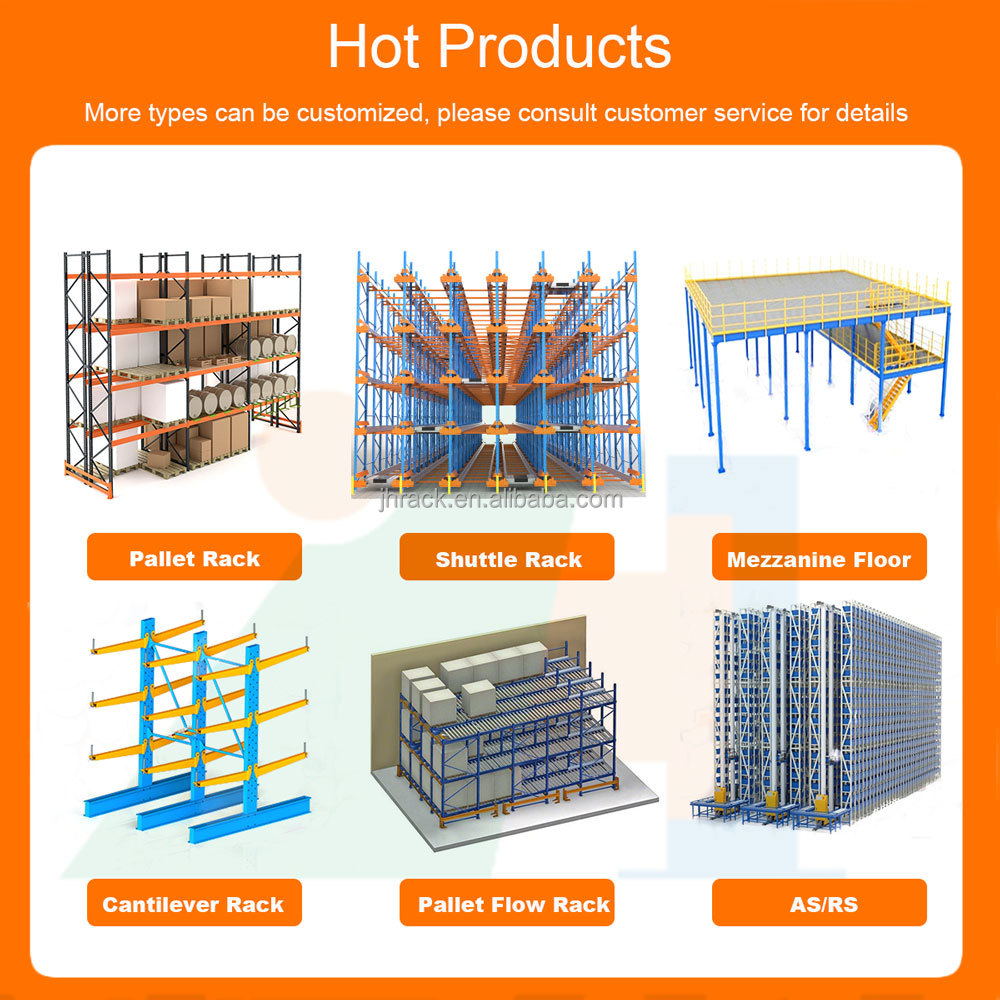
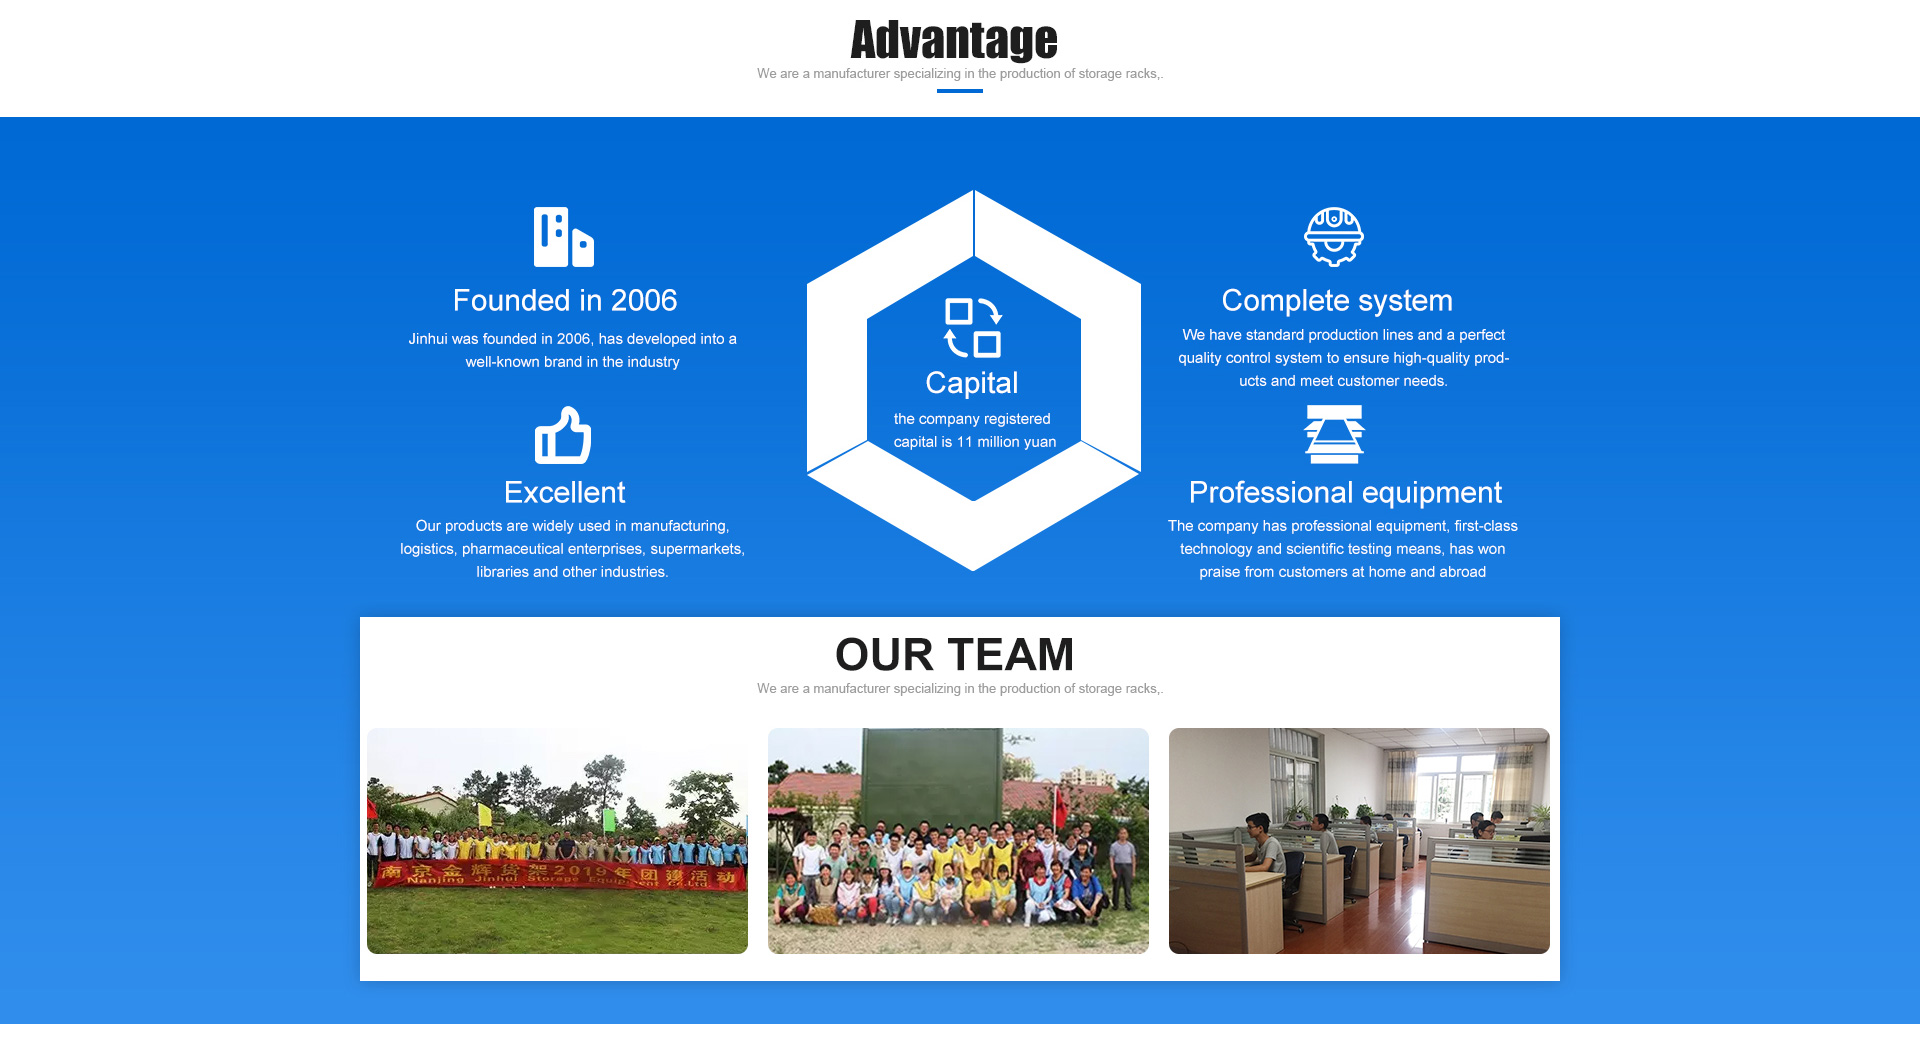
Established in 2006, Nanjing Jinhui Storage Equipment Co., Ltd. specializes in the research, development, sale, and service of pallet racking, mezzanine floors, cantilever racking, light and medium-duty shelving, and steel pallets.

Located in Nanjing with convenient transportation links, we are supported by advanced automated production lines and skilled technicians. Our professional installation and after-sales teams ensure a smooth implementation process. Dedicated to strict quality management and attentive customer service, our staff are always ready to tailor solutions to your storage requirements.

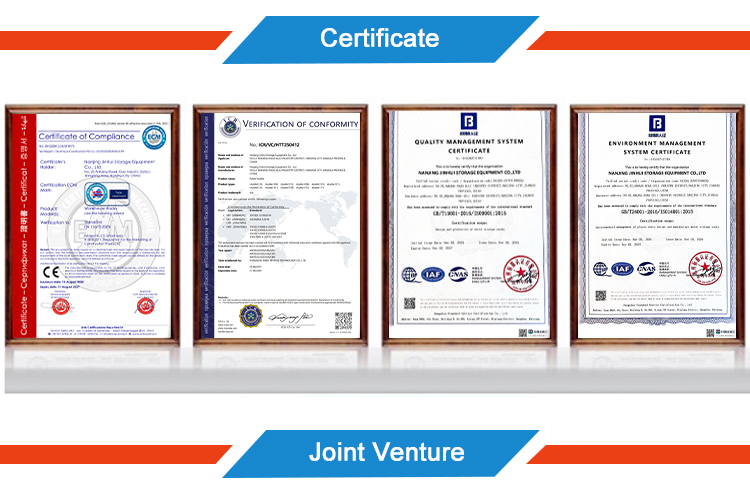
We hold CE, ISO9001, ISO14001, and TUV certificates. Distributed across China, our products are widely exported to Asia, North America, South America, and Africa. OEM and ODM orders are warmly welcomed.
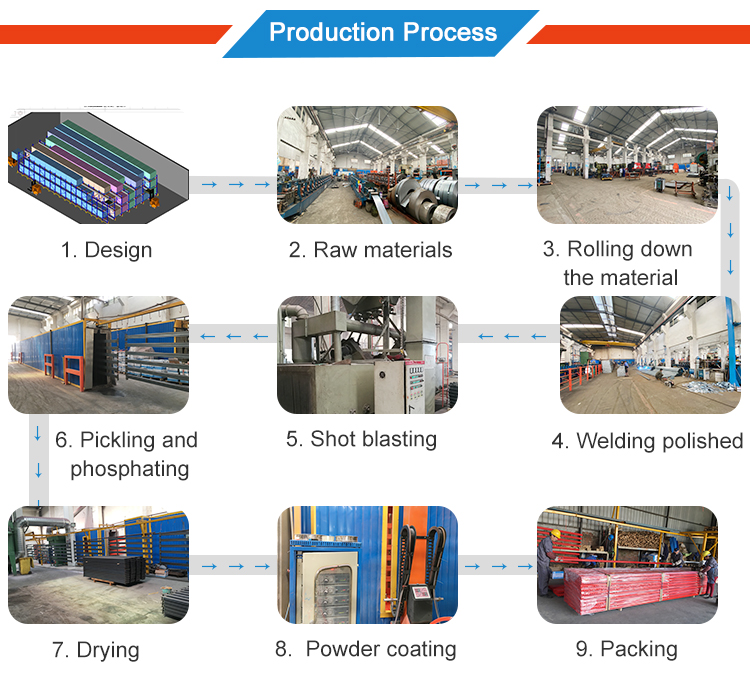
Production Facility
Manufacturing Line
Factory Workshop
Industrial Storage Racks

Packing & Delivery

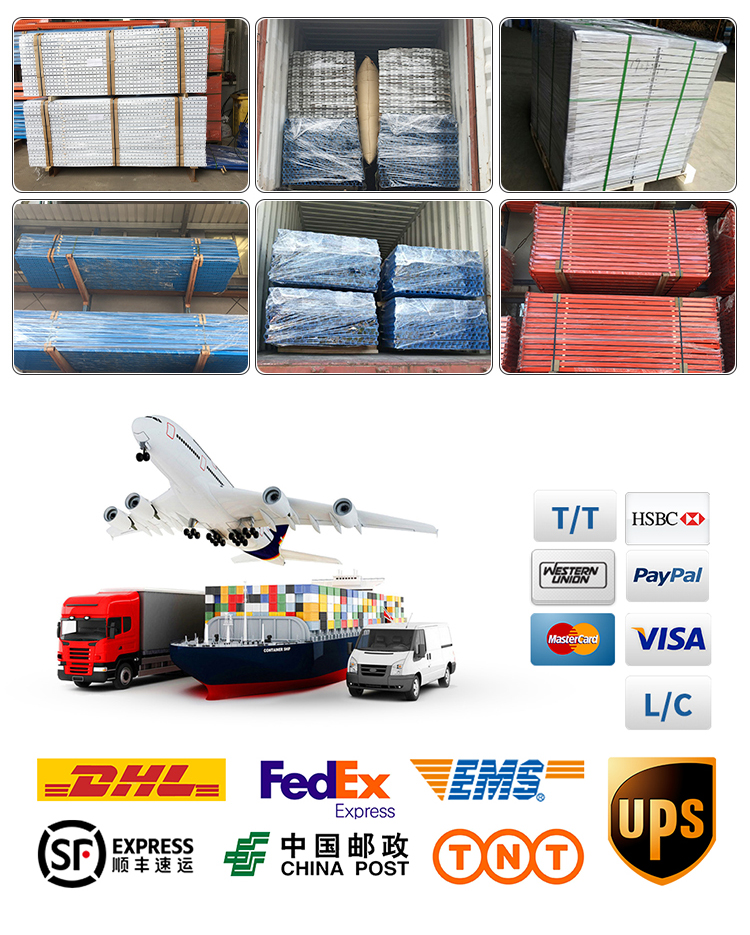
To better ensure the safety of your goods, professional, environmentally friendly, convenient, and efficient packaging services will be provided.
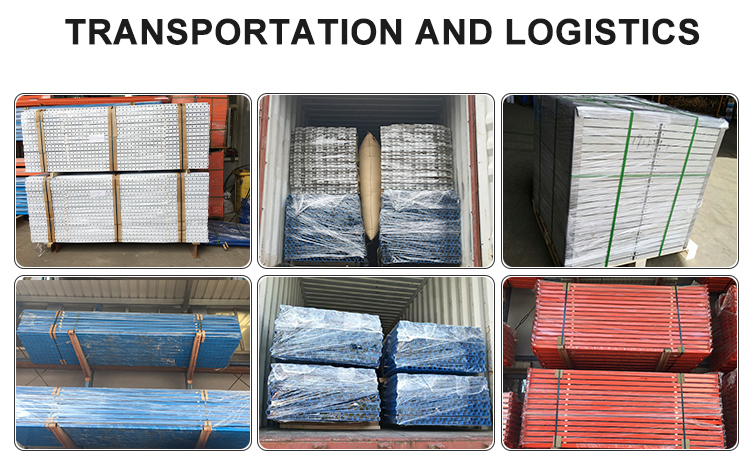
Packing Process
Secure Bundling
Container Loading

Certificate

CE Certificate
ISO Quality Certificate
TUV Certificate

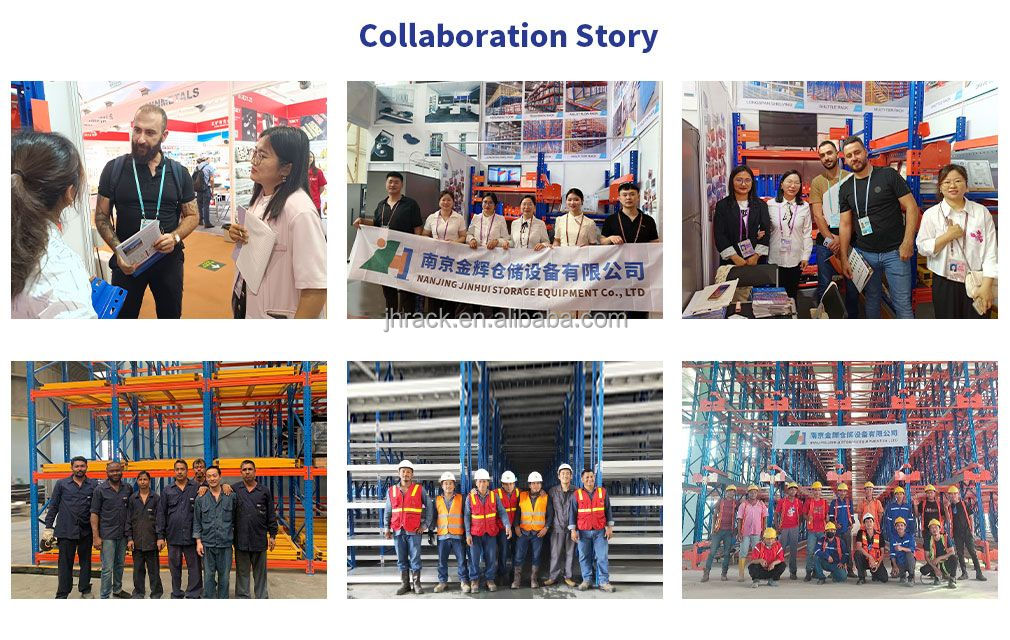
Joint Venture

Joint Venture Project 1
Joint Venture Project 2
Joint Venture Project 3

Frequently Asked Questions (FAQ)

Q1: Are you a factory or a trading company?
A: We are a direct manufacturer specializing in storage racks and intelligent warehouse systems.
Q2: Where is your factory located and how can I visit?
A: Our factory is located in Nanjing City, Jiangsu Province, China. You can fly directly to Nanjing Lukou International Airport, and our team will pick you up. Domestic and overseas clients are warmly invited to visit our facilities.
Q3: What raw material is used for your racking products?
A: We primarily utilize high-grade certified Q235 structural steel to ensure load integrity, seismic safety, and corrosion protection.
Q4: What is your standard packaging method?
A: Standard export packing is used for all orders. Structural parts are bundled with heavy-duty steel strapping and wrapped in protective moisture-resistant plastic stretch film.
Q5: What are your accepted payment terms?
A: We accept (1) T/T wire transfer payments, and (2) Irrevocable L/C at sight.
Q6: What is your estimated delivery time?
A: Delivery schedules depend on the specific project configuration and order quantity, normally ranging between 15 to 30 days upon receiving the official deposit.

Related Products