Technical Whitepaper & Engineering Specification
Aisle Geometry & Volumetric Efficiency: The Definitive Industrial Procurement Matrix
In modern high-throughput intralogistics, selecting an industrial aisle racking system goes far beyond purchasing cold-rolled uprights and load beams. The engineering relationship between horizontal aisle clearance (clear aisle dimension), vertical cube utilization, Material Handling Equipment (MHE) turning radii, and slab load distribution governs long-term operational profitability.
Industrial facility planners are confronted with balancing direct SKU selectivity against maximum cubic pallet density. Understanding exact operational aisle profiles empowers plant managers and distribution engineers to avoid two catastrophic errors: creating aisles too tight for material handling kinematic clearances (resulting in frequent upright collisions), or leaving unnecessary aisle dead-space that wastes costly commercial building footprint.
1. Wide Aisle Selective Systems vs. Very Narrow Aisle (VNA) Architectures
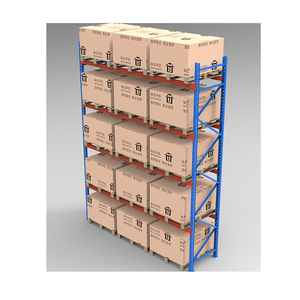
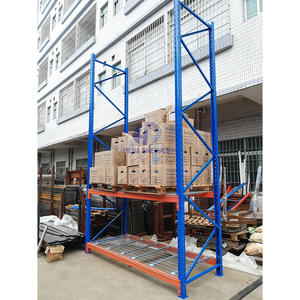
Standard Selective Pallet Racking remains the baseline for universal logistics where 100% immediate access to every pallet position is required. Operating with aisle clearances ranging from 3,000 mm to 3,600 mm, it facilitates the use of standard counterbalance lift trucks without floor-guided steering. While floor footprint utilization typically ranges between 35% and 42%, capital expenditure is minimal, and stock dispatch latency is virtually zero.
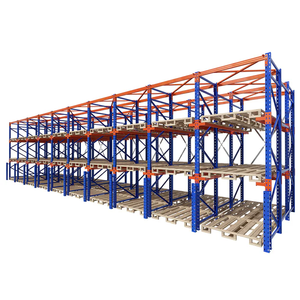
Conversely, Very Narrow Aisle (VNA) systems condense working aisles down to 1,600 mm to 1,850 mm, unlocking up to 55% space recovery while extending storage heights up to 24 meters. However, VNA integration demands stringent structural tolerances: floor slab flatness must comply with DIN 18202 Table 3 Line 4 or TR34 Superflat (FM2/FM1), paired with either physical omega guide rails or inductive buried inductive wire guidance to eliminate rack-frame collision risks during high-mast lift cycles.
| Aisle System Category |
Clear Working Aisle |
Cubic Floor Utilization |
Handling Equipment (MHE) |
Selectivity Profile |
Optimal Inventory Application |
| Wide Aisle Selective |
3,100 – 3,600 mm |
35% – 42% |
Counterbalance / Reach Truck |
100% Direct Selectivity |
FMCG, 3PL Multi-Tenant Hubs, Retail Warehouses |
| Very Narrow Aisle (VNA) |
1,600 – 1,900 mm |
55% – 65% |
Man-Up / Man-Down VNA Turret |
100% Direct Selectivity |
E-Commerce Fulfillment, Pharma Central Hubs |
| Drive-In / Drive-Thru |
Continuous Rail Aisle |
70% – 82% |
Narrow-Chassis Counterbalance |
LIFO / FIFO by Flange Lane |
Cold Storage Freezers, Beverage Bottling, Raw Bulk |
| Radio Shuttle High-Density |
2,800 mm Staging Aisle |
80% – 88% |
Semi-Automated Pallet Carrier |
Programmed LIFO / FIFO |
Seasonal Agricultural Buffers, Blast Chillers |
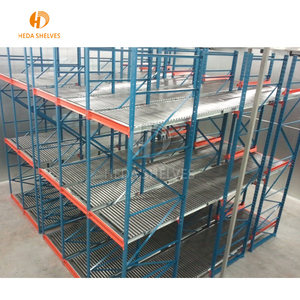
| Gravity Pallet Flow |
Dedicated Charge / Pick Aisles |
75% – 85% |
Standard Mast Forklift |
Strict FIFO Flow |
Perishable Fresh Food, Pharmaceutical Batching |
2. Structural Integrity & Seismic Bracing Considerations
Every industrial aisle installation engineered by HEDA Shelves undergoes rigorous Finite Element Analysis (FEA) calibrated against local site dynamics. Uprights are formed with continuous structural omega profiles featuring multi-bend cold-rolled cross sections that dramatically improve torsional stiffness against horizontal wind and earthquake sway.
For installations in active tectonic zones—such as the Pacific Ring of Fire spanning Central America, Southeast Asia, and Western South America—our structural calculation engineers incorporate seismic response acceleration coefficients according to the local building codes, Eurocode 3 (EN 1993-1-3), and ANSI/RMI MH16.1. Heavy-duty cast base plates, dual chemical anchor embedments, and top-tier horizontal aisle-tie trusses guarantee the rack assembly behaves as a unified, ductile, energy-dissipating framework during emergency cyclic stresses.