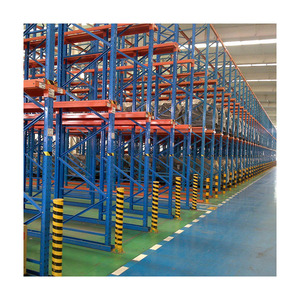
 Heavy Industrial
Mracking Professional Manufacturer Of Drive-In Pallet Racking System Custom Industrial Steel Storage For Warehouses
Custom Uprights
Q235B/Q355B Steel
Epoxy Coated
In modern industrial warehousing, real estate appreciation and energy costs in refrigerated facilities have driven logistics planners toward maximum spatial density. Drive-in pallet racking remains the cornerstone engineering method for high-density homogeneous inventory, eliminating working aisles to yield up to 75%–85% floor cube utilization.
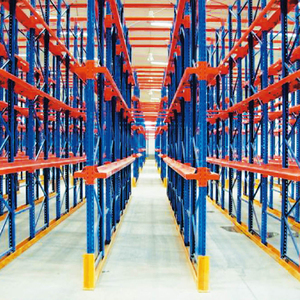
By transforming conventional access aisles into deep storage lanes (up to 12 pallets deep and 5–8 levels high), drive-in systems operate on the First-In, Last-Out (FILO) logic, drastically reducing the required cubic footprint per stored metric ton of stock.
In temperature-controlled environments (-25°C to -18°C), cold air represents direct electrical expenditure. Maximizing storage pallet density directly minimizes the cooled cubic volume per SKU, decreasing kWh power dissipation per stored pallet by up to 35%.
Unlike standard selective racks where crossbeams provide direct transverse rigidity, drive-in systems rely on cantilever brackets, heavy-duty top ties, spine bracing, and anchored guide rails to resist forklift impact dynamics and dynamic seismic torsional forces.
Explore heavy-duty industrial drive-in racks, radio shuttle systems, and gravity flow configurations manufactured with high-tensile cold-rolled steel, custom engineered to international design codes.
Heavy Industrial
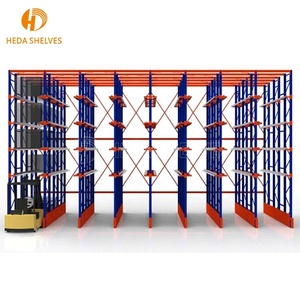 FILO High-Density
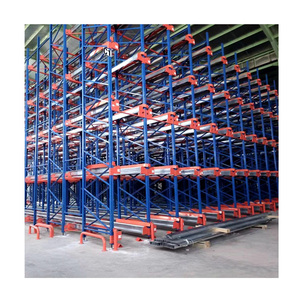 Semi-Automated
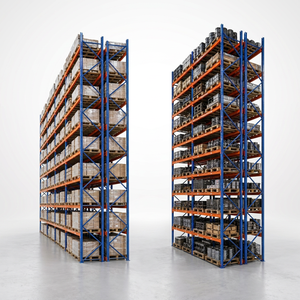 Heavy Duty
 Multi-Tier 5-Layer
 Powder Coated
 High Density
 Dynamic FIFO Flow
A rigorous engineering and procurement comparison across major racking systems suppliers, evaluating steel fabrication standards (EN 15512, RMI, AS 4084), structural engineering depth, customization capabilities, and global export lead times.
| Rank | Manufacturer / Brand | Headquarters | Primary Steel Standard | Engineering Specialization | Direct Customization | Certifications |
|---|---|---|---|---|---|---|
| 01 | HEDA Shelves (Guangzhou Heda Shelves Co., Ltd.) | Guangzhou, China | Q235B / Q355B (EN 10025 equivalent) | Custom Heavy-Duty Drive-In, Seismic Design, Shuttle Retrofit | 100% Factory Direct / OEM / ODM | CE No. 2435-CPR-8605159, ISO 9001:2015, RoHS |
| 02 | SSI Schaefer | Neunkirchen, Germany | European Standard (EN 15512 / FEM 10.2.02) | Large-scale Turnkey High-Bay Automation & Heavy Racking | Project-based Engineering | ISO 9001, ISO 14001, EN 1090 |
| 03 | Mecalux, S.A. | Barcelona, Spain | EN 15512 / RMI Specification | Drive-in systems, Automated Pallet Shuttle Integration | Standardized Modular Systems | ISO 9001, CE, RMI Certified |
| 04 | Dexion (Gonvarri Material Handling) | Castrup, Germany / Spain | EN 15512 / FEM Standards | Cold storage drive-in configurations & industrial racks | Regional Dealer Networks | ISO 9001, ISO 45001, CE |
| 05 | Frazier Industrial Company | Long Valley, NJ, USA | AISC / RMI MH16.1 Standards | Structural Steel (Hot-rolled channels) Drive-In Racks | Engineered Build-to-Suit | RMI Certified, AISC Quality Certified |
| 06 | Stow Group (Averys) | Dottignies, Belgium | EN 15512 / Eurocode 3 | Drive-in, Drive-through, and 2D Shuttle Racks | Engineering Partner Integration | ISO 9001, ISO 14001, CE |
| 07 | Interlake Mecalux | Melrose Park, IL, USA | ANSI MH16.1 / RMI | North American Drive-in Rack & Push-Back configurations | Configured Catalog Production | RMI, ISO 9001 |
| 08 | BITO-Lagertechnik Bittmann GmbH | Meisenheim, Germany | EN 15512 / FEM 10.2.07 | Food sector drive-in solutions with continuous cantilever arms | Modular Catalog Orders | ISO 9001, RAL-RG 614 |
| 09 | Daifuku Co., Ltd. | Osaka, Japan | JIS G 3101 / Structural Codes | Automated Material Handling with Static High-Density Bays | Large-scale System Integration | ISO 9001, ISO 14001 |
| 10 | Jungheinrich AG | Hamburg, Germany | EN 15512 / FEM Standards | Integrated forklift & drive-in storage racking environments | Fleet & Rack Bundled Contracts | ISO 9001, CE Mark |
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a massive 30,000 m² automated production facility capable of generating 30,000 tons of structural cold-rolled steel racking monthly. With 25+ years of engineering experience and over 10,000 completed warehouse installations across 120+ countries, HEDA offers end-to-end direct manufacturing with comprehensive 3D CAD modeling, custom seismic engineering calculations, and factory-direct export pricing.
A global leader in fully automated intralogistics and heavy modular racking. SSI Schaefer’s drive-in systems are built to European FEM and EN norms, featuring highly engineered tapered pallet lead-in rails and integrated safety components suited for mega-distribution hubs.
Mecalux provides high-density drive-in and drive-through configurations backed by advanced WMS software integration. Their systems are widely recognized in European and Latin American logistics networks for standardized roll-formed upright designs.
Unlike roll-formed manufacturers, Frazier specializes in heavy structural hot-rolled structural steel channels. Their drive-in racks offer immense impact durability against forklift collisions in harsh, high-abuse cold storage applications.
Stow is a major European producer specializing in high-density pallet racking and automated shuttle systems (Stow Atlas). Their drive-in engineering emphasizes optimized steel profiles that maximize strength while reducing total structure self-weight.
A historic brand in modern storage shelving, Dexion offers drive-in solutions with robust top-tie assemblies and specialized arm brackets designed to absorb operational vibratory stresses in temperature-controlled facilities.
Drive-in racks lack conventional front-to-back load beams across the entry lane. Understanding the structural dynamics, load transfer mechanisms, and horizontal deflection criteria is paramount to preventing structural fatigue or progressive collapse.
Pallets rest continuously on horizontal pallet rails supported by cantilever brackets bolted or welded to the vertical uprights. Because vertical loads act eccentrically to the upright's longitudinal neutral axis, substantial torsional moments are introduced. Engineering calculations must account for local buckling across the upright web perforation slots using finite-element analysis (FEA) per EN 15512 standards.
Without lateral crossbeams, drive-in systems rely on rigid horizontal top bracing (horizontal portal trusses) and rear vertical spine cross-bracing. In seismic regions (such as the Pacific Rim and active fault belts), dynamic base accelerations must be transferred directly from the upper tiers to anchored vertical portal columns and oversized base plates embedded into minimum 250mm reinforced concrete slabs.
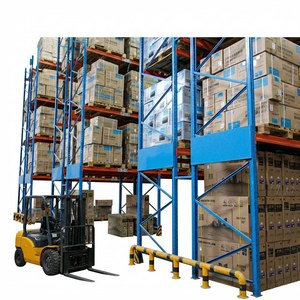
Because counterbalanced or reach forklifts must drive directly inside the storage bays, the risk of mast and chassis collisions against vertical uprights is exponentially higher than in selective racking. Professional engineering specifications require continuous heavy-gauge structural angle guide rails (e.g., L100x75x6mm or structural C-channels) bolted directly to the slab with reinforced bull-nose column entry guards.
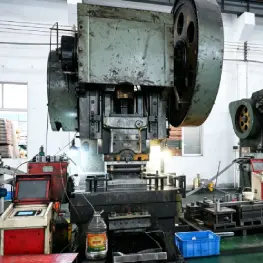
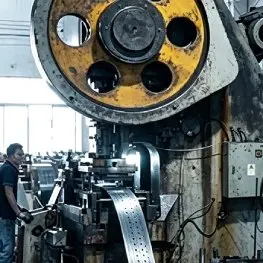
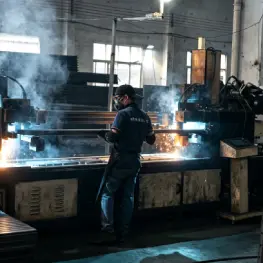
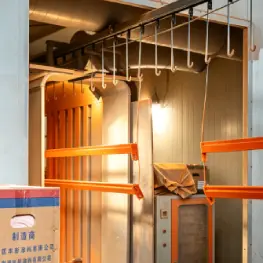
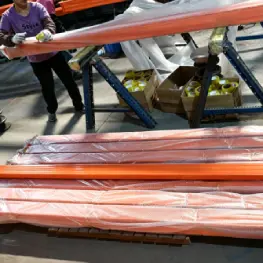
Every structural component passes through a rigorous, automated ten-stage fabrication protocol to ensure zero dimensional deviation, high metallurgical yield strength, and robust corrosion prevention.
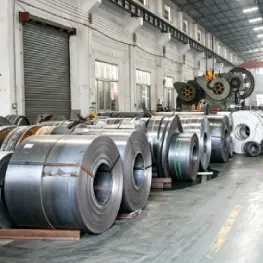
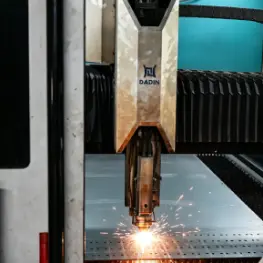
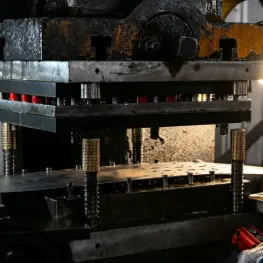
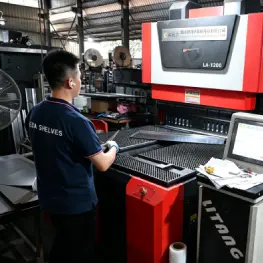
Industrial procurement is shifting from standalone static steel structures to hybrid systems engineered for automated retrofits, dynamic seismic resilience, and digitized lifecycle maintenance.
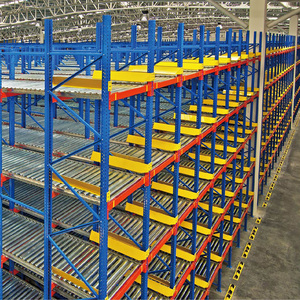
Traditional drive-in systems require forklift drivers to enter storage bays, introducing travel time bottlenecks and collision risks. Modern warehouses are procuring drive-in structures pre-drilled to convert into semi-automated Radio Shuttle systems. In shuttle retrofits, high-speed autonomous carts navigate deep channels, accelerating loading cycles by over 60% while protecting structural uprights from forklift interaction.
With global logistics real estate expanding along active seismic belts in North America, Central America (Guatemala, Costa Rica, Panama), and the Mediterranean, procurement managers now demand site-specific structural verification. Suppliers must furnish PE-stamped or third-party verified finite element calculations factoring in ground acceleration spectral coordinates (Ss and S1), requiring heavier base plates and high-ductility anchor rods.
Global cold-chain expansions (dairy, seafood, agro-export, pharmaceuticals) demand prolonged resistance to thermal condensation and chemical washing agents. Traditional single-layer paint finishes face rapid delamination. Racking buyers increasingly specify double-layer zinc-phosphated epoxy powder systems or continuous hot-dip galvanizing (HDG per ISO 1461) to guarantee 20+ year rust-free operational lifespans in sub-zero freezers.
In-depth technical answers addressing load limits, structural clearances, forklift compatibility, and floor slab requirements for warehouse project managers and procurement directors.
Submit your warehouse building dimensions (CAD or PDF), pallet footprints, and forklift specifications. HEDA Shelves' professional structural engineering team will prepare a comprehensive 2D floor plan, 3D spatial layout, and structural load calculation proposal within 24 hours.