Precision Dynamic Storage & Industrial Racking Systems
Manufactured under ISO 9001:2015 and CE standards utilizing high-tensile Q235B structural steel, optimized for seamless integration with carton gravity rollers and conveyor hubs.
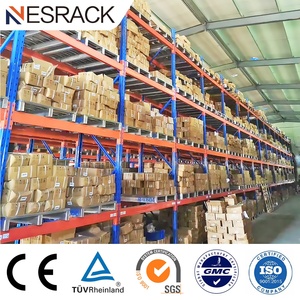
Heavy-Duty Boltless Shelving System
CE-certified modular shelving engineered for fast assembly, easily converted to hand-loaded carton feed lanes with adjustable tier pitches.
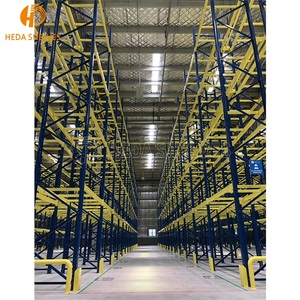
4-Layer Medium Duty Industrial Shelving
High-integrity phosphatized steel construction providing 100–300 kg shelf capacity, perfectly scaled for high-frequency split-case replenishment.
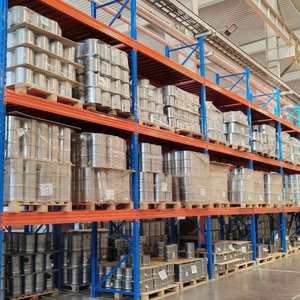
Selective Pallet Racking with Drop-in Beams
Industrial selective framework designed to host heavy pallet storage above, while bottom levels house dynamic carton flow bed systems.
Q235B Teardrop Adjustable Pallet Rack
Standardized teardrop configuration with 50mm pitch adjustability, compatible with North and Central American standard roller track assemblies.
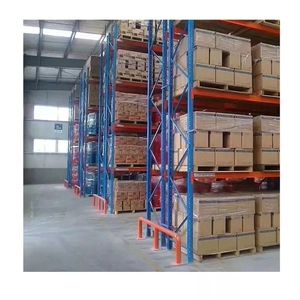
Heavy Duty Stacking Storage Metal Racking
Rigid vertical load columns designed for flexible warehouse setups, providing high torsional rigidity under continuous roller vibration.
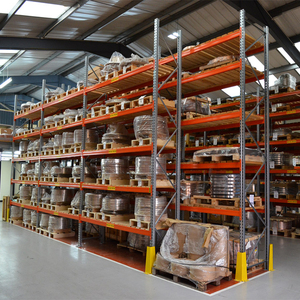
High SKU Selective Pallet Rack with ESD Finish
Specially coated with electrostatic dissipative powder, making this structure optimal for electronics, medical carton flow, and cleanrooms.
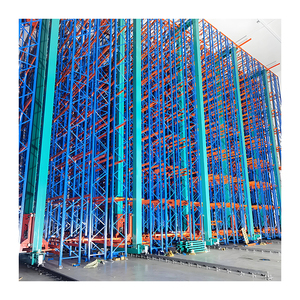
High-Density Automated Shuttle Storage System
3000kg load capacity automatic steel framework engineered for pallet buffering that feeds integrated gravity carton picking tunnels below.
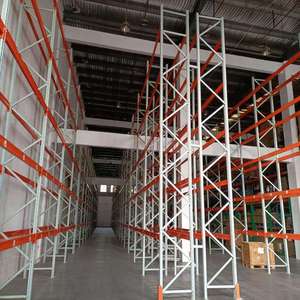
Heavy-Duty 4-Layer Tall Storage Rack
Dual-color powder-coated uprights and high-visibility safety beams built for multi-tiered picking mezzanines and deep flow track integration.
Engineering Audit: Selecting Top Carton Flow Rack Manufacturers
A technical guide evaluating structural integrity, roller physics, factory certification, and export stability for logistics infrastructure projects.
1. Steel Grade Verification
Certified Q235B or Q355 cold-rolled carbon steel ensuring uniform yield strength (≥ 235 MPa) under sustained static and rolling kinetic stress.
2. Dynamic Roller Physics
Precision-molded high-density polyethylene (HDPE) or steel skate wheels mounted on cold-formed galvanized or aluminum alloy tracks.
3. Certified QC Regimes
Accredited CE mark (EN 15512:2020) and ISO 9001:2015 quality management with continuous dimensional laser inspection during punching.
4. In-House Surface Finish
10-stage automated pre-treatment featuring chemical degreasing, acid pickling, phosphating, and electrostatic epoxy-polyester powder baking.
5. Seismic Resilience
FEA-modeled column uprights and customized baseplate anchor spacing designed according to IBC and Eurocode 8 seismic zoning factors.
6. Track Pitch Flexibility
Drop-in roller tracks with tool-free lane dividers adjustable on 10mm to 25mm lateral increments to instantly adapt to varying package widths.
7. Ergonomic Pick Shelves
Integrated tilt trays positioned at 5° to 15° presentation angles at the discharge face to minimize picker wrist and lumbar torque.
8. Monthly Scale & Capacity
Tier-1 factories possessing 30,000+ m² production workshops capable of outputting > 25,000 tons monthly for synchronized container shipments.
9. Export Packaging Rigor
Heavy-duty strapping, foam interlayers, and custom steel stillages preventing transit deflection during 40-foot HQ maritime container transport.
10. Full BIM & CAD Support
Dedicated design teams offering free 24-hour structural layout drawings, isometric 3D views, and discrete lane velocity simulations.
Key Information Gain for Engineering Evaluators
A carton flow system is not merely static racking fitted with plastic wheels. It is a precision dynamic conveyor bed. When tote bins or corrugated paper cartons enter a lane, velocity must be self-regulating. High-grade suppliers utilize controlled gradient drop (typically 2.5% to 4.5% based on container weight) alongside optional centrifugal speed controllers for runs exceeding 4 meters. Selecting a tier-one factory guarantees roller concentricity and minimizes rolling resistance, eliminating costly carton stalls or box crush collisions.
Carton Flow Engineering Parameters & Load Tolerances
Standard architectural parameters for heavy-duty industrial carton live storage systems manufactured by certified export facilities.
| System Component | Material Specification | Standard Dimension / Capacity | Functional Advantage |
|---|---|---|---|
| Upright Columns | Q235B Cold-formed steel (50mm/75mm hole pitch) | 80×60mm to 100×70mm, 1.8–2.5mm thickness | High torsional stability; accepts multi-tier mezzanine loads. |
| Load Beams | Interlocking step beam or structural box beam | 80×50mm to 120×50mm, span up to 2700mm | Direct drop-in track support without bolted beam brackets. |
| Roller Tracks (Bed) | High-strength extruded aluminum or galvanized C-channel | Wheel pitch: 28mm, 35mm, 50mm, 70mm | Zero deflection under concentrated point loads up to 250 kg/m². |
| Rollers & Wheels | Engineered HDPE, Polypropylene, or Steel Bearings | Ø 28mm to Ø 38mm; 15–25 kg per roller | Impact resistant, silent rolling (< 58 dB), broad temperature range (-25°C to +40°C). |
| Lane Dividers | Cold-rolled steel sheet with powder-coated finish | Heights: 60mm, 100mm; tool-free clip adjustment | Maintains straight tracking paths; eliminates carton pinching and skewing. |
| Loading / Pick Trays | Formed steel with smooth folded safety lips | Tilt presentation: 0° to 18°; load capacity 150 kg | Enables rapid split-case SKU visualization and ergonomic hand picking. |
Emerging Technologies Shaping Carton Flow Systems (2025–2035)
Strategic purchasing insights for operations executives planning next-generation automated distribution centers.
Pick-to-Light (PTL) Native Integration
Future procurement demands carton flow tracks equipped with snap-on bus channels and digital display brackets. Modern factories now punch beams with pre-indexed conduits to host pick-to-light sensors, dynamic e-ink labeling, and optical pick confirmation modules without manual drilling.
AMR & Cobot Hybrid Interfaces
Autonomous Mobile Robots (AMRs) increasingly service carton flow discharge faces. Future systems incorporate mechanical dampening stops, optical reflectors, and docking precision brackets that allow robotic gripping arms to pick directly from flow lanes with sub-millimeter repeatable accuracy.
Zero-VOC & Low-Carbon Steel Supply
Corporate ESG procurement dictates strict carbon lifecycle reporting. Leading manufacturers have upgraded to heavy-metal-free zirconium conversion pre-treatments, closed-loop powder reclamation exceeding 98% efficiency, and high-efficiency induction curing ovens powered by renewable solar arrays.
Universal Drop-In Bed Retrofits
Supply chain elasticity requires converting existing selective pallet racks into dynamic picking tunnels within hours. Next-generation universal carton flow beds use spring-loaded hanger clips that seat instantly into teardrop, diamond, or keyhole upright slots without requiring beam alterations.
IoT Sensor-Embedded Roller Beds
Predictive maintenance sensors embedded in gravity tracks detect inventory depletion, lane blockages, and bearing friction anomalies in real-time. This dynamic telemetry triggers automated replenishment alerts via warehouse management systems (WMS) before picker stockouts occur.
Anti-Microbial & Cold-Chain Formulations
For pharmaceutical and perishables fulfillment, roller wheels now incorporate food-grade, anti-static, and anti-microbial additives that inhibit bacterial biofilm growth while functioning smoothly down to blast-freezer conditions (-30°C) without plastic embrittlement.
Why International Enterprise Buyers Choose HEDA Shelves
Guangzhou Heda Shelves Co., Ltd. delivers single-source accountability from raw steel coil processing to international port logistics.
10-Stage Controlled Manufacturing Cycle
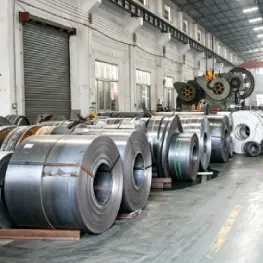
Raw Material QC
Spectrometric testing of premium Q235B cold-rolled steel coils.
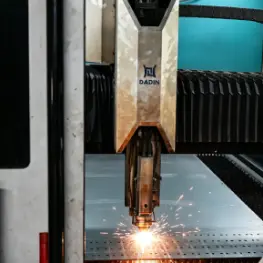
Precision Slitting
CNC decoiling and high-speed longitudinal slitting lines.
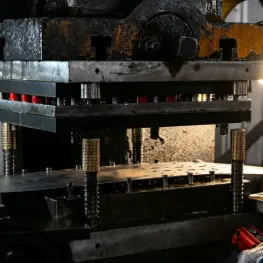
Auto Punching
Continuous hydraulic stamping ensuring +/-0.1mm pitch accuracy.
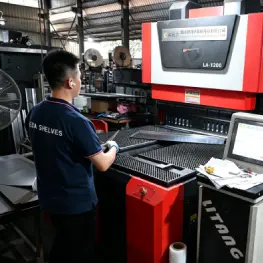
Cold Roll Forming
Multi-station automated roller forming for maximum stiffness.
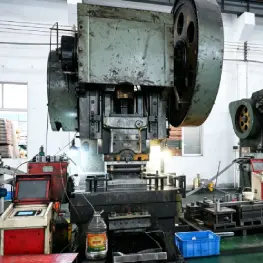
Profile Sizing
Automatic laser cut-off to required project clear heights.
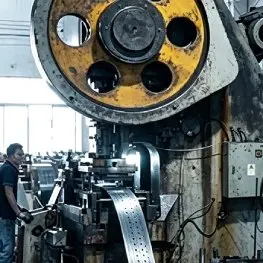
Weld Prep Polish
Mechanical deburring and weld seam edge prep polishing.
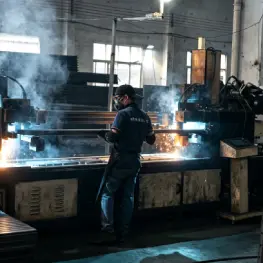
Robotic Welding
Shielded dual-wire robotic MIG welding for connectors.
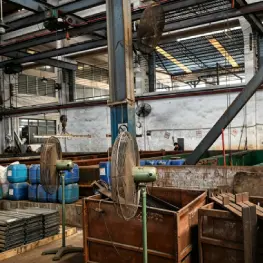
Acid Pickling
Full chemical immersion to remove mill scale and inhibit rust.
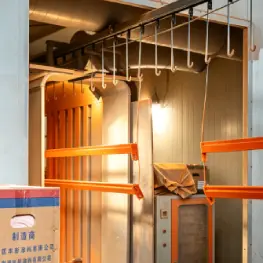
Powder Coating
60–80 micron electrostatic epoxy cure at 200°C.
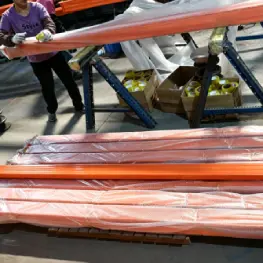
Export Packing
Palletized banding, corner protection, and container stowage.
Verified Regulatory Certifications
Fully compliant with international engineering covenants, verified for customs clearance and insurer validation.
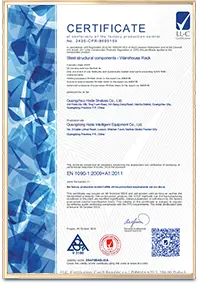 CE Certified
No. 2435-CPR-8605159
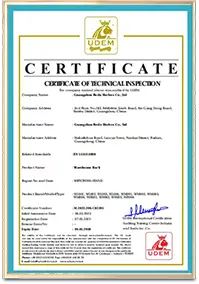 ISO 9001:2015
No. 18624Q00169R0M (Audit: 2027)
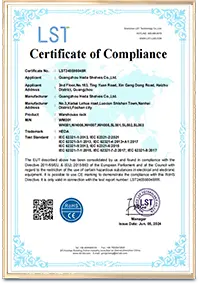 RoHS Compliant
Zero Hazardous Substances
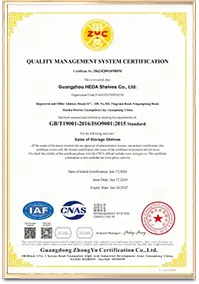 SGS / TÜV Audited
Structural Load & Yield Tested
Frequently Asked Questions: Carton Flow Racking Procurement
Comprehensive answers addressing slope calculations, carton weight capacities, maintenance intervals, and container shipping.
Ready to Engineer Your High-Velocity Carton Flow System?
Partner directly with Guangzhou Heda Shelves Co., Ltd.—over 25 years of manufacturing excellence, CE & ISO 9001 certified, exporting factory-direct to over 120 countries worldwide. Receive your free CAD layout and itemized FOB/CIF quotation within 24 hours.