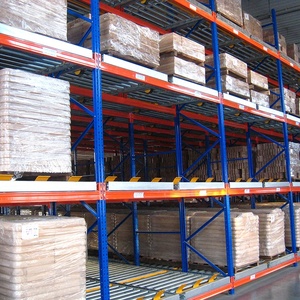
 Gravity Flow
CE Certified Heavy Duty Pallet Flow Rack System
Gravity-driven inclined roller lane system featuring dynamic centrifugal speed controllers and automatic end separators for 100% strict First-In First-Out operations.
Engineered for mission-critical logistics, perishables management, cold chains, and automated multi-tier warehouses requiring zero stock obsolescence.
Gravity Flow
Gravity-driven inclined roller lane system featuring dynamic centrifugal speed controllers and automatic end separators for 100% strict First-In First-Out operations.
 Semi-Autonomous
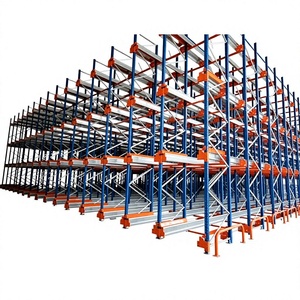
Intelligent radio shuttle platform designed for high-throughput fulfillment channels. Supports flexible FIFO / LIFO switching without requiring forklifts inside storage bays.
 ASRS Multi-Direction
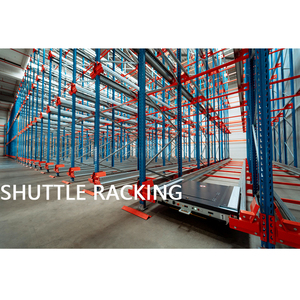
Cross-directional multi-tier matrix shuttle network optimized for deep lane storage, high-density buffers, and integrated vertical lifters with automated dispatch control.
 Heavy-Duty ASRS
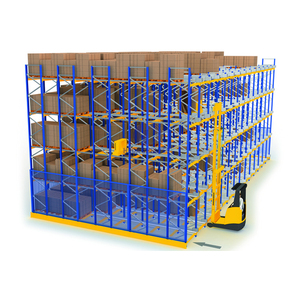
Rugged high-load profile engineered for structural durability in extreme environments. Built-in obstacle avoidance, rapid battery hot-swaps, and automated lane shifting.
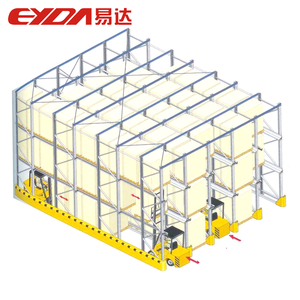 Drive-Thru Dual Access
Continuous aisle-free design configured as a Drive-Thru setup for FIFO batch handling. Loading on one face, picking on opposite face for high-density storage utilization.
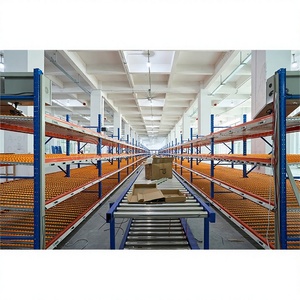 Dynamic Roller Lane
Galvanized full-width steel rollers with integrated safety braking mechanisms for heavy industrial logistics, beverage operations, and pharmaceutical central warehouses.
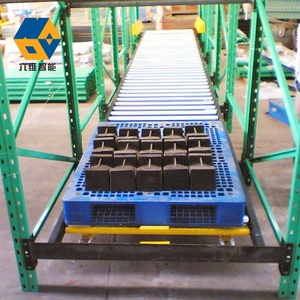 Modular Industrial
Multi-lane dynamic FIFO pallet configuration with quick-drop dampening guides, adjustable entry lead-ins, and floor-anchored high-impact structural column guard protectors.
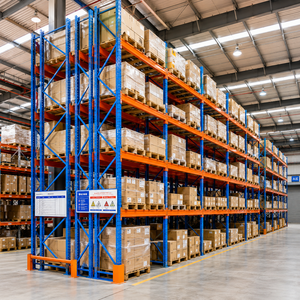 High Load Selective
Q235B cold-rolled structural steel shelving with epoxy powder anti-rust treatment. Ideal staging buffer system, intermediate storage floor, and multi-tier picking deck.
A technical guide for warehouse managers, systems integrators, and procurement directors on selecting, dimensioning, and commissioning high-density FIFO racking installations.
Operates entirely through gravitational kinematics. Lanes sit on an inclined angle (normally 3.0% to 3.5% grade). Pallets are deposited into the charge end, travel smoothly along controlled brake rollers, and decelerate against structural end stops. This eliminates intermediate forklift traffic aisles, isolating loading lanes from picking bays.
Combines deep continuous structural channels with intelligent autonomous robotic shuttles. In true FIFO configurations, access requires open charge aisles and separate discharge aisles. The shuttle drives beneath pallets, hoists cargo using hydraulic/electric ball-screws, and deposits it at the output edge via optical sensors.
Configured with continuous drive-through corridors, allowing material handlers to enter one side of the bay block to replenish pallets and enter the opposing side for retrieval. This creates true batch FIFO operations at a fraction of automated system costs, best suited for uniform pallet dimensions and batch production runs.
| Evaluation Parameter | Gravity Pallet Flow | Radio Shuttle FIFO | Drive-Thru Racking | ASRS 4-Way Shuttle |
|---|---|---|---|---|
| Stock Rotation Fidelity | 100% Strict Continuous FIFO | Software-Managed Batch FIFO | Batch / Campaign FIFO | 100% Automated Matrix FIFO |
| Volumetric Footprint Efficiency | Extremely High (Up to 80%) | Maximum Dense (Up to 85%) | High (Up to 75%) | Maximum Footprint (Up to 90%) |
| Forklift Aisles Required | Only 2 (Input & Output Ends) | Only 2 (Load & Retrieve) | Direct Drive-In Bays | 0 Internal (Out-of-bay Crane/Lift) |
| Maintenance & Energy Costs | Zero Electrical Energy Draw | Periodic Lithium Battery Swaps | Low (Focus on Column Guards) | Programmed Electrical & PLC Maintenance |
| Ideal Industry Scenarios | Dairy, Produce, Cold Chain, Pharma | High Volume SKU Perishables | Beverage, Grain, Packaging | Smart Megawarehouses, Lights-Out 3PL |
How automation integration, environmental resilience, and digital traceability are shifting the procurement landscape for warehouse storage equipment.
Global supply chain managers are shifting from static, baseline loading considerations toward dynamic impact resistance. Racks configured for deep-lane FIFO encounter heavy repeated vibrations from continuous roller momentum or shuttle travel. Modern procurement specifications demand cold-formed high-tensile Q235B/Q355B steel, reinforced frame footplates, high-ductility anchor assemblies, and compliance with modern seismic design codes (such as RMI ANSI MH16.1 and EN 15512).
Gravity-fed pallet flow lanes frequently encounter varied wooden, plastic, and corrugated pallet styles. Future procurement trends place heavy emphasis on universal roller profiles: polyurethane sleeves, reinforced polymer sprockets, and zinc-electroplated steel rollers paired with centrifugal safety brakes. This protects against uncontrolled pallet acceleration and ensures smooth operational flow even in sub-zero cold-storage (-30°C) facilities.
Modern supply chains require complete real-time inventory visibility. The industry is moving away from passive steel racks toward instrumented storage networks. Advanced FIFO installations now frequently deploy optical beam sensors, radio telemetry, and load-plate transducers that interface directly with WMS/ERP platforms, providing real-time bay utilization, weight tracking, and automated stock rotation verification without manual checks.
Corporate ESG mandates and strict environmental standards are reshaping surface finishing requirements. Leading international buyers now actively require suppliers to provide eco-friendly, zero-VOC electrostatic powder coatings, heavy metal-free multi-stage pickling and phosphating cycles, and verified corrosion warranties for tropical humidity and maritime operating conditions.
Decades of manufacturing precision, automated production infrastructure, and dedicated global project support.
Equipped with computerized cold-roll profiling lines, automated CNC punch systems, and continuous-feed robotic welding lines. We inspect and control every step from raw hot-rolled strip steel coils to packaged components.
Full CE certification (No. 2435-CPR-8605159) alongside ISO 9001:2015 audited quality management systems (No. 18624Q00169R0M). Every project includes structural calculations and factory load test documentation.
Experienced design engineers create tailored CAD plans, structural load calculations, and comprehensive 3D visual models to maximize warehouse space and match pallet handling equipment specifications.
Serving over 120 countries with sea-worthy container bundling, labelled component indices, and complete logistics coordination. We also provide remote video engineering support and on-site assembly supervision.
Clear, practical answers to common questions regarding structural engineering, commissioning, and system performance.
Our gravity-fed flow racks utilize built-in centrifugal speed controller rollers positioned at measured intervals down each lane. As pallets accelerate down the 3.0% to 3.5% slope, the internal centrifugal brakes engage mechanically without electrical power, keeping speed to a controlled crawl of 0.1 to 0.3 m/s. Additionally, heavy-duty separator stops hold back queue pressure at the discharge face, so fork truck operators can retrieve the lead pallet safely without dealing with back pressure from rear loads.
Yes. Our upright frames feature precision CNC-punched teardrop or diamond hole patterns at 50mm or 75mm pitch intervals. This bolt-free connection structure allows quick adjustments to beam levels, easy extension of rack lengths, and straightforward retrofits—such as transitioning static drive-through layouts to automated radio shuttle channels or adding live carton flow tracks for manual picking levels.
High-density racking systems generate concentrated point loads through the upright baseplates. Concrete slabs typically require minimum compressive strengths of 25 to 30 MPa (C25/C30 grade) and a thickness of 150mm to 250mm, reinforced with steel mesh. For gravity flow or narrow-aisle shuttle operations, floor flatness should meet DIN 18202 Table 3 Group 3 or ASTM E1155 F-min 75 standards to keep upright columns plum and roller planes aligned.
Every steel component undergoes an automated chemical pretreatment sequence: degreasing, acid pickling to eliminate scale, and iron phosphating to ensure paint bonding. We then apply an electrostatic dry-powder thermosetting epoxy-polyester coating baked at 180°C to 200°C. For damp coastal warehouses, ambient chemical facilities, or sub-zero cold rooms (-30°C), we also offer hot-dip galvanizing per EN ISO 1461, providing decades of rust-resistant protection.
To produce an accurate CAD layout, structural load analysis, and quotation, please provide: (1) Warehouse architectural drawings showing clear heights, building columns, dock doors, and fire exits; (2) Pallet specifications including width, depth, height, and maximum load weight; (3) Pallet bottom design (e.g., three-runner, perimeter base, plastic/wood); (4) Material handling equipment models, lifting heights, and turning radii; and (5) Operational throughput targets (pallets per hour in and out).
All HEDA racking systems include our factory warranty covering structural integrity and manufacturing defects under rated usage conditions. We supply complete CE declarations of performance, Mill Test Certificates (MTC) verifying raw coil steel mechanical properties, and verified structural design calculations adhering to EN 15512, FEM 10.2.02, and RMI standards.