High-Efficiency Carton Flow & Heavy-Duty Warehouse Storage Racks
Explore our industrial-grade live dynamic flow lanes, high-bay selective pallet frameworks, and multi-tier picking setups manufactured with certified high-tensile steel.
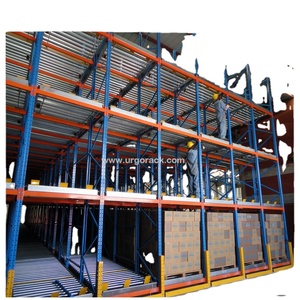
High Efficiency Order Picking Racking System, Gravity Flow Roller Racking System
Equipped with aluminum alloy guide tracks, precision polyurethane or steel rollers, and adjustable shelf dividers to enable smooth First-In, First-Out (FIFO) split-case fulfillment.
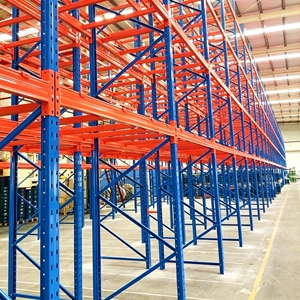
Hot Selling Adjustable Heavy Duty Steel Industrial Racks 6 8 10 Layer High Bay Warehouse Storage Selective Pallet Racking System
Built with certified Q235B cold-rolled profiles supporting 1,000–4,500 kg per beam level. Complete integration with multi-tier carton flow pick levels underneath heavy pallets.
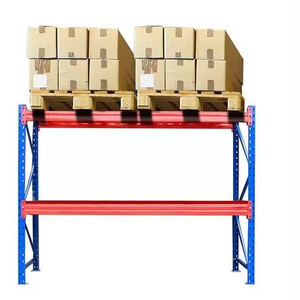
Heavy Duty Racking System - Selective Pallet Racking System
Standard modular selective racking featuring bolted frame uprights, adjustable 50mm/75mm beam hole pitches, electrostatic epoxy finish, and custom anti-impact column guards.
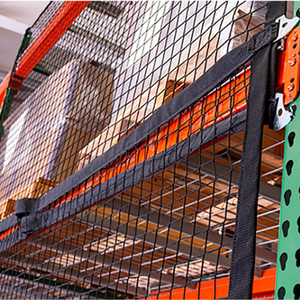
Customizable Polyester Woven Pallet Cargo Rack Net with Rope Edge OEM/ODM Cargo Wrap Netting Cut-to-Size Service
Heavy-duty containment mesh designed for anti-drop protection along rear discharge faces of high-speed carton gravity and live roller picking aisles.
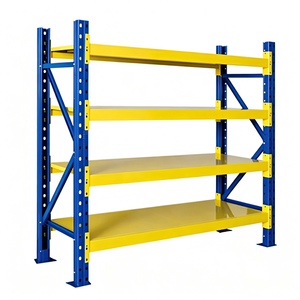
Industrial Warehouse Shelving Adjustable Metal Storage Rack Commercial Logistics Factory Garage Workshop Goods Organization
Versatile boltless and adjustable steel shelving modules convertible into gravity flow picking beds with modular snap-in roller tracks and guide rails.
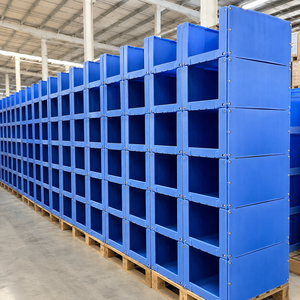
PP Corrugated Plastic Stackable Warehouse Picking Bins Front Opening Warehouse Shelf Storage for Industrial Parts
Impact-resistant polypropylene front-opening totes engineered for continuous slide and zero-friction navigation through carton flow bed tracks.
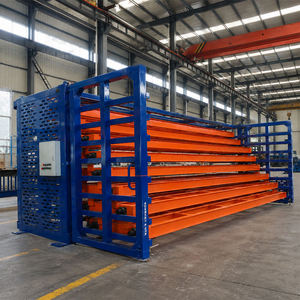
Heavy Duty Durable 6-Layer Carbon Steel Foldable Push-Back Pallet Rack Industrial Warehouse Storage Space Saving Anti-Rust
Nested dynamic cart design utilizing inclined rails to deliver deep-lane high-density accumulation, maximizing cubic volume utilization up to 75%.
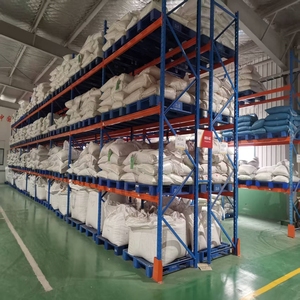
Industrial Storage Racks Custom 5 Layer US Teardrop Pallet Rack Conventional Pallet Racking For Warehouse Cold Room Storage
Standard American teardrop pattern compatibility, cold-room treated anti-rust electrostatic powder coatings, allowing bolt-free snap-in carton flow shelf integration.
Carton Flow Shelving: Mechanical Principles & Warehouse Ergonomics
In modern e-commerce fulfillment hubs, high-turnover pharmaceutical logistics, and fast-moving consumer goods (FMCG) distribution centers, split-case picking accounts for upwards of 55% to 65% of total operating warehouse labor costs. Conventional static shelving requires order pickers to travel excessive linear distances, leading to operator fatigue, aisle congestion, and picking bottlenecks. As an elite China wholesale carton flow shelving manufacturer, our engineered gravity flow solutions separate stock replenishment from order picking aisles, fundamentally eliminating picker-replenisher conflicts and increasing picking throughput by over 150%.
Carton flow racking—frequently referred to as gravity flow shelving, live storage, or carton roller racks—utilizes inclined roller tracks or skate-wheel conveyor beds mounted inside standard pallet rack or independent shelving structures. Operating on natural gravitational energy, totes, bins, and corrugated cartons introduced at the rear loading (charging) face automatically roll forward along an engineered slope (typically calibrated between 2.5° to 4.5°) toward the front discharge (picking) face. When the foremost SKU is picked by an operator, the trailing stock smoothly glides forward into the primary retrieval position under controlled gravity momentum.
Strict FIFO Stock Rotation
By enforcing an unalterable First-In, First-Out sequence, carton flow racking eliminates inventory expiration risks in perishables, cosmetics, pharmaceutical distribution, and batch-sensitive cold stores.
Ergonomic Pick Density
Consolidating up to 40 distinct SKUs per linear meter along the aisle face cuts picker transit walks by up to 75%, maintaining clear separation between forklift loading lanes and pedestrian picking lanes.
Seamless WMS & Pick-to-Light
Our track frameworks feature integrated wiring channels and fascia mounting channels specifically engineered for electronic Pick-to-Light (PTL), Pick-by-Voice, and automated picking sensor brackets.
Structural Engineering Matrix: Wheel Track vs. Roller Bed Configurations
Choosing the correct track geometry depends upon carton bottom characteristics, unit weight distribution, and environmental ambient conditions. Below is our factory engineering comparison designed to guide wholesale buyers and industrial consultants:
| Engineering Attribute | Plastic Skate-Wheel Flow Track | Full-Width Steel Roller Bed | Heavy-Duty Polyurethane Wheel |
|---|---|---|---|
| Track Profile Material | High-strength extruded Aluminum / Galvanized Steel | Precision Cold-Rolled SPCC C-Profile | Structural Cold-Drawn Steel Channel |
| Wheel / Roller Pitch | 25mm / 35mm / 50mm Adjustable | 30mm to 100mm Continuous Pitch | 35mm / 50mm Heavy-Load Spacing |
| Uniform Load Capacity | 50 – 120 kg per linear meter | 150 – 350 kg per linear meter | 200 – 500 kg per linear meter |
| Recommended Carton Substrate | Rigid flat-bottom plastic totes & KLT bins | Corrugated cardboard, mixed packaging, banded totes | Heavy industrial wooden crates, steel totes |
| Operating Temperature Range | -10°C to +45°C (Dry warehousing) | -30°C to +60°C (Cold storage blast freezers) | -25°C to +50°C (Industrial chemical / automotive) |
| Braking & Flow Control | Integrated entry & exit impact guides | Centrifugal speed brake rollers available | Heavy end-stop safety retainers |
Why Tier-1 Importers Partner with Our Guangzhou Manufacturing Base
Since 2001, Guangzhou Heda Shelves Co., Ltd. has stood as a pioneer among Chinese racking manufacturers. Operating from our modern 30,000 m² production complex with over 300 experienced engineers and technicians, we guarantee direct-from-factory pricing with uncompromising international quality standards.
Automated CNC Roll-Forming Lines
We operate 16 continuous precision cold-roll-forming extrusion lines capable of punching and profiling upright columns, step beams, and flow bed frames with dimensional tolerances maintained under ±0.5mm.
Certified International Compliance
All factory structural components carry certified third-party testing credentials, including European CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 Management System Certification No. 18624Q00169R0M, and RoHS hazardous materials conformity.
10-Stage Surface Treatment Line
Steel parts undergo immersion degreasing, ultrasonic rust removal, zinc phosphating, and electrostatic epoxy-polyester powder baking at 200°C, offering superior corrosion resistance against tropical humidity and cold-chain condensation.
10 Controlled Production Stages: From Prime Steel Coil to Containerized Export
Every carton flow frame and heavy-duty shelf that leaves our workshops adheres to strict structural tracing:
Raw Materials
Certified prime Q235B & Q355B coils tested for yield & tensile strength.
Precision Slitting
High-speed laser cutting & computerized coil uncoiling to exact dimensions.
Continuous Punching
Automated CNC multi-station hydraulic punching for teardrop and diamond pitch holes.
Cold Roll Forming
Progressive roller pass lines shaping structural uprights and step beams.
Track Bending
Forming customized galvanized C-channels and roller track framework.
Robotic Welding
CO2 gas-shielded automated robotic welding ensuring defect-free joint weld beads.
Pickling & Phosphating
Multi-tank chemical pre-treatment removing surface oxides for powder adhesion.
Electrostatic Coating
Automated powder coating booths applying uniform 60–90 micron polymer coats.
Baking & Curing
Continuous tunnel ovens baking parts at high temperatures for impact elasticity.
Export Packing
Steel-strapped bundles with corrugated wrap and labeled loading charts.
Future Procurement & Technological Trends in Carton Flow Racking (2025–2030)
Supply chain leaders must plan storage investments around emerging automation frameworks, shifting SKU velocities, and carbon-reduction initiatives. Here is where the carton flow engineering industry is heading over the next five years:
Hybrid AMR & AGV Integration
Modern carton flow designs no longer rely solely on human pickers. Next-generation installations incorporate automated replenishment by Autonomous Mobile Robots (AMRs) loading rear lanes and cobots picking from the discharge front.
Modular "Drop-In" Universal Flow Beds
Procurement managers increasingly demand flexibility over dedicated lane hardware. Pre-assembled drop-in roller beds that sit directly on existing pallet rack beams allow warehouses to dynamically shift between bulk pallet storage and split-case carton picking within minutes.
Sustainable Low-Friction Polymers
The transition toward carbon-neutral supply chains has accelerated the adoption of recyclable polypropylene and self-lubricating POM roller wheels. These rollers drop the incline angle required for gravity propulsion from 4.5° to 2.2°, maximizing vertical cube utilization by saving clearance space.
Strategic Procurement Recommendations for Global B2B Buyers
When procuring wholesale carton flow shelving from Chinese manufacturers, corporate procurement teams should avoid evaluating suppliers solely on basic steel tonnage prices. A poorly engineered flow lane will exhibit carton hanging, tracking drift, carton crush, or premature axle fatigue, resulting in costly operational downtime.
Ensure that your factory partner conducts Dynamic Deflection Calculations and guarantees that track guide rails maintain an L/250 deflection threshold under full carton live loads. Request physical flow testing with your exact carton dimensions and weight specifications before approving mass container loading. Working directly with an established engineering manufacturer like Guangzhou Heda Shelves guarantees transparent mill test certificates (MTC), verifiable CE/ISO credentials, and precise CAD/BIM architectural layout files for seamless local permit approval.
Frequently Asked Questions: Sourcing Carton Flow Shelving from China
Authoritative technical answers to common questions raised by procurement officers, project managers, and logistics consultants when sourcing wholesale gravity shelving.
Ready to Optimize Your Order Picking Infrastructure?
Whether you are outfitting a regional e-commerce fulfillment center, modernizing a 3PL distribution hub, or seeking reliable OEM/ODM contract manufacturing for industrial racking components, our engineering team in Guangzhou is ready to assist. Contact us today for free 3D warehouse layouts, structural calculations, and competitive factory-direct wholesale pricing.