China Top Storage Racks For Industrial Use Manufacturer & Factory
Precision-engineered selective pallet systems, automated radio shuttles, high-capacity mezzanines, and seismic-rated racking structures direct from our audited manufacturing facility.
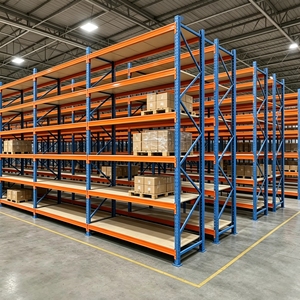
High-Efficiency Industrial Storage Systems for Warehouses & Logistics
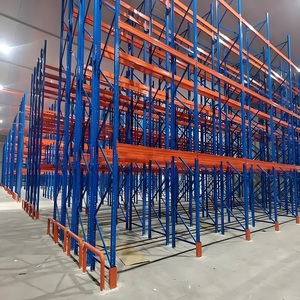
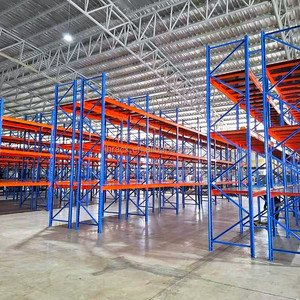
Our heavy-duty steel systems deliver optimal volumetric utilization, high-density throughput, and structural durability verified under international safety protocols (CE, ISO 9001:2015, and RoHS).
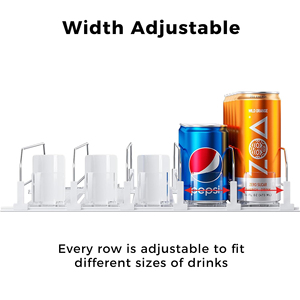
Self-facing gravity roller lane system for retail distribution, commercial coolers, and fast-moving picking zones, cutting handling time significantly.
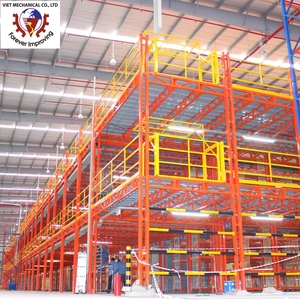
Doubles or triples warehouse square footage using heavy upright columns to support intermediate picking platforms, conveyors, or administrative suites.
Global supply-chain resilience requires moving away from commodity steel purchases toward verified load design, seismic calculation, and modular automation-ready warehouse frameworks.
Finite Element (FEA) Structural Optimization
Modern industrial racks must comply with stringent international standards such as EN 15512, RMI MH16.1, and local seismic criteria. Cold-formed steel profiles with optimized multi-bend Omega geometries yield up to 22% higher load ratings with less steel deadweight, cutting freight and installation costs.
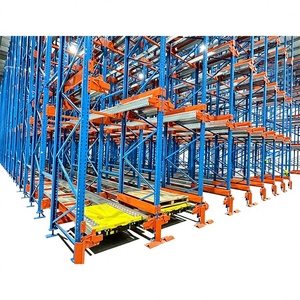
Semi-Automated Pallet Shuttle Integration
Conventional Drive-in racks are quickly being upgraded to Radio Shuttle and 4-Way AS/RS setups. This shift addresses high labor costs and warehouse real-estate pricing by replacing forklift lanes with continuous storage lanes, boosting capacity by 40% to 70% and lowering rack impact damage.
Advanced Anti-Corrosive Coatings
Cold-chain warehousing, coastal facilities, and tropical climates require heavy-duty surface protection. Multi-stage phosphating plus epoxy powder coating (60–90µm) combined with hot-dip galvanizing for sub-zero rooms ensures over 15 years of rust-free service without peeling.
Direct Manufacturer Credibility
Guangzhou HEDA Shelves: 25 Years of Factory-Direct Engineering Authority
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is a premier Chinese manufacturer specializing in heavy-duty industrial pallet racking, automated shuttle systems, and multi-tier mezzanines. Our single-source production model eliminates trading margins and ensures direct accountability.
From initial structural layout simulations to automated continuous rolling lines and ISO-certified quality inspections, we supply industrial facilities across Latin America, Southeast Asia, Europe, and North America.
Certified Compliance: CE Mark (No. 2435-CPR-8605159), ISO 9001:2015, and RoHS verified structural integrity.
Free Engineering Services: Comprehensive 2D CAD floor plans, 3D parametric models, and seismic load analyses delivered within 24 hours.
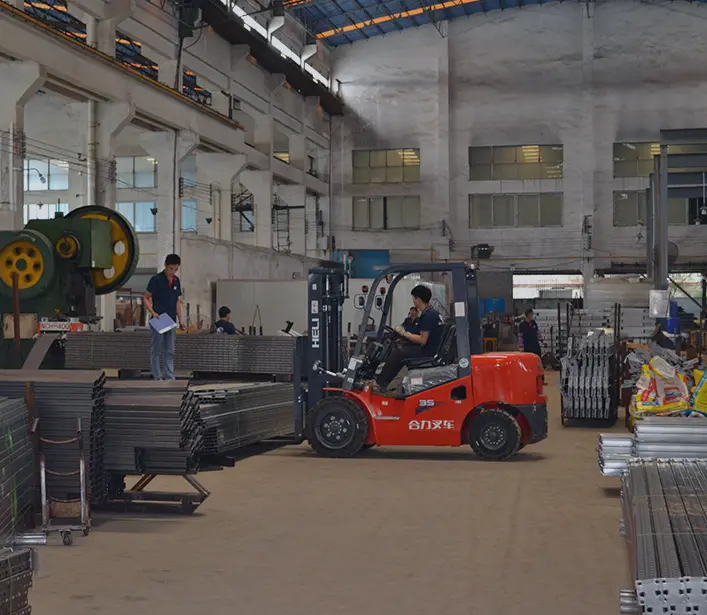
High Production Capacity: 30,000 m² workshop, 300+ trained fabricators, handling orders up to 30,000 metric tons per month.
Components undergo an automated 4-stage cleaning, acid pickling, and phosphating cycle prior to electrostatic curing at 180°C, ensuring impact resistance and long-term corrosion prevention.
Procurement Intelligence
Frequently Asked Questions by Industrial Rack Buyers
Clear, practical answers covering shipping logistics, custom engineering, building permits, and structural verification.
What parameters are required to calculate an accurate structural rack quote?
To configure a code-compliant racking layout, our engineering team requires: (1) Warehouse clear height to the lowest overhead obstruction, (2) Floor slab concrete thickness, reinforcement details, and compressive strength (e.g., 20–25 MPa), (3) Pallet dimensions (W × D × H) including product overhang, (4) Maximum gross weight per pallet load, and (5) Forklift model, minimum turning radius, and maximum mast extension.
Can HEDA Shelves design storage systems for active seismic zones?
Yes. Many overseas warehouses sit in active seismic zones (such as the Pacific Rim and Latin America). Our engineers perform dynamic finite element calculations based on your local building code and soil classification. We configure enlarged base plates, high-tensile anchor bolts, and reinforced diagonal bracing patterns to handle both static and seismic dynamic loads.
What surface finish is best for cold rooms or humid environments?
For ambient warehouses, our multi-stage electrostatic powder coating provides strong, long-lasting surface protection. For cold-chain operations, freezing facilities (-25°C to -30°C), coastal warehouses, or chemical storage, we provide hot-dip galvanized (HDG) uprights, beams, and wire decks to prevent condensation-induced rust.
How are installation, alignment, and site assembly handled for export orders?
Every shipment includes detailed CAD layout maps, numbered assembly sequences, component packing lists, and step-by-step video instructions. For major distribution centers, cold stores, and multi-tier mezzanines, we can send bilingual installation supervisors to direct your local team, or provide direct remote video support.
What international testing certifications accompany shipments?
Our manufacturing systems operate under ISO 9001:2015 quality assurance. Our structural products carry CE certification (No. 2435-CPR-8605159) and RoHS compliance. We also provide mill test certificates (MTC) documenting steel yield points and chemical composition upon request.
Ready to maximize your facility's vertical capacity and structural safety?