LIFO System
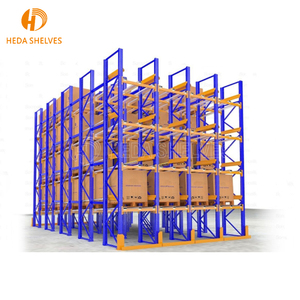
Manufactured to rigid CE specifications using high-tensile Q235B structural steel, automated punching lines, and multi-stage electrostatic powder coating.
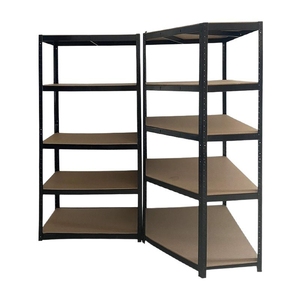
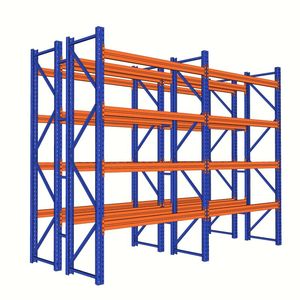
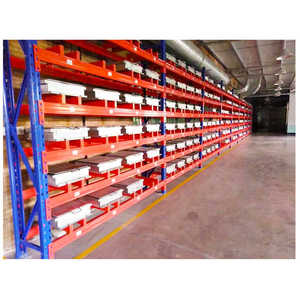
A technical assessment of load dynamics, floor utilization, access selectivity, and handling velocity to maximize warehouse ROI.
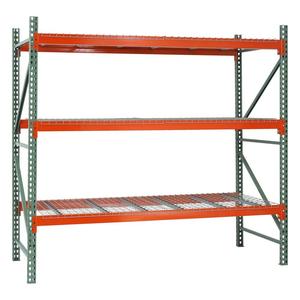
The global benchmark for multi-SKU inventory environments requiring pure 100% SKU selectivity. Compatible with counterbalanced, reach trucks, and articulated equipment.
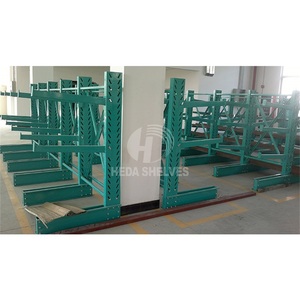
Engineered to eliminate picking aisles, forklifts enter structural lanes to place pallets on continuous console rails. Maximizes cubic volumetric capacity.
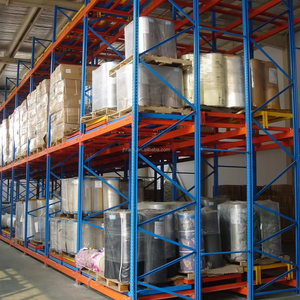
Semi-automated deep lane technology where high-precision smart lithium shuttle carts transport unit loads within internal channels via remote command.
Mechanical benchmarks conforming to EN 15512 European Standards and certified for international export.
| Racking Type | Typical Payload / Level | Clear Height Reach | Material Standard | Stock Rotation Rule | Aisle Width Requisite |
|---|---|---|---|---|---|
| Selective Pallet Rack | 1,000 kg – 4,500 kg | Up to 14.5 Meters | Certified Q235B / Q355B | Strict FIFO (100% Selectivity) | 2.8m – 3.6m (Truck Dependent) |
| Heavy Duty Drive-In | 800 kg – 1,800 kg / pallet | Up to 12.0 Meters | Cold-Rolled Omega Profile | LIFO / Optional FIFO | Lane-based (Guide Rails Applied) |
| Cantilever Rack System | 500 kg – 3,000 kg / arm | Up to 9.0 Meters | H-Beam / Structural C-Roll | Unrestricted Longitudinal Access | Direct Lateral Loading |
| Push Back Racking | 1,000 kg – 1,500 kg / cart | Up to 7.5 Meters | Heavy-Gauge Ball Bearings | LIFO (Gravity Cart Flow) | Standard Counterbalance Reach |
| Multi-Tier Mezzanine | 300 kg – 1,200 kg / m² | Multi-Level (2–4 tiers) | Engineered Box Girder & Mesh | Zone Picking / Manual Split | Integrated Stairway & Catwalks |
Market intelligence regarding seismic design requirements, eco-friendly coatings, and high-density material integration.
Global procurement teams no longer accept static generic calculations. Modern facilities located along active fault zones demand project-tailored structural calculations incorporating floor slab tensile resistance, dynamic baseplate anchorage, and EN 16681 compliant moment-resistant frame assemblies.
With real estate costs rising globally, the capital expenditure on high-density push-back, gravity flow, and 24V lithium radio-shuttle systems pays back within 18 months by eliminating useless aisle dead space and slashing industrial refrigeration power loads by up to 35%.
Industrial warehousing across tropical coastlines requires advanced multi-stage chemical surface conversion. Ten-stage spray washing, automated zinc phosphating, and thermo-cured hybrid epoxy-polyester coatings ensure maximum salt-spray resistance and longevity in high-humidity zones.
Combining world-class production infrastructure, accredited quality management, and comprehensive project support.
Spanning over 30,000 m² of smart facilities, our workshop runs 10 precision production lines: cold-roll forming, automated CNC punch stamping, CO2 gas-shielded welding, phosphating baths, and electrostatic powder curing.
Operating under CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 quality management (Registration No. 18624Q00169R0M, valid to June 2027), and RoHS compliance for international bidding assurance.
Our senior CAD engineering desk provides free warehouse layout schemes, 3D structural visual simulations, clearance clearances, and mechanical deflection checks within 24 hours of receiving site blueprints.
We source prime hot-rolled structural steel coils exclusively from tier-1 mills. Mill test reports verify tensile strength, elongation percentages, and chemical batch consistency across every column profile.
Beams, frames, and upright brackets are bundled with multi-layer bubble wrap, edge protection angles, and moisture-proof plastic film, tagged with clear container loading manifests for fast field unloading.
Every order is dispatched with bilingual step-by-step assembly diagrams. Dedicated structural supervisors are available for worldwide on-site installation oversight and contractor training.
In-depth technical answers addressing import compliance, seismic safety, layout parameters, and container logistics.
Our engineering team requires: (1) Architectural drawings showing warehouse length, width, column pitch, and unobstructed height beneath roof trusses; (2) Pallet specifications including overall dimensions (W×D×H), maximum gross load weight, and bottom runner orientations; (3) Material handling equipment profile—forklift turning radius, mast height, and reach limits; and (4) Turnaround velocity / SKU metrics to balance density versus access speed.
Every structural system is tailored to local site conditions. By cross-referencing regional seismic response parameters (such as peak ground acceleration) and slab structural data, we perform Finite Element Analysis (FEA) to determine vertical column thicknesses, heavy-duty floor baseplates, back-to-back bracing, and anchor wedge diameters that meet stringent EN 16681 standards.
For standard temperature-controlled warehouses, our 10-stage phosphating bath coupled with thermoset hybrid electrostatic powder coating (60–80 microns) provides superb protection. In high-humidity coastal ports, walk-in cold rooms, or chemical storage, we engineer continuous hot-dip galvanized components (BS EN ISO 1461 compliant) that provide active zinc barrier protection against rust.
As a seasoned tier-1 exporter, HEDA Shelves delivers under FOB, CIF, CFR, or DDP terms worldwide. We provide full customs clearance packages including CE Declarations of Conformity, Mill Test Certificates (EN 10204 3.1), Form E / Certificate of Origin, container loading weight distributions, and itemized component pack lists to streamline port clearance.
Consult with our senior logistics engineers today. Receive an itemized turnkey proposal, complete structural calculation report, and 2D/3D CAD layout within 24 hours.
Inquire Now