Engineered High-Density Racking & Dynamic Shuttle Solutions
Discover factory-direct heavy-duty storage configurations compliant with EN 15512 and FEM 10.2.02 standards. Purpose-built for maximum volumetric efficiency.
25+
Years Industry Engineering
30,000t
Monthly Steel Throughput
10,000+
Global Installations
100%
CE & ISO Audited Quality
Technical Whitepaper: Engineering Criteria for Industrial Drive Through Racking
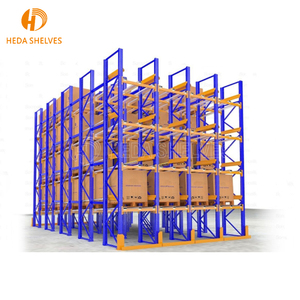
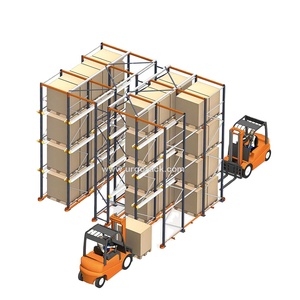
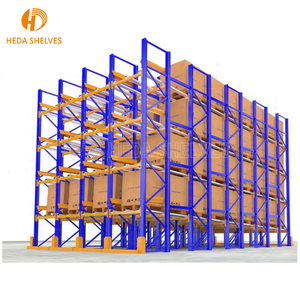
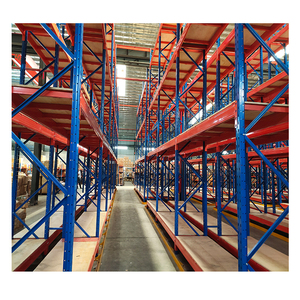
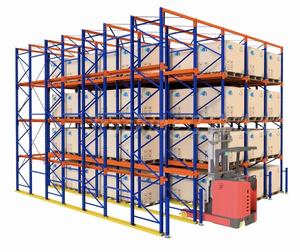
Drive Through racking represents the pinnacle of floor-space optimization for facilities operating on a strict First-In, First-Out (FIFO) batch turnover system. Unlike standard Drive-In racking which relies on a single entrance/exit aisle (LIFO), Drive Through structures are engineered with separate entry and dispatch aisles. This dual-access layout completely isolates loading workflows from retrieval operations, eliminating logistics bottlenecks in high-velocity cold chains, chemical plants, and fast-moving consumer goods (FMCG) distribution centers.
Because structural forklifts must physically navigate inside the storage cube, the engineering integrity of every component is subject to strict stress calculations. Without cross-aisle horizontal beam bracing across the drive bays, torsional deflection and horizontal displacement become critical factors. As a certified manufacturer, our engineering team adheres strictly to EN 15512:2020 (European Standard for Steel Static Storage Systems) and RMI (Rack Manufacturers Institute) seismic safety provisions, incorporating heavy-gauge Q235B and high-yield Q355B cold-formed structural steel profiles.
| Structural Dimension | Standard Warehouse Requirement | HEDA High-Spec Engineering Profile | Operational Value Metric |
|---|---|---|---|
| Upright Section Gauge | 1.8 mm – 2.0 mm Carbon Steel | 2.0 mm – 2.5 mm High-Tensile Q355B | +35% Dynamic Torsional Resistance |
| Pallet Support Arm | Standard Cantilever Arm | Reinforced Tapered Double-Support Arm | Zero-Sag Pallet Guidance Alignment |
| Corrosion Barrier | Single Coat Solvent Spray | Pickling, Phosphating + Electrostatic Powder | ISO 9227 Salt Spray Testing > 500h |
| Seismic Anchoring | Standard Wedge Expansion Anchors | Heavy-Duty Baseplates with Chemical M16 Anchors | Certified Peak Ground Acceleration (PGA) resistance |
Industry Procurement Trends: Strategic Analysis for 2025–2030
Global supply chains are navigating elevated land values, cold-chain electricity expenses, and skilled-operator shortages. As enterprise logistics directors reassess capital investments, Drive Through and high-density racking procurement is undergoing measurable shifts:
Cold-Chain Densification
Refrigerated and frozen cubic real estate carries 4x the operating expense of ambient space. Modern procurement mandates high-density Drive Through channels equipped with hot-dip galvanizing to prevent structural embrittlement down to -30°C.
Life-Cycle Risk Abatement
Procurement teams are moving away from non-certified budget steel. Demands now focus on documented CE CPR certifications, third-party yield tensile validation, and full batch traceability to mitigate liability and insurance audit failures.
Hybrid Shuttle Adaptability
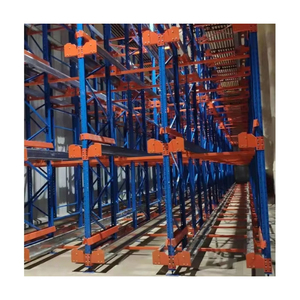
Buyers are selecting Drive Through rail profiles that can natively accept Radio Shuttle carriers. This future-proofs the installation, allowing warehouses to transition from manual forklift drive-in to semi-automated shuttle dispatch without replacing uprights.
Technological Advancements in Drive Through Rack Architecture
The engineering evolution of drive-through infrastructure is resolving historical trade-offs between density and structural fatigue. Key innovations implemented across our production facilities include:
Finite Element Seismic Analysis
Using 3D FEA stress simulations, our engineers calculate second-order (P-Delta) frame effects under extreme seismic lateral loads, customizing horizontal top-tie trusses to deliver complete stability across geologically active regions.
Smart Impact-Deflecting Armor
Forklift impact inside continuous lanes is minimized via floor-anchored continuous guide rails and cold-rolled column protectors featuring polymer shock absorption, ensuring structural verticality remains uncompromised over decades.
WMS-Integrated Sensor Nodes
Modern drive through infrastructure incorporates retrofitted optical distance and lane-depth sensors. Real-time data streams into warehouse management systems, preventing driver misplacement and verifying pallet clearance dynamically.
Enterprise Manufacturing Competence & Supply Chain Authority
As Guangzhou Heda Shelves Co., Ltd., we combine 25 years of engineering manufacturing with global logistics execution. Operating from our 30,000 m² state-of-the-art facility, our monthly capacity exceeds 30,000 tons of structural steel storage equipment, delivered to more than 120 countries worldwide.
Certified International Compliance
Our operations carry European CE Certification (Certificate No. 2435-CPR-8605159), ISO 9001:2015 Quality Management System verification (Certificate No. 18624Q00169R0M), and complete RoHS material non-toxicity compliance, ensuring smooth local municipal approval.
End-to-End Vertical Manufacturing
From automated multi-station cold roll-forming lines and CNC punching to fully enclosed electrostatic powder coating systems with 10-stage pre-treatment, every beam, rail, and upright is produced under strict internal quality gates.
Bespoke Engineering & Free 3D Layouts
Our technical team of 300+ engineers delivers free CAD floor layouts, dynamic 3D visualizations, and precise load capacity calculations within 24 hours, taking into account building dimensions, forklift turning radii, and SKU dynamics.
Container-Optimized Export Packing
Overseas delivery mandates precise protection. Every component is bundled, barcoded, and cataloged on itemized packing manifests. We offer dedicated CIF and FOB port handling across major Pacific, Caribbean, and European maritime routes.
Procurement Technical FAQ
Essential structural and commercial considerations addressed by our Senior Application Engineers:
What is the structural difference between Drive-In and Drive-Through Racking?
Drive-In utilizes a single access aisle for loading and unloading, operating exclusively on a LIFO (Last-In, First-Out) principle. Drive-Through racking features open entry on both ends, creating separate loading and retrieval aisles. This supports strict FIFO management, making it ideal for batch-sensitive goods, fresh produce, and rapid turnarounds.
How does your engineering team address seismic risks?
Drive-Through systems lack traditional beam cross-bracing within the lanes. To maintain rigidity, we design rigid overhead horizontal tie-beams, top portal bracing, and reinforced column baseplates. Our structural calculations integrate local spectral response accelerations (Ss and S1) according to site-specific building regulations.
What forklift clearances are required inside Drive Through lanes?
Standard counterbalanced forklifts, reach trucks, or articulated trucks can operate in drive-through systems, provided overall mast and chassis widths clear the pallet support rails. Standard lane design generally specifies 75 mm to 100 mm of total clearance on each side, along with floor-mounted steel guide rails to safeguard column uprights.
Which surface coating should be selected for high humidity or cold storage?
For ambient, dry warehousing, our 10-stage pickling, phosphating, and electrostatic powder coating provides robust mechanical resistance. For sub-zero cold rooms, coastal tropical ports, or agricultural chemicals, hot-dip galvanizing (ISO 1461) is strongly recommended to protect against oxidation and steel embrittlement.
What essential project specifications are required for a 3D layout?
To produce an engineered proposal within 24 hours, our design office requires: warehouse clear height and slab dimensions, pallet dimensions (W x D x H including overhang), maximum gross pallet weight, forklift model and reach height, and temperature parameters.
How are international installation and on-site assembly handled?
Every export shipment is accompanied by detailed structural component drawings, anchor torque specs, and step-by-step video assembly guides. For large-scale industrial projects, senior installation project engineers can be deployed on-site to oversee assembly and load-testing certifications.